HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced powder handling systems. This article explores the desulfurization sodium bicarbonate powder conveying system equipment, detailing its functionality and the underlying design principles that ensure efficient and reliable operation in industrial applications.
Introduction to Desulfurization Sodium Bicarbonate Powder Conveying System Equipment
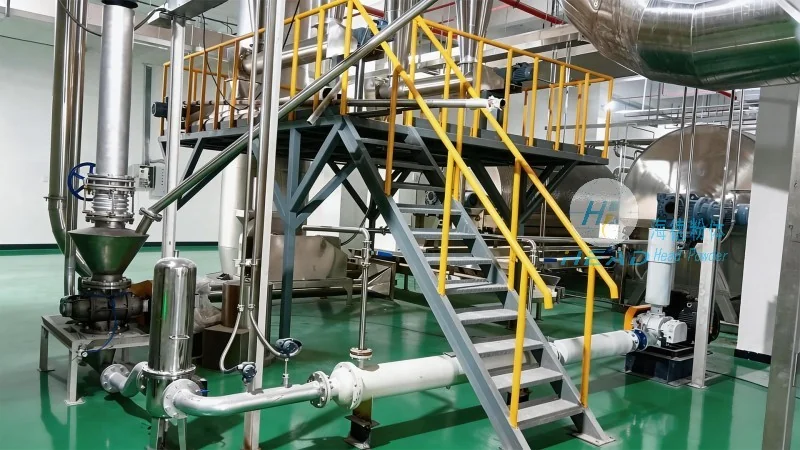
The desulfurization sodium bicarbonate powder conveying system equipment is a specialized device used in industrial processes, particularly in power plants and chemical facilities, to transport sodium bicarbonate powder. This material is commonly employed as a desulfurizer in flue gas treatment systems, where it helps reduce sulfur dioxide emissions. The conveying system ensures that the sodium bicarbonate powder is moved from storage to the point of use with minimal loss, contamination, or environmental impact.
Key Components and Functionality of the Conveying System
The system typically consists of several key components that work in tandem to achieve efficient powder transport. These include a hopper for material storage, a feeder to control the flow rate, a conveying pipeline (often equipped with air or gas to facilitate movement), and a discharge mechanism at the destination. The design emphasizes the use of positive pressure or negative pressure systems to maintain a sealed environment, preventing dust leakage and ensuring compliance with environmental regulations.
Design Principles for Efficient and Reliable Operation
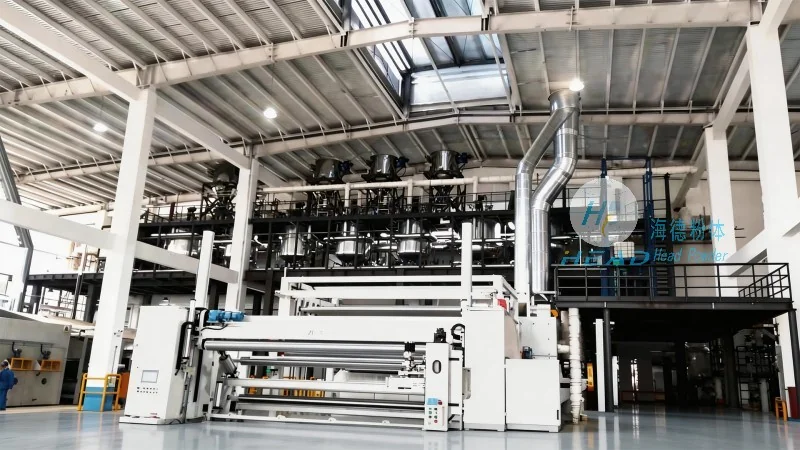
The design of the desulfurization sodium bicarbonate powder conveying system equipment is guided by several critical principles aimed at optimizing performance and safety. One of the primary principles is the maintenance of a consistent flow rate, which is achieved through precise control of the feeder mechanism. This ensures that the powder is conveyed at a steady speed, reducing the risk of clogging or uneven distribution.
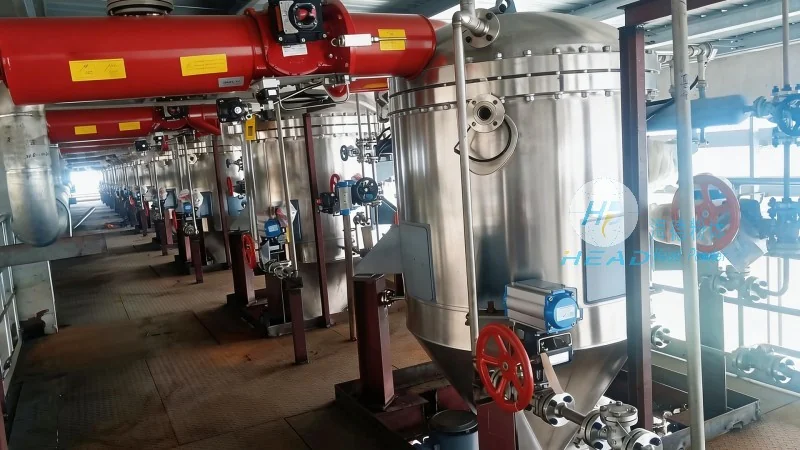
Another key principle is the use of airtight and dust-proof components. The system is engineered to minimize particle leakage and prevent contamination of the surrounding environment. This is crucial in industrial settings where air quality and safety are paramount. The materials used in the construction of the equipment, such as stainless steel and corrosion-resistant alloys, further enhance durability and longevity.
Advantages of the System in Industrial Applications
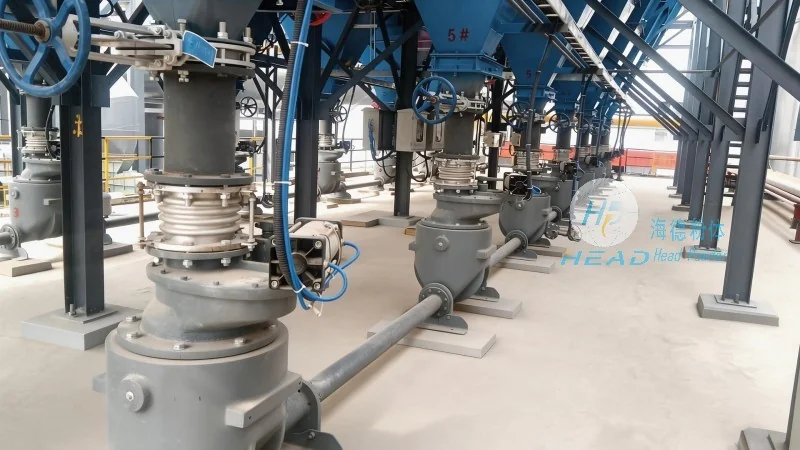
The desulfurization sodium bicarbonate powder conveying system equipment offers several advantages that make it an ideal choice for industrial desulfurization processes. Firstly, it provides a highly efficient and continuous method of transporting the powder, reducing downtime and increasing overall productivity. Secondly, the sealed system design minimizes environmental impact by preventing dust emissions, which is essential for meeting regulatory standards. Additionally, the system's flexibility allows it to be integrated with existing infrastructure, making it a cost-effective solution for upgrading or expanding desulfurization facilities.
Conclusion
In conclusion, the desulfurization sodium bicarbonate powder conveying system equipment is a sophisticated piece of industrial machinery designed to handle sodium bicarbonate powder with precision and efficiency. The design principles, including consistent flow control, airtight construction, and material durability, ensure that the system operates reliably and safely in demanding industrial environments. As a product of Shandong HeadPowder Engineering Co., Ltd., this equipment represents a commitment to quality and innovation in powder handling technology, supporting the effective management of desulfurization processes in various industries.




