For industrial applications that require efficient and reliable powder handling, the gray bin powder conveying line is a critical component. This system is designed to transport bulk materials such as powders, granules, and other particulate substances from storage bins to processing equipment. Understanding its structure and design principles is essential for optimizing material flow and ensuring operational efficiency in various industries, including pharmaceuticals, chemicals, food processing, and manufacturing.
Introduction to Gray Bin Powder Conveying Lines
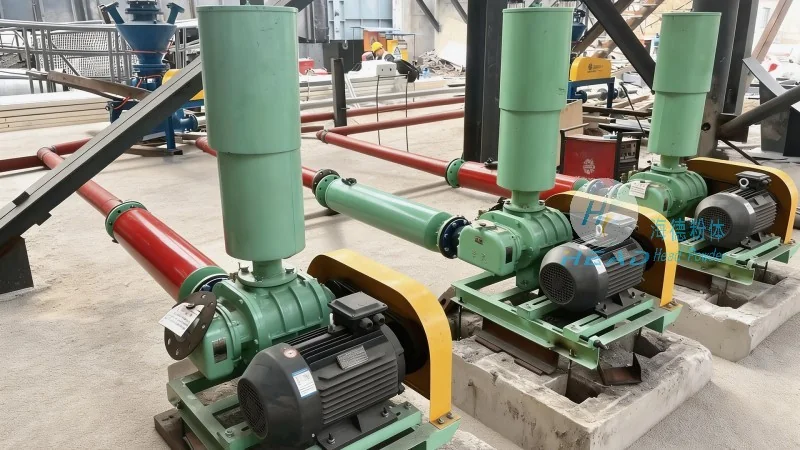
The gray bin powder conveying line, as the name suggests, utilizes a gray storage bin as the primary hopper for holding bulk powders. This bin is typically made of durable materials like stainless steel or high-density polyethylene to ensure resistance to corrosion and wear from the conveyed materials. The system integrates several key components that work in tandem to facilitate smooth material transfer. These components include the hopper, conveyor mechanism, control system, and discharge equipment. Each part plays a vital role in maintaining the integrity of the material and ensuring consistent performance under different operational conditions.
Design Principles of the Gray Bin Powder Conveying Line
The design of a gray bin powder conveying line is guided by several fundamental principles aimed at maximizing efficiency, safety, and reliability. One of the core principles is the use of a sealed hopper to prevent material contamination and dust emissions. The gray color of the bin often serves functional purposes, such as heat reflection to reduce temperature buildup, which is crucial for temperature-sensitive materials. The system also incorporates a low-pressure air or mechanical conveyor to move the material from the bin to the processing line. This approach minimizes product degradation and ensures that the material remains in its original state throughout the conveying process.
Key Components and Their Functions
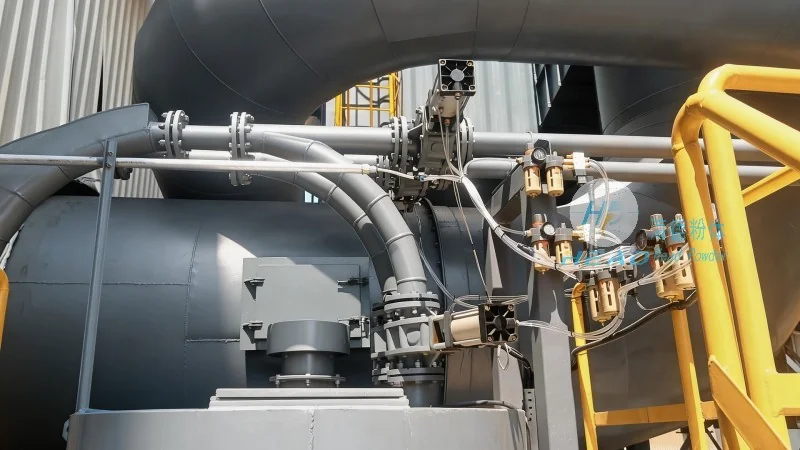
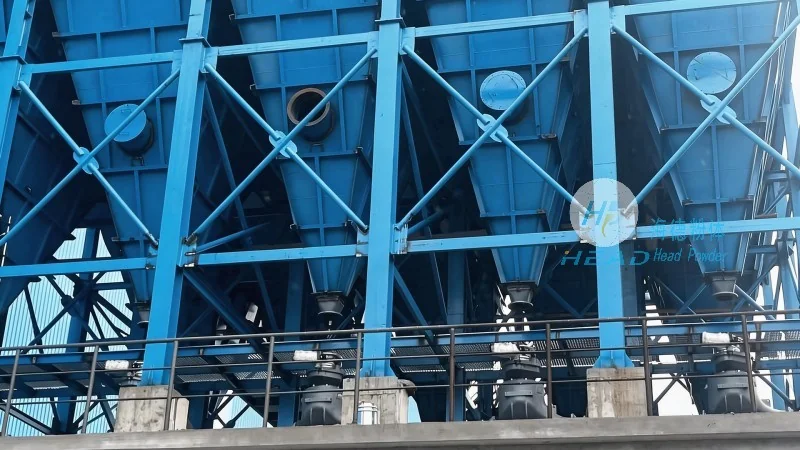
At the heart of the gray bin powder conveying line are several critical components that enable its operation. The storage bin, or hopper, is designed with a conical or rectangular shape to facilitate material flow. The bin's outlet is equipped with a valve or gate mechanism that controls the release of material into the conveyor. The conveyor itself can be a pneumatic system using compressed air to create a vacuum or pressure to move the powder, or a mechanical system like a screw or belt conveyor. The control system manages the operation of these components, ensuring that the material is conveyed at the correct rate and that the system operates safely. Additionally, the discharge equipment, such as a rotary valve or star feeder, regulates the flow of material from the conveyor to the downstream processing equipment, preventing blockages and ensuring a steady supply.
Advantages of Using a Gray Bin Powder Conveying Line
Implementing a gray bin powder conveying line offers numerous advantages for industrial operations. First, it enhances material handling efficiency by reducing the time and labor required for manual transfer. The automated system ensures consistent and reliable material flow, minimizing downtime and improving overall productivity. Second, the sealed design helps maintain product quality by preventing contamination from external sources and reducing dust exposure. This is particularly important for industries dealing with sensitive materials like pharmaceuticals or food products. Third, the system's modular design allows for easy integration with existing processing lines, making it a flexible solution for various applications. Furthermore, the use of durable materials in the construction of the bin and conveyor components ensures long-term reliability and low maintenance costs.
Applications in Different Industries
The gray bin powder conveying line is widely used across multiple industries due to its versatility and adaptability. In the pharmaceutical industry, it is used to transport raw materials and finished products with high precision, ensuring compliance with regulatory standards. In the chemical industry, it handles various powders and granules, including those that are corrosive or reactive, with minimal risk of contamination. The food processing industry benefits from the system's ability to maintain hygiene standards, as the sealed design prevents cross-contamination and dust from entering the processing line. In manufacturing, the line is used to transport raw materials to production lines, improving workflow and reducing material handling errors. Each application leverages the system's design principles to meet specific operational requirements, ensuring optimal performance in diverse environments.
Conclusion and Company Information
The gray bin powder conveying line is a sophisticated and efficient solution for bulk powder handling, designed to meet the demands of modern industrial operations. Its robust construction, sealed design, and integrated control system make it a reliable choice for various applications. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing these systems to ensure optimal performance and customer satisfaction. With a focus on quality and innovation, the company offers tailored solutions that address the unique needs of each client, contributing to improved operational efficiency and product quality across industries. Based in China, Shandong HeadPowder Engineering Co., Ltd. leverages its expertise to deliver high-performance powder conveying lines that enhance productivity and safety in industrial settings.




