When it comes to the safe and efficient handling of powders in industrial settings, especially those that are prone to oxidation or pose explosion risks, the nitrogen-protected powder conveying system emerges as a critical solution. This technology is designed to maintain an inert atmosphere within the conveying line, effectively isolating the powder from atmospheric oxygen and moisture. The primary goal is to prevent spontaneous combustion, dust explosions, and degradation of the material during transport. Understanding the components and design principles behind such a system is essential for industries ranging from pharmaceuticals and food processing to chemical manufacturing and mining.
About HeadPowder: Your Trusted Partner in Powder Handling Solutions
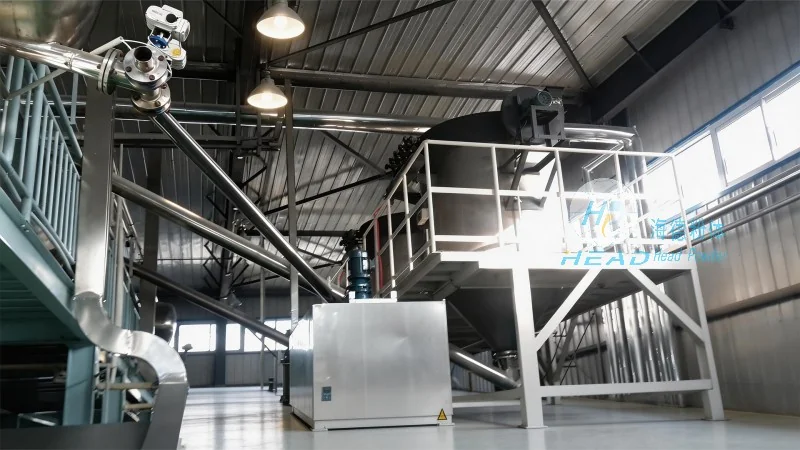
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of advanced powder handling equipment based in Shandong, China. With a strong commitment to innovation and safety, the company specializes in developing customized solutions tailored to the unique needs of various industries. HeadPowder's expertise lies in designing systems that ensure the integrity of sensitive powders while adhering to stringent safety standards. The company's facilities and technical team are dedicated to delivering high-quality, reliable equipment that meets international safety and performance requirements.
Introducing the Nitrogen-Protected Powder Conveying System
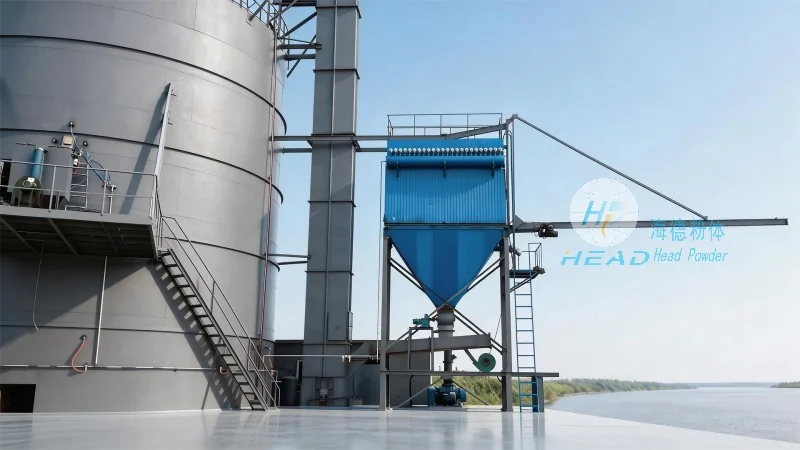
The nitrogen-protected powder conveying system is a sophisticated piece of industrial equipment engineered to transport dry powders through a sealed pipeline while maintaining a protective nitrogen environment. This system is particularly valuable for handling materials that are sensitive to air exposure, such as pharmaceuticals, food additives, and certain chemicals. The core components of the system include a nitrogen gas supply unit, a series of sealed conveying pipes, and specialized valves and controls. The nitrogen gas is continuously introduced into the pipeline, displacing the air and creating an inert atmosphere that prevents oxidation or other chemical reactions that could compromise the quality of the powder. The system is equipped with sensors and monitoring devices to ensure the nitrogen level remains consistent throughout the conveying process.
The Design Principles of a Nitrogen-Protected Powder Conveying System
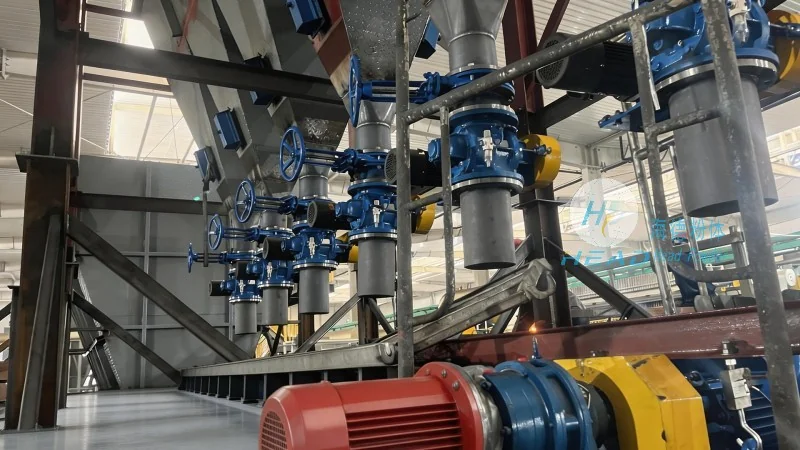
The design of a nitrogen-protected powder conveying system is based on several key principles aimed at ensuring safety, efficiency, and material integrity. First, the system must provide a complete seal to prevent any air ingress. This is achieved through the use of double-flanged or welded joints in the conveying pipes, as well as specialized sealing mechanisms at the inlet and outlet points. Second, the nitrogen gas supply must be reliable and capable of maintaining a consistent pressure and flow rate. This typically involves a nitrogen generator or a high-pressure storage system, coupled with a regulator and flow control valve. Third, the conveying mechanism itself—such as a screw conveyor, pneumatic blower, or air slide—must be compatible with the inert atmosphere. These components are often designed with materials that are resistant to corrosion and wear, ensuring long-term performance. Fourth, the system incorporates safety features, including pressure relief valves, gas detectors, and emergency shut-off mechanisms, to mitigate any potential risks. The integration of these elements results in a robust and reliable system that can handle a wide range of powders while maintaining the required inert environment.
Key Advantages of Using a Nitrogen-Protected Powder Conveying System
Implementing a nitrogen-protected powder conveying system offers numerous benefits for industrial operations. One of the most significant advantages is the prevention of dust explosions and spontaneous combustion, which are major hazards in powder handling environments. By maintaining an oxygen-free atmosphere, the system eliminates the risk of ignition from static electricity or other sources. Additionally, the inert environment protects the powder from oxidation, which can alter its properties, affect its shelf life, or reduce its effectiveness in downstream processes. This is particularly important for pharmaceutical and food products where quality and purity are paramount. The system also enhances the efficiency of the conveying process by reducing the risk of material caking or blockages, which can occur when powders are exposed to air. Furthermore, the sealed design minimizes dust emissions, improving workplace safety and compliance with environmental regulations. Overall, the nitrogen-protected system provides a cost-effective and sustainable solution that improves both safety and product quality in powder handling applications.
Conclusion: The Importance of Proper Design and Implementation
In conclusion, the nitrogen-protected powder conveying system is a vital technology for industries dealing with sensitive powders. Its design, which emphasizes complete sealing, reliable nitrogen supply, and robust conveying mechanisms, ensures that powders are transported safely and efficiently. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in developing and supplying these systems, providing tailored solutions that meet the specific requirements of their clients. By investing in such advanced equipment, industries can mitigate risks, improve product quality, and enhance operational efficiency. The continued development and application of nitrogen-protected systems will remain essential as industries strive to maintain high standards of safety and performance in powder handling operations.




