Desulfurization processes in industrial applications often rely on sodium bicarbonate as a key reagent. The efficient and reliable transport of this powder is critical for maintaining process efficiency and minimizing downtime. The desulfurization sodium bicarbonate powder conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., addresses these challenges through a specialized design that ensures optimal performance in various industrial settings.
Key Components and Design Philosophy
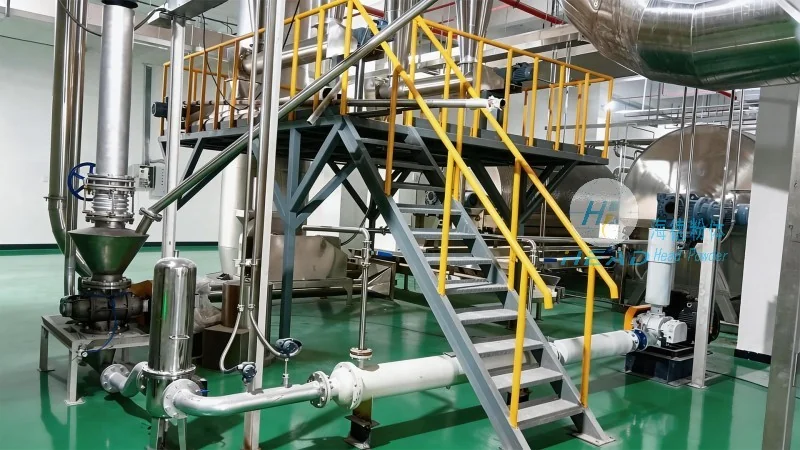
The system is engineered with a focus on durability, efficiency, and safety, reflecting the company's commitment to delivering high-quality industrial solutions. At the core of the design are components such as feed hoppers, screw conveyors, and pneumatic transport units, each carefully selected to handle the unique properties of sodium bicarbonate powder. The feed hopper is designed to accommodate bulk storage and controlled discharge, ensuring a steady flow of material into the conveying system. The screw conveyor, with its helical blades, provides gentle yet effective movement, preventing material degradation and maintaining product integrity. Pneumatic transport units, when integrated, offer flexibility for long-distance or complex routing, enhancing the system's adaptability.
Design Principles for Optimal Performance
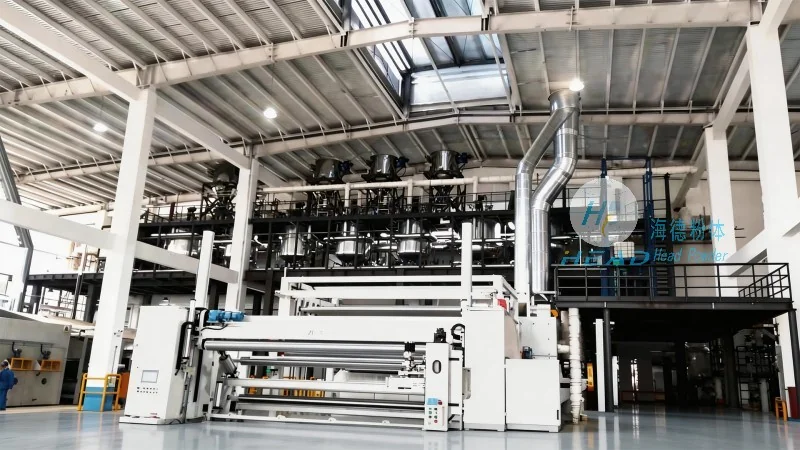
The design principles of the desulfurization sodium bicarbonate powder conveying system are centered on several key factors: material handling efficiency, system reliability, and operational safety. The system is built to minimize material degradation, which is crucial for maintaining the chemical properties of sodium bicarbonate. This is achieved through low-friction surfaces, gentle material movement, and proper sealing to prevent contamination or loss. Reliability is ensured through robust construction, using materials resistant to corrosion and wear, typical of industrial environments. The system also incorporates safety features, such as emergency shut-off valves and pressure relief mechanisms, to protect operators and equipment from potential hazards.
Application in Desulfurization Processes
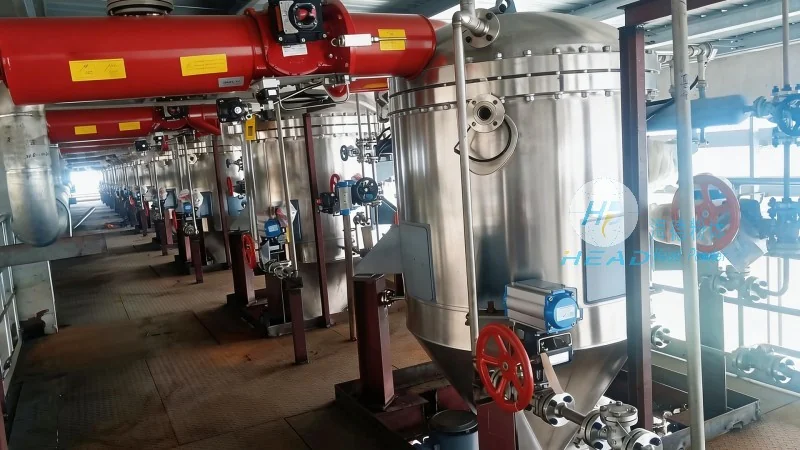
In desulfurization applications, the conveying system plays a vital role in delivering sodium bicarbonate to reactors or absorbers. The system's ability to handle fine powders without clogging or bridging is particularly important, as these issues can lead to process interruptions. The design ensures consistent flow rates, which directly impacts the efficiency of the desulfurization reaction. By maintaining a steady supply of sodium bicarbonate, the system supports consistent performance and reduces the need for frequent maintenance or adjustments.
Advantages of the HeadPowder Solution
Shandong HeadPowder Engineering Co., Ltd. has integrated years of experience in powder handling technology into the design of this conveying system. The result is a solution that offers several advantages over traditional methods. These include reduced energy consumption due to optimized material movement, lower maintenance costs from durable components, and enhanced safety through integrated safety features. The system's modular design also allows for easy integration into existing industrial setups, minimizing installation time and disruption to operations.
Conclusion
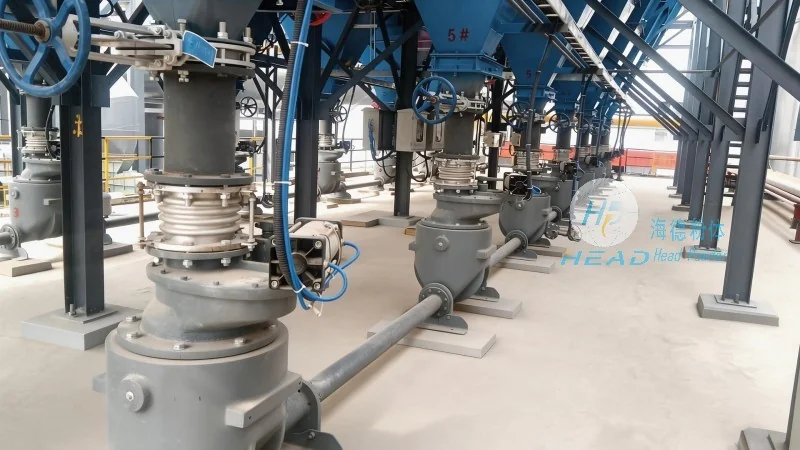
The desulfurization sodium bicarbonate powder conveying system equipment from Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated solution for the efficient transport of sodium bicarbonate in industrial desulfurization processes. By adhering to principles of durability, efficiency, and safety, the system ensures reliable performance while maintaining the quality of the material being handled. For industries seeking to optimize their desulfurization operations, this equipment offers a practical and effective approach to powder handling, supporting consistent and efficient process outcomes.




