HeadPowder Engineering, a leading provider of industrial material handling solutions, specializes in the design and implementation of efficient pneumatic conveying systems tailored for the transportation of manganese sulfate. This system is engineered to meet the specific demands of handling manganese sulfate, ensuring reliable and safe material transport in industrial applications. The design incorporates advanced technology and robust construction to handle the unique properties of manganese sulfate, such as its chemical stability and handling requirements.
Key Features and Technical Specifications
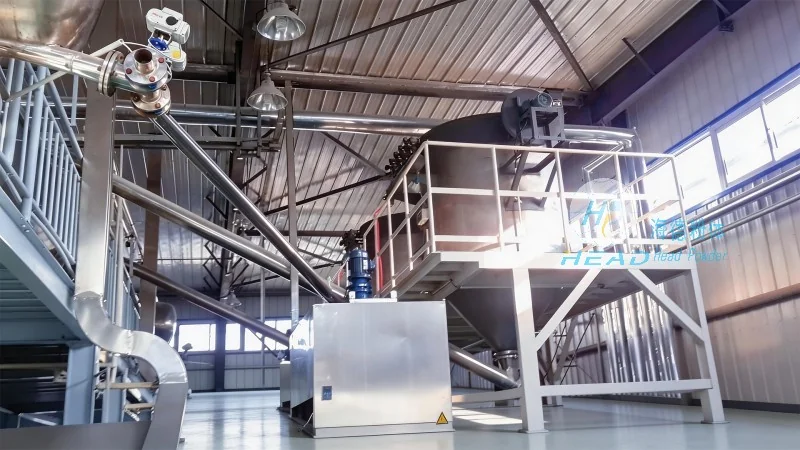
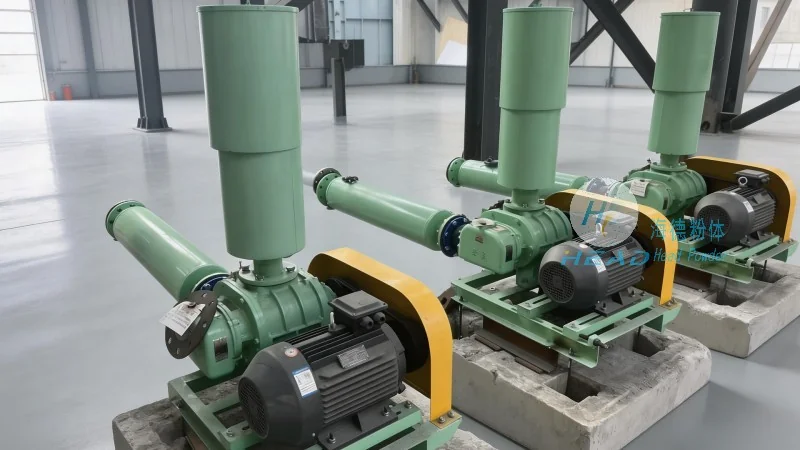
The pneumatic conveying system for manganese sulfate is equipped with several key features that enhance its performance and reliability. These include high-efficiency air fans capable of maintaining consistent air pressure and flow rates, which are critical for the smooth transport of the material. The system utilizes a combination of positive and negative pressure conveying methods, allowing for flexible operation based on the application requirements. Additionally, the system incorporates high-quality material handling components, including stainless steel or corrosion-resistant materials, to ensure durability and resistance to the chemical properties of manganese sulfate. The design also includes advanced control systems that allow for real-time monitoring and adjustment of the conveying process, optimizing efficiency and minimizing downtime.
Application and Operational Benefits
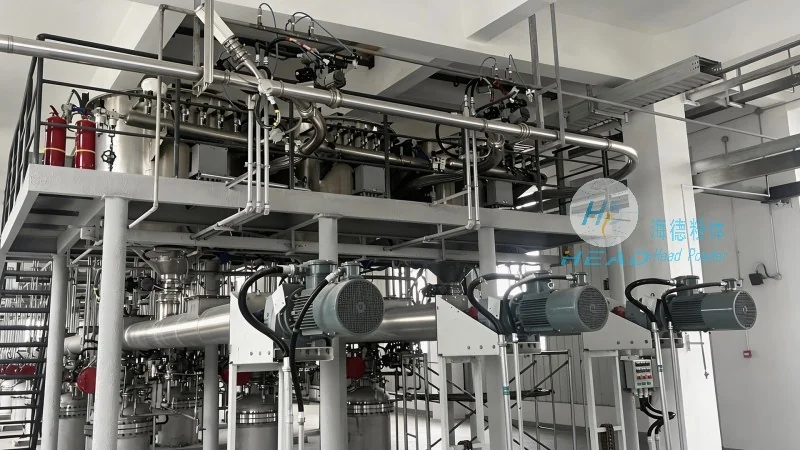
The pneumatic conveying system for manganese sulfate is widely used in various industrial sectors, including chemical manufacturing, mining, and food processing. Its primary benefits include the ability to transport manganese sulfate in a dust-free environment, reducing the risk of contamination and improving workplace safety. The system also offers significant advantages in terms of space efficiency, as it eliminates the need for traditional conveyor belts or hoppers, allowing for more compact and flexible layouts. Furthermore, the system's ability to handle varying material flow rates and compositions makes it suitable for a wide range of applications, from small-scale laboratory use to large-scale industrial production. The operational benefits also extend to cost savings, as the system reduces labor costs associated with manual handling and minimizes material loss due to spillage or degradation.
Customization and Integration Services
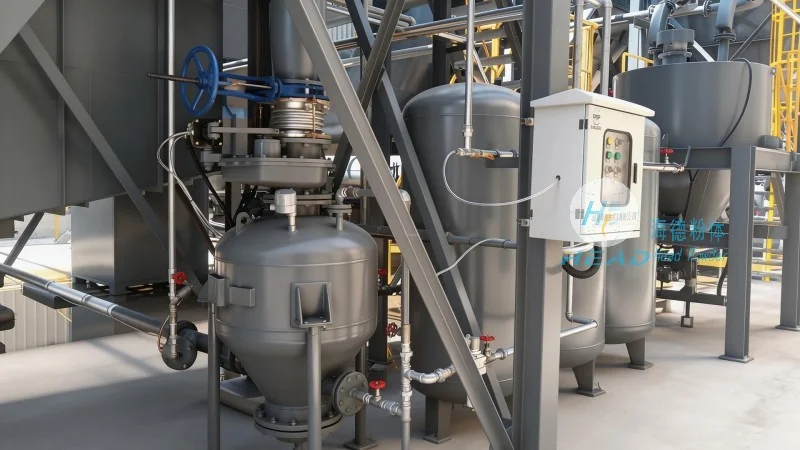
HeadPowder Engineering understands that each industrial application has unique requirements. Therefore, the pneumatic conveying system for manganese sulfate is designed to be highly customizable. The company offers tailored solutions that can be integrated with existing production lines or new facilities. This includes the ability to adjust the system's capacity, pressure, and flow rates to match specific production needs. Additionally, the system can be integrated with other industrial equipment, such as storage tanks, mixers, and processing units, to create a comprehensive material handling solution. The customization process involves detailed consultation with clients to understand their operational needs, followed by the design and implementation of a system that meets all technical and safety standards.
Quality Assurance and Compliance
HeadPowder Engineering adheres to strict quality assurance protocols to ensure the reliability and safety of its pneumatic conveying systems. The manganese sulfate system is manufactured using high-quality materials and components that meet international standards for industrial equipment. The company follows a rigorous quality control process, including material testing, component inspection, and system testing, to ensure that each system meets the required performance and safety specifications. Additionally, the system is designed to comply with relevant industry regulations and standards, such as those related to chemical handling and workplace safety. This ensures that the system is not only efficient but also safe for operation in industrial environments.
Customer Support and After-Sales Service
HeadPowder Engineering provides comprehensive customer support and after-sales services to ensure the long-term performance and reliability of the pneumatic conveying system for manganese sulfate. The company offers technical support, including installation guidance and operational training, to help clients maximize the system's efficiency. Additionally, the company provides regular maintenance and inspection services to identify and address potential issues before they become major problems. The after-sales service also includes spare parts availability and prompt technical assistance, ensuring that clients can maintain the system's optimal performance. This support is crucial for ensuring the system's longevity and minimizing downtime, which is essential for maintaining production efficiency.




