This article provides an introduction to the pneumatic conveying equipment designed for transporting coke and limestone powder. Such equipment is essential in industrial processes where efficient and reliable material handling is crucial. The system utilizes air as the medium to move bulk materials, offering advantages like reduced contamination, lower maintenance, and the ability to transport materials over long distances without the need for complex mechanical components.
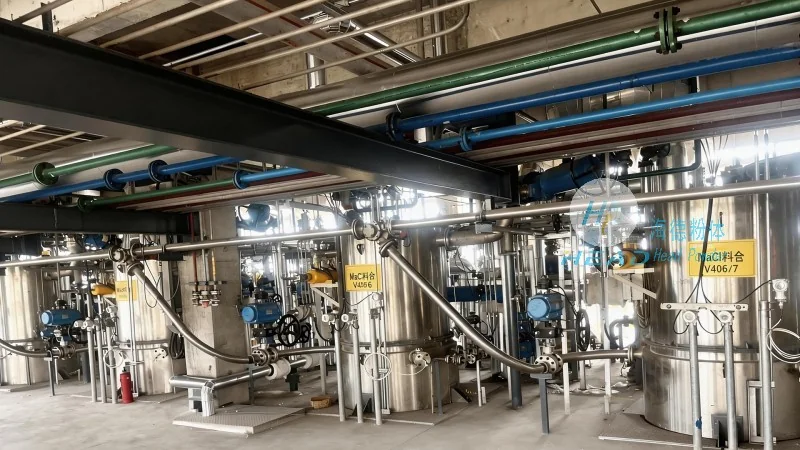
Key Components and Structure of the Pneumatic Conveying System
The core structure of the coke and limestone powder pneumatic conveying equipment typically includes several key components. The system starts with a hopper or storage bin where the raw material is stored. From there, the material is fed into a conveying line through a feeder, which controls the flow rate. The conveying line itself is often a pipeline that transports the material using compressed air. At the receiving end, a separator or cyclone is used to separate the material from the air stream, allowing the material to be deposited in the target location. Additionally, a filter system is integrated to clean the air before it is released back into the environment, ensuring compliance with environmental regulations.
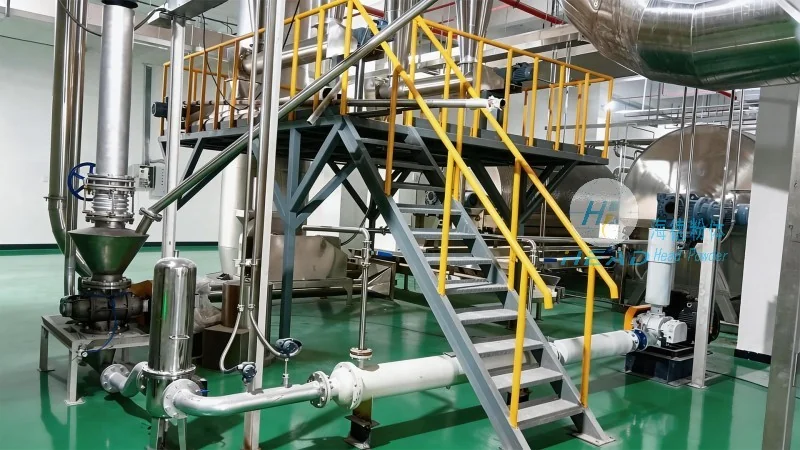
Working Principle of the Pneumatic Conveying Process
The operation of the coke and limestone powder pneumatic conveying system is based on the principle of air flow. When compressed air is introduced into the conveying line, it creates a pressure differential that draws the powder material from the hopper into the line. The air and powder mixture travels through the pipeline at high velocity, maintaining the material in suspension. As the mixture reaches the receiving end, the separator uses centrifugal force to separate the powder from the air. The separated powder is collected in a collection bin, while the clean air is filtered and discharged. This process ensures that the material is transported efficiently and without degradation, making it suitable for various industrial applications.
Advantages of Using Pneumatic Conveying for Coke and Limestone Powder
Employing pneumatic conveying for coke and limestone powder offers several benefits that enhance operational efficiency and product quality. First, the system minimizes material contamination, which is critical for maintaining the purity of the powder, especially in applications like cement production or steel manufacturing. Second, it reduces the need for manual handling, improving workplace safety and reducing labor costs. Third, the equipment is compact and can be installed in various layouts, making it adaptable to different plant designs. Finally, the system is highly reliable, with fewer moving parts compared to mechanical conveyors, leading to lower maintenance requirements and longer service life.
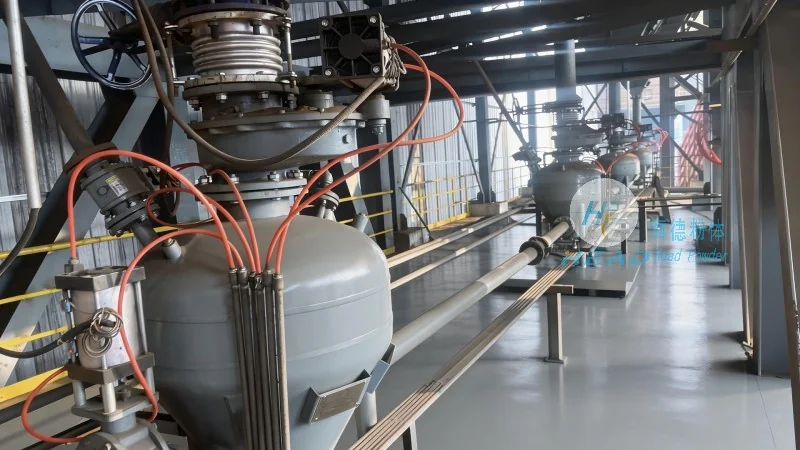
Company Information: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the manufacturer of this advanced pneumatic conveying equipment, is a leading company in the field of material handling solutions. Based in Shandong, China, the company specializes in designing and manufacturing customized equipment for various industrial applications. With years of experience and a commitment to quality, HeadPowder provides reliable and efficient solutions for transporting bulk materials like coke and limestone powder. The company's products are engineered to meet the specific needs of clients, ensuring optimal performance and durability in demanding industrial environments.




