This article provides an overview of the metering bin pump pneumatic conveying system, a critical equipment used in the handling and transportation of bulk materials such as powders and granules. The system is designed to efficiently move materials over long distances with minimal energy consumption and low maintenance requirements. By understanding its structure and operational principles, users can better appreciate its advantages in industrial applications, particularly in sectors like food processing, pharmaceuticals, and chemical manufacturing.
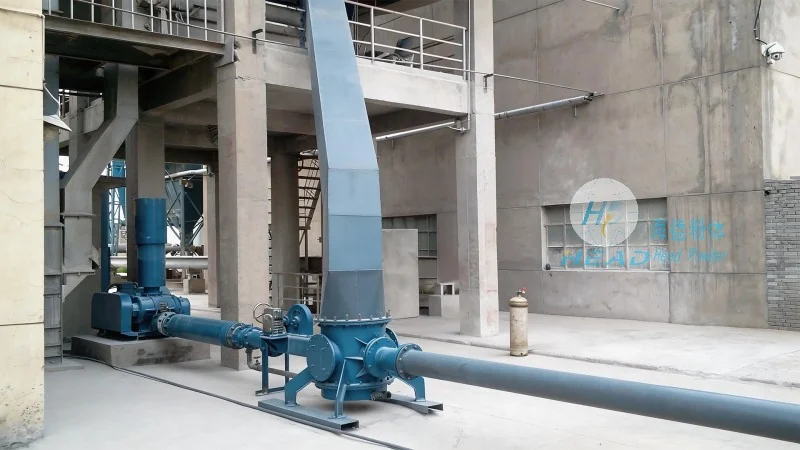
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in engineering solutions for powder handling and material processing. The company has built a strong reputation for delivering high-quality pneumatic conveying systems and related equipment. With a focus on innovation and customer satisfaction, HeadPowder has become a trusted partner for industries requiring reliable and efficient material transport solutions. The company's headquarters and main production facilities are located in Shandong, providing a solid foundation for its operations and product development.
System Structure and Core Components
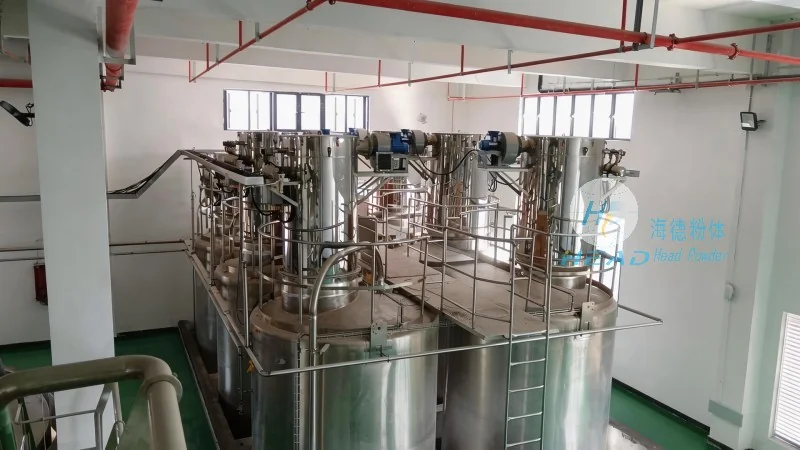
The metering bin pump pneumatic conveying system comprises several key components that work in coordination to achieve effective material transport. The primary components include the metering bin, the pump unit, the conveying pipeline, and the control system. The metering bin serves as the storage and feeding unit, where bulk materials are stored and metered before being fed into the pump. The pump unit, typically a positive displacement pump, generates the necessary pressure to move the material through the pipeline. The conveying pipeline connects the pump to the discharge point, ensuring a continuous flow of material. The control system manages the operation of the pump, bin, and other components, allowing for precise control over the conveying process. Additionally, the system may include accessories such as air filters, silencers, and material separators to enhance performance and safety.
Operational Principle and Working Mechanism
The operational principle of the metering bin pump pneumatic conveying system is based on the positive displacement of the pump, which creates a pressure differential to move the material. The process starts with the material being fed from the metering bin into the pump chamber. As the pump rotates, it traps the material and forces it through the discharge port into the conveying pipeline. Simultaneously, air is introduced into the pump to assist in the transport, reducing friction and ensuring smooth flow. The system operates in a closed loop, with the air and material being separated at the discharge point, and the air being recirculated or vented as needed. This design minimizes material loss and ensures high efficiency in the conveying process. The positive displacement mechanism ensures a consistent flow rate, which is crucial for processes that require precise material delivery, such as dosing or batching.
Advantages of the Metering Bin Pump System
Compared to traditional pneumatic conveying systems, the metering bin pump offers several advantages that make it suitable for a wide range of industrial applications. One of the key benefits is its ability to handle a wide variety of materials, including fine powders and abrasive granules, without causing blockages or excessive wear. The positive displacement design ensures a consistent flow rate, which is essential for processes that require accurate material delivery, such as in pharmaceutical manufacturing or food processing. Additionally, the system is energy-efficient, as it uses less air pressure compared to other pneumatic systems, resulting in lower operational costs. The compact design of the metering bin pump also allows for easy integration into existing production lines, reducing installation time and costs. Furthermore, the system is relatively low maintenance, with fewer moving parts compared to other conveying methods, which contributes to its long service life and reliability.
Applications and Industry Use Cases
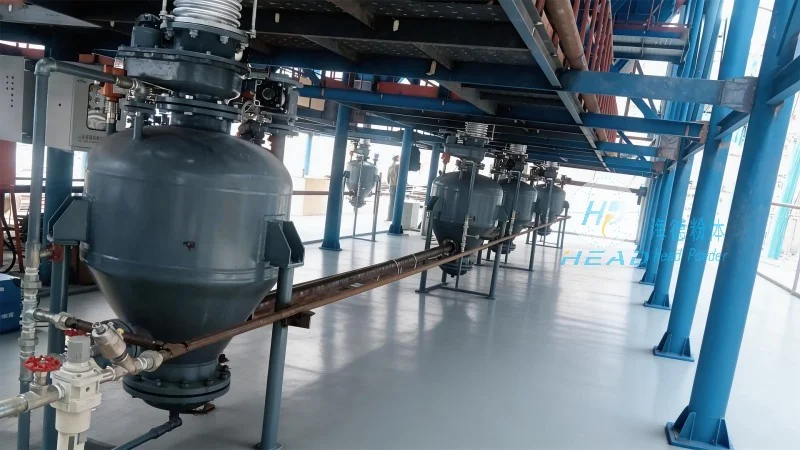
The metering bin pump pneumatic conveying system is widely used in various industries due to its versatility and efficiency. In the food industry, it is commonly used to transport ingredients like flour, sugar, and spices, ensuring hygienic and dust-free handling. In the pharmaceutical sector, the system is employed to convey active pharmaceutical ingredients (APIs) and excipients, maintaining strict contamination control. The chemical industry utilizes the system for transporting powders and granules, such as pigments, catalysts, and reagents, in manufacturing processes. Additionally, the system is used in the agricultural sector for handling fertilizers and seeds, and in the construction industry for transporting cement and other bulk materials. The adaptability of the metering bin pump makes it a preferred choice for industries that require reliable and efficient material transport solutions.
Installation and Maintenance Considerations
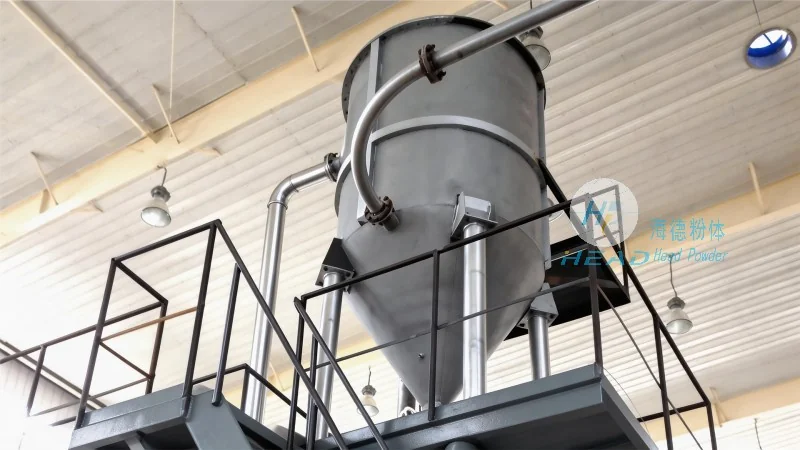
Proper installation and regular maintenance are crucial for the optimal performance and longevity of the metering bin pump pneumatic conveying system. During installation, it is important to ensure that the system is properly aligned and that all connections are secure to prevent air leaks or material blockages. The control system should be configured correctly to match the specific requirements of the application, such as flow rate and pressure settings. Regular maintenance includes checking for wear and tear on the pump components, cleaning the air filters, and inspecting the conveying pipeline for any signs of damage or clogging. By following the manufacturer's guidelines and performing routine maintenance, users can ensure that the system operates efficiently and reliably, minimizing downtime and maintenance costs.
Conclusion
In conclusion, the metering bin pump pneumatic conveying system is a highly efficient and versatile equipment for handling and transporting bulk materials. Its structure and operational principles make it suitable for a wide range of industrial applications, offering advantages such as consistent flow rates, energy efficiency, and low maintenance requirements. With a strong presence in the market, Shandong HeadPowder Engineering Co., Ltd. continues to provide high-quality systems that meet the needs of various industries. By understanding the system's components and working mechanism, users can make informed decisions about its application and ensure optimal performance in their operations.




