Ammonium sulfate, a widely used chemical fertilizer, requires efficient and reliable transportation methods to ensure its safe and timely delivery from production sites to end-users. Pneumatic conveying, a technology that uses air or gas to transport bulk materials, offers several effective solutions for handling ammonium sulfate. This article explores various pneumatic conveying approaches tailored for ammonium sulfate, highlighting the key considerations and benefits of each method.
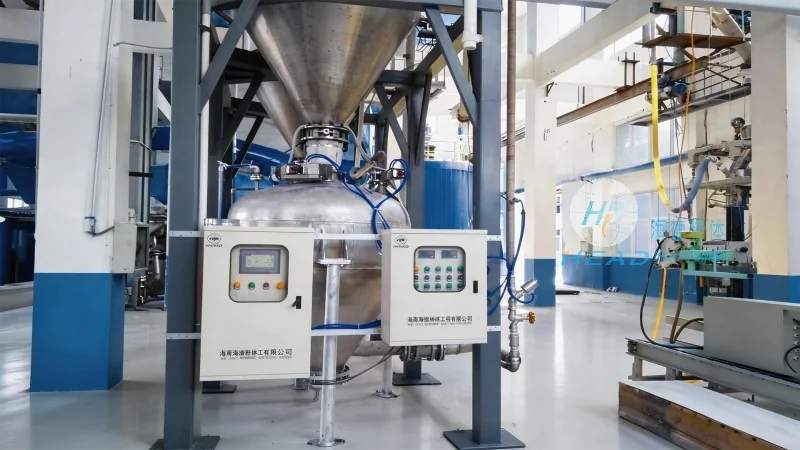
1. Positive Pressure Pneumatic Conveying Systems
Positive pressure systems operate by generating air pressure within the conveying line, pushing the material forward. This method is particularly suitable for ammonium sulfate due to its ability to handle high material loads and maintain consistent flow rates. The system typically includes a blower, a hopper for material storage, and a series of pipes that transport the material. Positive pressure conveying reduces the risk of dust contamination and is ideal for applications where the material needs to be delivered to multiple destinations. The headpowder company, with its expertise in chemical handling, offers customized positive pressure systems that ensure optimal performance and minimal downtime.
2. Negative Pressure (Vacuum) Pneumatic Conveying Systems
Negative pressure systems, also known as vacuum conveying, use a vacuum to draw material from the source into the conveying line. This approach is beneficial for applications where the material is located at a higher elevation or needs to be transported over long distances. Negative pressure conveying is effective for handling fine powders like ammonium sulfate, as it minimizes particle breakage and maintains product integrity. The system comprises a vacuum pump, a receiver, and a series of ducts that pull the material. Shandong HeadPowder Engineering Co., Ltd. specializes in designing vacuum conveying systems that are energy-efficient and environmentally friendly, ensuring compliance with industrial standards.
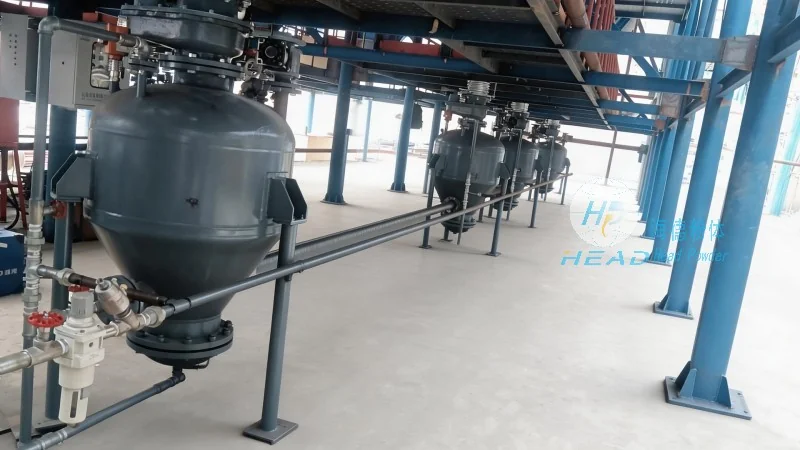
3. Hybrid (Positive and Negative Pressure) Pneumatic Conveying Systems
Hybrid systems combine the advantages of both positive and negative pressure methods, providing flexibility in material handling. These systems are suitable for complex conveying routes that involve multiple elevations and distances. By integrating positive and negative pressure components, the system can handle both upward and downward transport of ammonium sulfate. The headpowder company has developed advanced hybrid solutions that optimize energy consumption and reduce operational costs. This approach is particularly useful for large-scale ammonium sulfate production facilities that require efficient material movement across different parts of the plant.
4. Key Factors to Consider in Pneumatic Conveying of Ammonium Sulfate
When selecting a pneumatic conveying system for ammonium sulfate, several factors must be taken into account. The particle size and moisture content of the material influence the choice of system, as finer particles may require higher air velocities to prevent blockages. The distance and elevation changes between the source and destination also impact the system design. Additionally, the need for dust control and environmental compliance is crucial, as ammonium sulfate is a fine powder that can cause air pollution if not handled properly. The Shandong HeadPowder Engineering Co., Ltd. team conducts thorough assessments to evaluate these factors and recommend the most suitable conveying solution for each client's specific requirements.
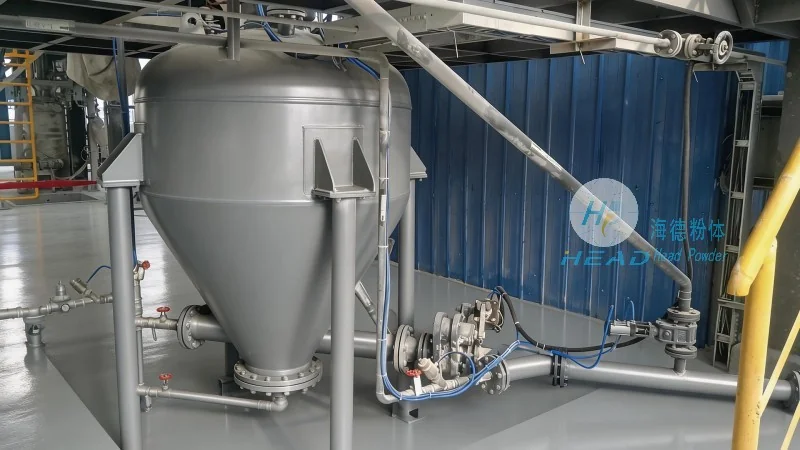
5. Benefits of Implementing Pneumatic Conveying Solutions
Adopting pneumatic conveying systems for ammonium sulfate offers numerous benefits. These include improved safety by reducing manual handling of the material, increased efficiency through automated material transport, and enhanced product quality by minimizing exposure to contaminants. The systems also contribute to cost savings by reducing labor costs and minimizing material loss during transport. Furthermore, the headpowder company's solutions are designed to be scalable, allowing facilities to expand their conveying capabilities as production needs grow. This adaptability ensures long-term investment returns and operational flexibility.
6. Customization and After-Sales Support from HeadPowder
Shandong HeadPowder Engineering Co., Ltd. understands that each ammonium sulfate production facility has unique operational needs. Therefore, the company provides customized pneumatic conveying solutions tailored to specific requirements. From system design and installation to ongoing maintenance and support, headpowder ensures that clients receive comprehensive services throughout the lifecycle of their conveying equipment. The company's technical team works closely with clients to understand their production processes and material characteristics, ensuring that the chosen system meets all operational and safety standards. This personalized approach has made headpowder a trusted partner in the chemical industry, with a reputation for delivering reliable and efficient conveying solutions.




