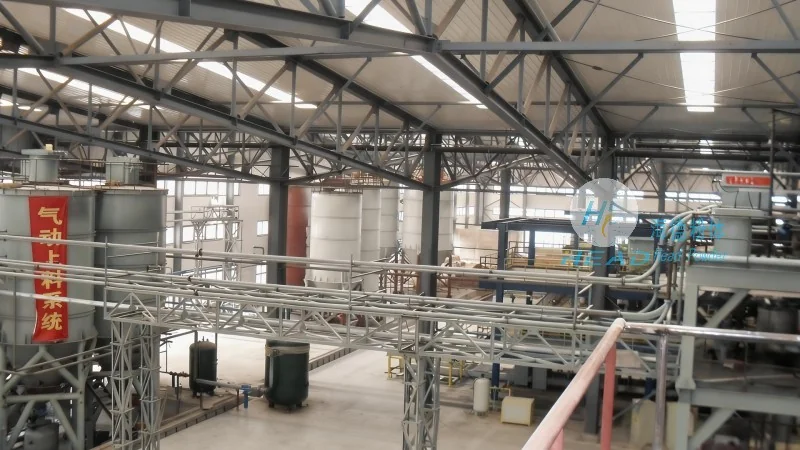
Intelligent tonne bag loading stations are advanced equipment designed for efficient handling and conveying of bulk powder materials. These systems are integral to modern industrial processes, particularly in sectors such as chemical manufacturing, food processing, and pharmaceuticals, where precise and reliable material transfer is critical. The following article provides a detailed overview of the operation process and working principle of such a system, highlighting its key components, operational steps, and technical advantages.
Key Components and Their Functions
The intelligent tonne bag loading station for powder conveying typically consists of several core components, each playing a vital role in the overall system performance. These components include the tonne bag handling mechanism, the powder discharge system, the conveying pipeline, and the control unit. The tonne bag handling mechanism is responsible for securely positioning and opening the bag to allow material discharge. The powder discharge system, often equipped with a rotary valve or a screw conveyor, ensures controlled and consistent material flow from the bag into the conveying system. The conveying pipeline, usually made of stainless steel or other corrosion-resistant materials, transports the powder to the processing unit. The control unit, integrated with sensors and automation technology, manages the entire operation, ensuring safety, efficiency, and compliance with operational parameters.
Operation Process of the Powder Conveying System
The operation process of the intelligent tonne bag loading station begins with the placement of a tonne bag onto the loading platform. The system then uses a mechanical arm or a lifting mechanism to secure the bag and open the top. Once the bag is opened, the powder discharge system starts to extract the material from the bag. The powder is then conveyed through the pipeline to the target destination, such as a silo or a processing machine. The control unit monitors the flow rate, pressure, and other parameters to ensure smooth operation. The entire process is automated, reducing the need for manual intervention and minimizing the risk of material spillage or contamination.
Working Principle of the Tonne Bag Feeding Mechanism
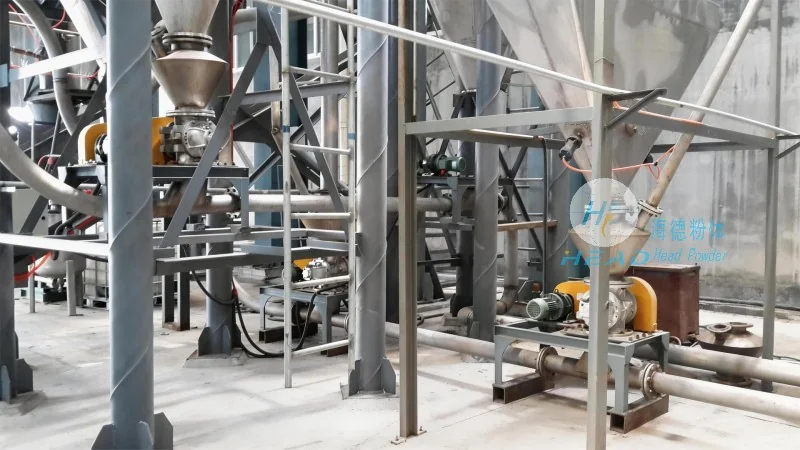
The working principle of the tonne bag feeding mechanism is based on a combination of mechanical and pneumatic systems. The mechanical part includes the bag handling and opening mechanism, which uses hydraulic or electric actuators to position and open the bag. The pneumatic system, often integrated with the discharge valve, controls the flow of air to regulate the powder discharge rate. The conveying system utilizes a positive displacement pump or a screw conveyor to move the powder through the pipeline. The control unit, equipped with sensors such as pressure transducers and flow meters, continuously monitors the system status and adjusts the operation as needed. This closed-loop control ensures that the material is transferred accurately and efficiently, maintaining consistent product quality.
Technical Advantages and Applications
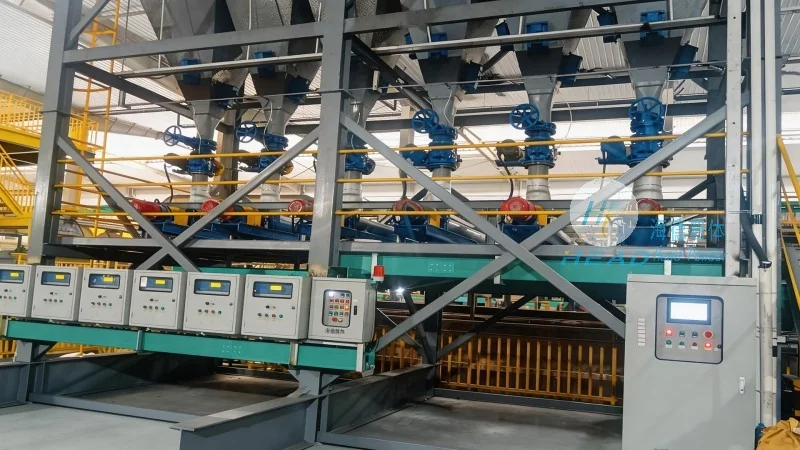
The intelligent tonne bag loading station offers several technical advantages that make it suitable for various industrial applications. One of the key advantages is its high efficiency, as the automated operation reduces processing time and increases production throughput. The system also ensures high material purity by minimizing exposure to air and contaminants, which is crucial for sensitive materials like pharmaceuticals or food products. Additionally, the system is designed for easy maintenance and cleaning, with components that can be easily accessed and replaced. The compact design of the equipment allows for flexible installation in different industrial settings, making it suitable for both new and existing facilities. The application of this technology is widespread across industries, including chemical manufacturing, where it is used for handling raw materials like pigments and additives; food processing, where it is used for handling ingredients like flour and sugar; and pharmaceuticals, where it is used for handling active pharmaceutical ingredients (APIs).
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of powder handling equipment, specializes in the design and production of intelligent tonne bag loading stations. With a focus on innovation and quality, the company has developed advanced solutions that meet the evolving needs of modern industries. HeadPowder's products are engineered to provide reliable and efficient material transfer, ensuring that customers can achieve their production goals while maintaining the highest standards of safety and compliance. The company's headquarters is located in Shandong, China, where it continues to invest in research and development to stay at the forefront of the powder handling industry.




