HeadPowder, a leading provider in the field, specializes in advanced powder handling solutions. The company, based in Shandong, China, has developed a range of innovative systems designed to efficiently transport various types of powders through pneumatic conveying technology. These systems are engineered to meet diverse industrial needs, offering flexibility and reliability in material handling operations.
Core Principles of Pneumatic Conveying Technology
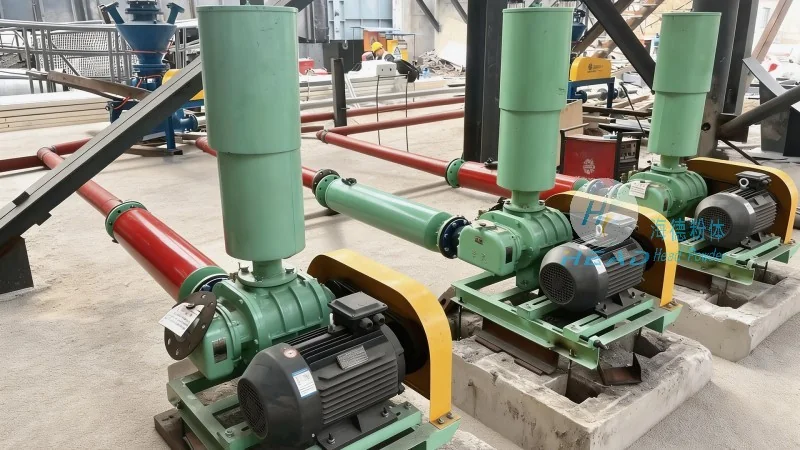
The fundamental principle behind multi-functional powder pneumatic conveying systems is the use of air as the conveying medium to transport bulk powders from one location to another. Unlike traditional mechanical methods, pneumatic systems eliminate the need for moving parts in the conveying path, reducing maintenance requirements and enhancing operational safety. The technology relies on creating a pressure differential or using vacuum to move powders through pipelines, ensuring a smooth and continuous flow. Key components include air movers (such as blowers or vacuum pumps), conveying lines, and control systems that regulate the flow rate and pressure. The design of these systems allows for customization based on the specific characteristics of the powder, including particle size, density, and moisture content. By optimizing the air velocity and pipeline configuration, the systems can achieve high efficiency in transporting powders over long distances with minimal degradation of the material.
Application Scenarios and Operational Advantages
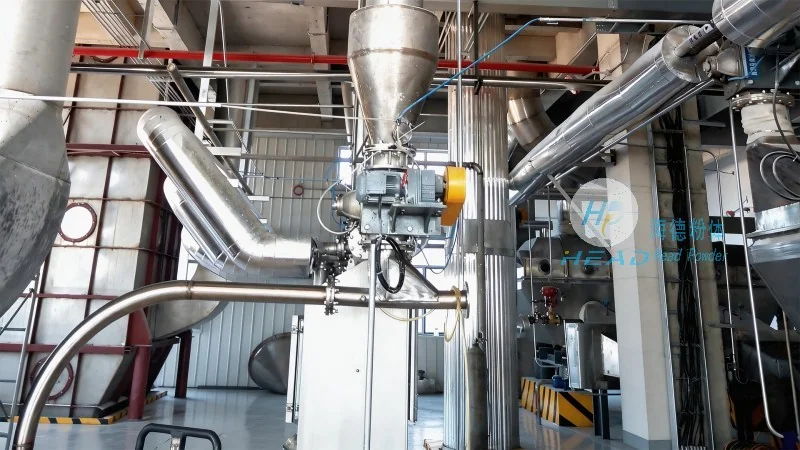
Multi-functional powder pneumatic conveying systems are widely applied in various industrial sectors, including pharmaceuticals, food processing, chemical manufacturing, and cement production. In pharmaceutical applications, these systems ensure the safe and sterile handling of active pharmaceutical ingredients (APIs) and excipients, maintaining product purity and preventing contamination. The systems are designed with sanitary components and easy-to-clean features, meeting stringent regulatory requirements. In the food industry, they are used for transporting dry ingredients like flour, sugar, and spices, preserving the quality and flavor of the products. The gentle handling of powders minimizes agglomeration and breakage, which is crucial for maintaining product integrity. In chemical manufacturing, the systems handle a variety of chemicals, from fine powders to bulk materials, ensuring efficient and safe material transfer. The ability to handle hazardous materials under controlled conditions is a significant advantage, reducing the risk of accidents and environmental contamination. For cement and construction materials, the systems provide reliable transport of raw materials and finished products, supporting high-volume production processes. The operational advantages of these systems include reduced labor costs, increased throughput, and improved product quality. By automating the material handling process, companies can achieve higher productivity and lower operational expenses. The flexibility of the systems allows for integration with existing production lines, minimizing downtime during installation and operation. Additionally, the energy efficiency of pneumatic conveying systems contributes to lower operational costs and environmental sustainability.
Customization and Integration Capabilities
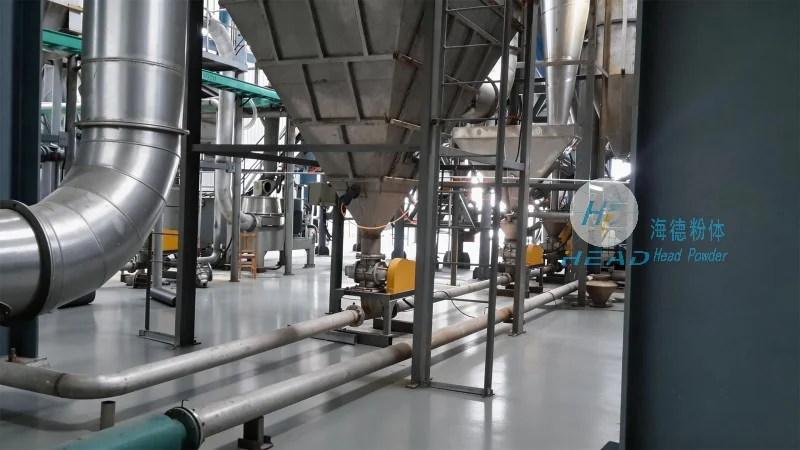
HeadPowder offers tailored solutions to meet the unique requirements of each client. The company’s engineering team works closely with customers to design systems that align with their specific operational needs. Customization options include different types of air movers (positive displacement blowers, centrifugal fans), pipeline materials (stainless steel, PVC, or special alloys), and control systems (manual or automated). The systems can be configured for both pressure and vacuum conveying, allowing for flexibility in handling different powder types and distances. Integration with existing production equipment is seamless, with options for direct connection to silos, hoppers, and processing units. The company provides comprehensive support, including installation, commissioning, and maintenance services, ensuring that the systems operate at optimal performance. By leveraging advanced design and manufacturing capabilities, HeadPowder delivers high-quality, reliable powder conveying solutions that enhance overall operational efficiency.




