Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the powder handling industry, specializes in the design, manufacturing, and integration of advanced conveying systems for various industrial applications. The expanded clay aggregate powder conveying system is a critical component in many production processes, particularly in industries dealing with lightweight aggregates used in construction, horticulture, and other sectors. This system is engineered to efficiently transport fine powders like expanded clay aggregates, ensuring consistent performance and reliability in demanding operational environments.
Principle of the Powder Conveying System
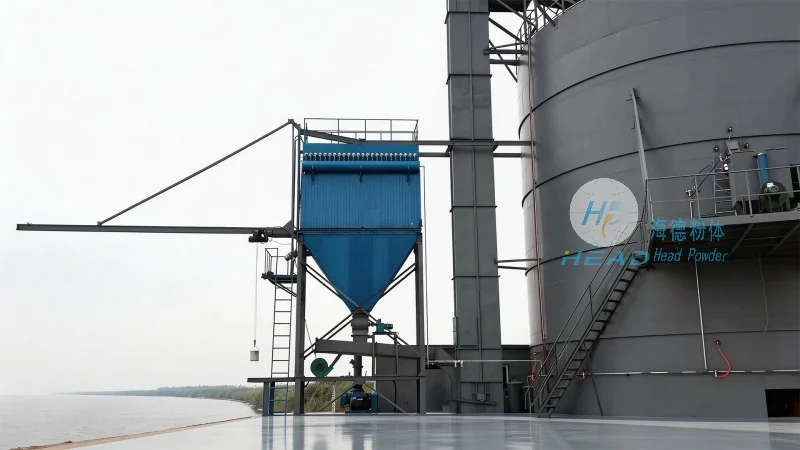
The core principle of the expanded clay aggregate powder conveying system revolves around the use of positive pressure or negative pressure to move powders through a network of pipes and components. The system typically comprises a blower or vacuum pump, a hopper for material storage, a feeder to control the flow rate, and a pipeline network that directs the material to the destination. The operation is based on creating a pressure differential that propels the powder particles along the pipeline. For expanded clay aggregates, which are lightweight and can be prone to bridging or clogging, the system is designed with features such as agitators, air knives, or special hopper geometries to maintain material flow and prevent blockages. The control system, often integrated with sensors for level and flow monitoring, ensures precise regulation of the conveying process, optimizing energy consumption and minimizing material loss.
Key Components and Their Functions
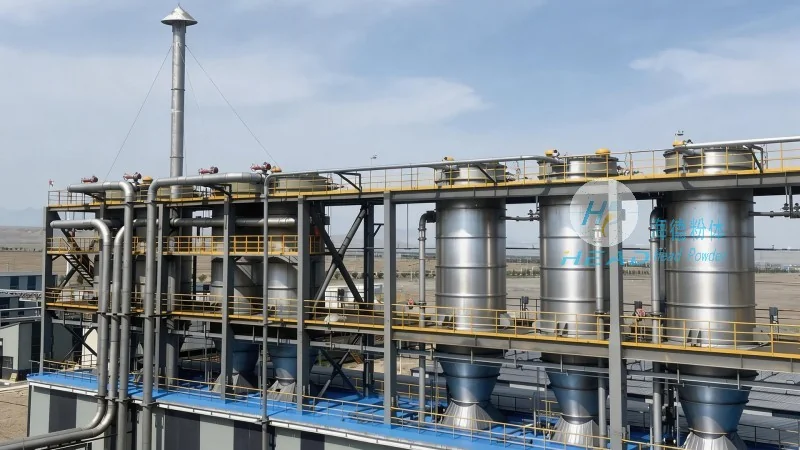
Several key components work in tandem to ensure the efficient operation of the expanded clay aggregate powder conveying system. The blower or vacuum pump provides the necessary air pressure or suction to move the powder. The hopper, usually equipped with a conical or wedge-shaped bottom, helps in feeding the material smoothly into the feeder. The feeder, which can be a rotary valve, screw feeder, or vibratory feeder, regulates the discharge rate of the powder, preventing overloading of the pipeline. The pipeline itself is often made of materials like stainless steel or plastic, chosen for their resistance to corrosion and abrasion from the lightweight aggregates. Additionally, the system may include filters or cyclones to separate any fines or dust, maintaining air quality and protecting downstream equipment. The control panel, equipped with digital displays and programmable logic controllers (PLCs), allows operators to monitor and adjust the system parameters in real-time, enhancing operational flexibility and safety.
Working Scene Characteristics and Application Scenarios
The working scene characteristics of the expanded clay aggregate powder conveying system are tailored to meet the diverse needs of industrial applications. In construction material production, the system is used to transport expanded clay aggregates from storage silos to mixing plants or packaging lines. The lightweight nature of the aggregates makes them ideal for lightweight concrete and insulation materials, where consistent particle size and moisture content are crucial. The system's ability to handle fine powders without clogging is particularly beneficial in such applications, as it ensures uniform material distribution and reduces downtime. In horticulture, the conveying system is used to move expanded clay aggregates used as growing media, where the system's gentle handling prevents damage to the aggregates and maintains their structural integrity. The system's scalability allows it to be adapted for both small-scale and large-scale production facilities, making it suitable for various operational capacities. The working environment, often in industrial plants with high ceilings and large storage areas, requires the system to be robust and durable, with components designed to withstand the rigors of continuous operation. The system's low maintenance requirements and energy efficiency also contribute to its suitability for long-term use in different working scenarios.
Advantages and Benefits in Practical Applications
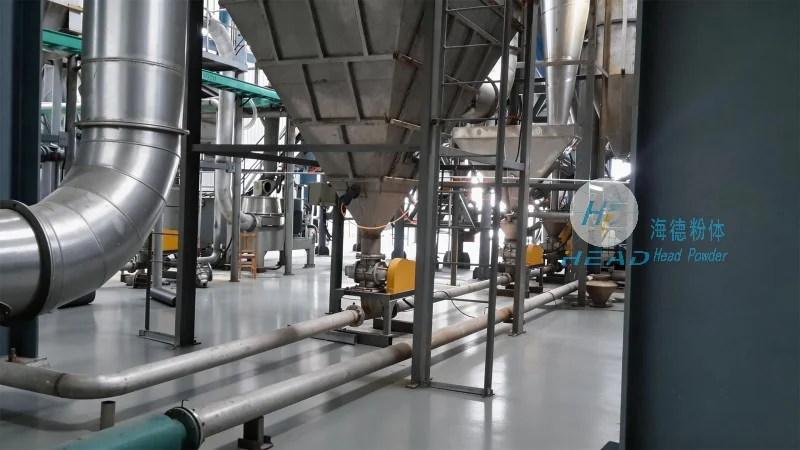
Implementing the expanded clay aggregate powder conveying system offers several advantages that enhance operational efficiency and product quality. The system's ability to handle fine powders with minimal loss and clogging reduces material waste and lowers production costs. The precise control over flow rates and pressure ensures consistent product quality, which is critical in applications where uniform particle size and moisture content are required. The system's compact design and flexible pipeline layout allow for easy integration into existing production lines, minimizing installation time and costs. Additionally, the system's energy efficiency, achieved through optimized air flow and reduced pressure drops, contributes to lower operational expenses and environmental impact. The reliability of the system, with its robust components and advanced control features, reduces downtime and maintenance needs, ensuring continuous production. For industries dealing with expanded clay aggregates, the system provides a cost-effective and efficient solution for material handling, improving overall productivity and competitiveness.




