For industries dealing with bulk fertilizer handling, efficient and reliable material transport is crucial. Powdered fertilizer pneumatic conveying systems offer a sophisticated solution that addresses the challenges of transporting fine particles over long distances. This technology leverages air pressure to move dry, powdered materials, providing a flexible and cost-effective method compared to traditional mechanical conveyors.
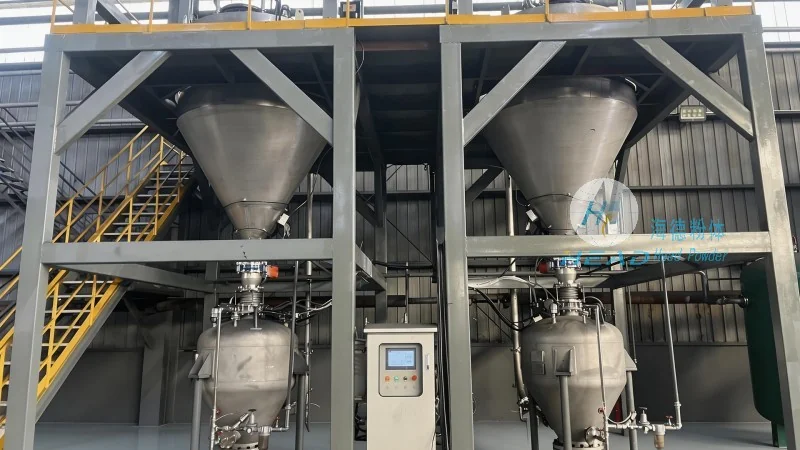
Working Principle of Powdered Fertilizer Pneumatic Conveying
The core mechanism of powdered fertilizer pneumatic conveying involves the use of a pressurized air system to transport dry, granular or powdered materials. The process typically begins with a hopper or storage silo where the fertilizer is stored. From there, the material is drawn into a conveying line by a fan or blower that generates a flow of air. As the air moves through the pipeline, it carries the fertilizer particles along, ensuring a continuous and uniform flow. The system may include components such as a rotary valve, which controls the discharge of material from the hopper, and a filter or cyclone separator that separates the fertilizer from the air at the receiving end, allowing the air to be recirculated or vented safely.
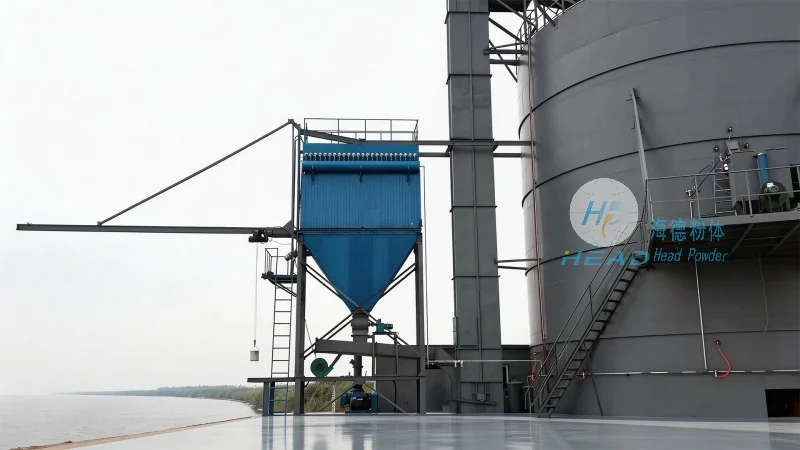
Key Characteristics of Powdered Fertilizer Pneumatic Conveying
Several distinct characteristics make powdered fertilizer pneumatic conveying an attractive option for agricultural and industrial applications. Firstly, it offers high efficiency in material transport, with the ability to move large volumes of fertilizer over significant distances with minimal energy consumption. The system is also highly flexible, as it can be easily adjusted to handle different types of fertilizers, including nitrogen, phosphorus, and potassium compounds, as well as various formulations. Another key characteristic is its low maintenance requirements, as there are fewer moving parts compared to mechanical conveyors, reducing the risk of breakdowns and maintenance costs. Additionally, the system provides excellent control over the flow rate and pressure, allowing for precise dosing and distribution of fertilizer, which is critical for optimizing application rates and reducing waste.
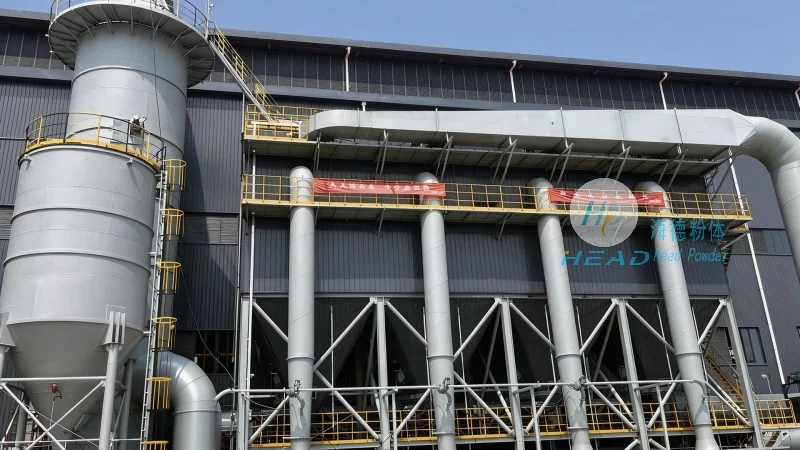
Advantages of Using Powdered Fertilizer Pneumatic Conveying
Implementing a powdered fertilizer pneumatic conveying system brings numerous advantages to operations. One of the most significant benefits is the reduction in labor costs, as the automated process minimizes the need for manual handling of heavy or dusty materials. This not only improves safety in the workplace but also enhances productivity by streamlining the material transport process. The system also contributes to environmental sustainability by reducing dust emissions and minimizing the risk of material spillage, which is particularly important for handling sensitive fertilizers that can be harmful if released into the environment. Furthermore, the compact design of pneumatic conveying systems allows for easier integration into existing facilities, making it a viable option for both new and retrofit projects. The ability to handle fine particles without causing blockages or degradation is another advantage, ensuring that the quality of the fertilizer remains intact throughout the transport process.
Applications in Fertilizer Handling
Powdered fertilizer pneumatic conveying systems are widely used in various stages of the fertilizer supply chain. From manufacturing plants where raw materials are processed into powdered forms, to storage facilities where bulk fertilizer is stored before distribution, and finally to agricultural fields where precise application is required. The systems are particularly effective in large-scale agricultural operations, where the need to transport large quantities of fertilizer over long distances is common. They are also used in industrial settings, such as chemical plants and food processing facilities, where the handling of fine powders is necessary. The versatility of the system allows it to adapt to different operational needs, whether it's for short-distance transport within a facility or long-distance delivery to remote agricultural sites.
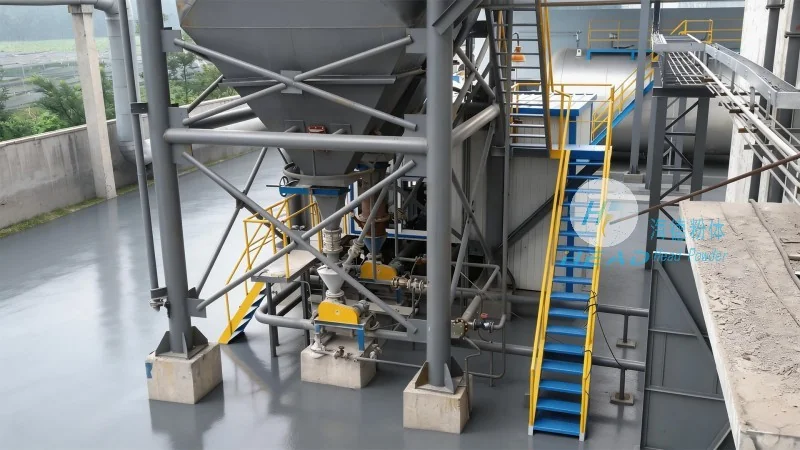
Conclusion and Company Overview
Overall, powdered fertilizer pneumatic conveying represents a modern and efficient solution for the transport of bulk fertilizer. By leveraging air pressure to move fine particles, this technology offers significant advantages in terms of efficiency, flexibility, and cost-effectiveness. For companies operating in the fertilizer industry, investing in such a system can lead to improved operational performance, reduced costs, and enhanced safety. Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for material handling, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of fertilizer producers and distributors. With a focus on quality and innovation, HeadPowder ensures that their systems meet the highest standards of performance and reliability, helping clients optimize their fertilizer handling processes and achieve their business objectives.




