Wheat bran material handling systems are essential in various industrial applications, particularly in food processing and agricultural sectors. These systems are designed to efficiently transport wheat bran, a byproduct of wheat milling, from one processing stage to another. The equipment used in such systems must be capable of handling the unique properties of wheat bran, including its fine texture, light weight, and potential for dust generation. A well-designed material handling system ensures optimal workflow, reduces material loss, and maintains product quality throughout the processing chain.
Working Principle of Wheat Bran Material Handling Equipment
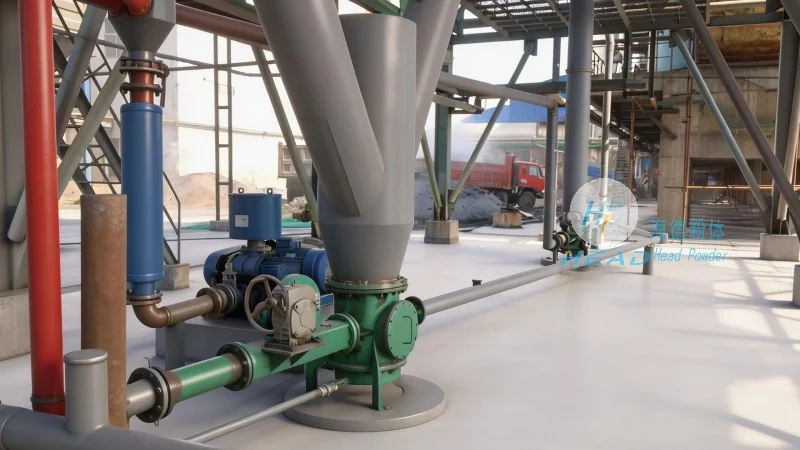
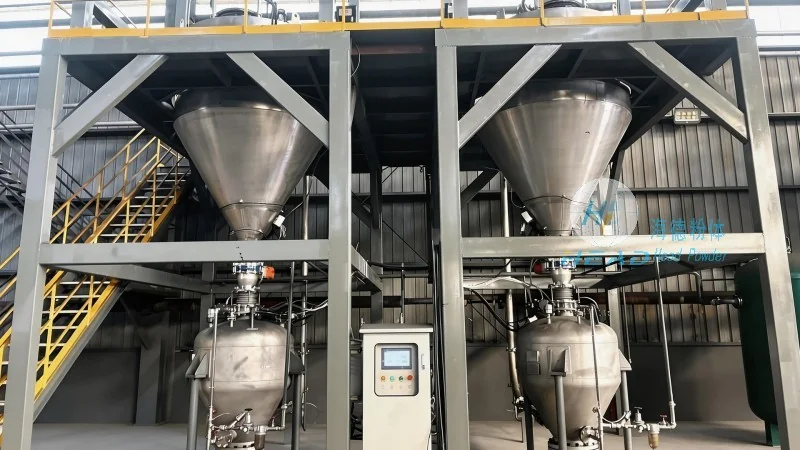
The working principle of wheat bran material handling systems typically involves several key components and mechanisms. One common method is the use of screw conveyors, which utilize a rotating screw to move material along a trough. This type of equipment is ideal for vertical or inclined transport, as it can handle the fine particles of wheat bran without causing excessive wear or blockages. Another popular option is the belt conveyor, which uses a continuous belt to transport material horizontally or at a slight incline. Belt conveyors are particularly effective for longer distances and can be equipped with various accessories, such as hoppers and feeders, to enhance material flow. Additionally, pneumatic conveying systems may be employed for more delicate or dust-sensitive applications, where air pressure is used to transport wheat bran through pipes. Each of these methods operates based on the principles of mechanical or pneumatic force, ensuring reliable and consistent material movement.
Key Features of Wheat Bran Material Handling Systems
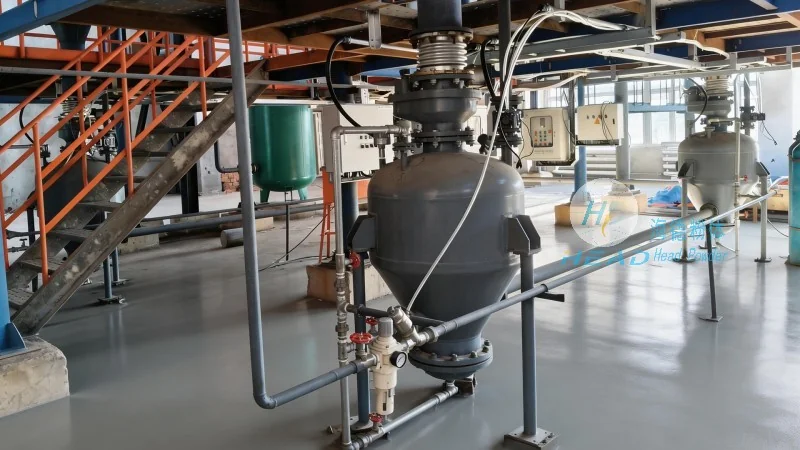
Wheat bran material handling systems from Shandong HeadPowder Engineering Co., Ltd. are characterized by several advanced features that enhance their performance and efficiency. One notable feature is the use of high-quality materials in the construction of conveyor components, such as stainless steel or corrosion-resistant alloys, which are resistant to the acidic and abrasive nature of wheat bran. This ensures long-term durability and minimal maintenance. Another key feature is the integration of variable speed drives, allowing operators to adjust the conveyor speed based on the processing requirements. This flexibility helps optimize energy consumption and prevent overloading, which can lead to system failures. Furthermore, the systems are equipped with advanced control systems, including sensors and monitoring devices, that provide real-time feedback on material flow and system performance. These features enable proactive maintenance and ensure that the system operates at peak efficiency. The design also incorporates dust control measures, such as sealed housings and dust collection systems, to minimize environmental impact and maintain a safe working environment.
Company Information and Location
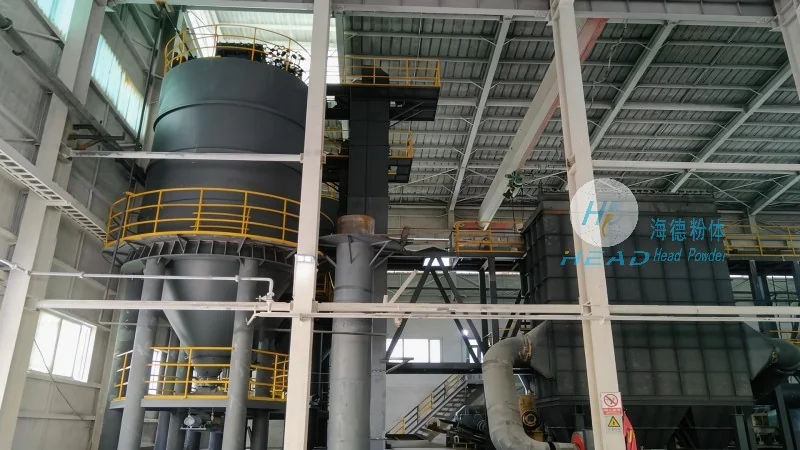
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of material handling solutions, is based in Shandong, China. The company specializes in the design, manufacturing, and installation of custom material handling systems tailored to the specific needs of its clients. With years of experience in the industry, HeadPowder has developed a reputation for delivering high-quality, reliable equipment that meets the stringent requirements of food processing and agricultural applications. The company's facilities in Shandong are equipped with state-of-the-art technology and skilled personnel, ensuring that each system is manufactured to the highest standards. By choosing HeadPowder, clients can benefit from expert guidance and support throughout the entire project lifecycle, from initial design to final installation and maintenance.




