When it comes to efficient and reliable handling of bulk powders, the tote bag unloading powder conveyor stands out as a critical piece of equipment in various industrial applications. This machinery is specifically designed to streamline the process of transferring bulk materials from tote bags into processing systems, storage silos, or other handling equipment. The operation of this conveyor system is built on a combination of mechanical components and intelligent control mechanisms that ensure smooth and consistent material flow.
Working Principle of Tote Bag Unloading Powder Conveyors
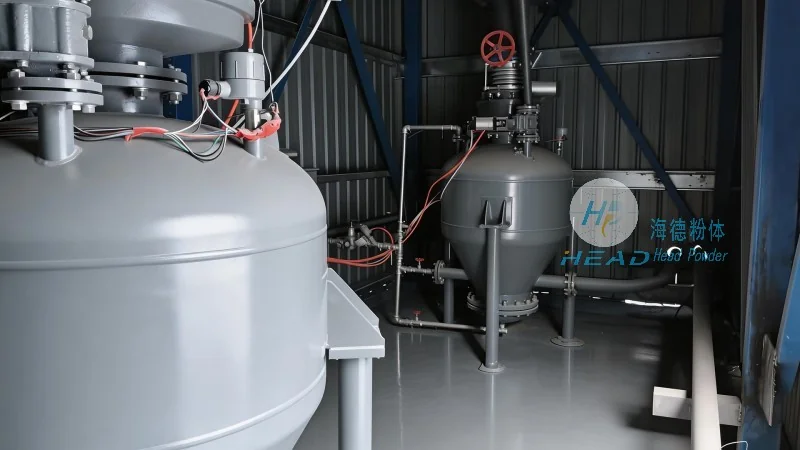
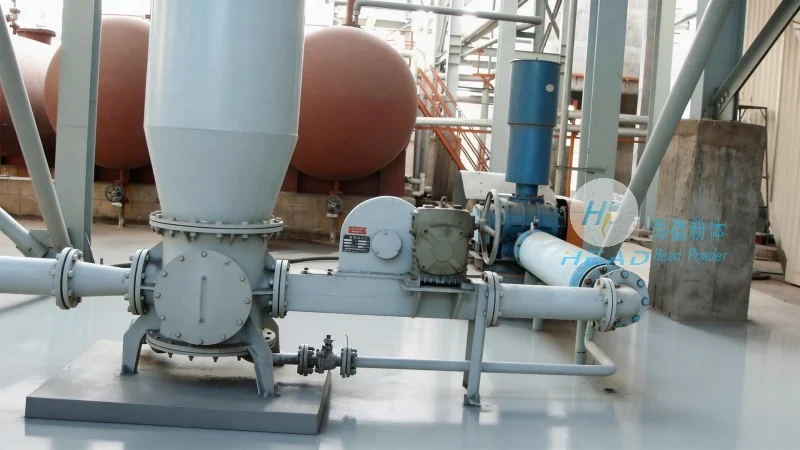
The working principle of a tote bag unloading powder conveyor involves several key steps that work in tandem to achieve efficient material transfer. The process typically begins with the placement of a tote bag containing the powder material onto the conveyor's loading platform. The system then uses a combination of lifting mechanisms, such as hydraulic or mechanical lifts, to raise the tote bag to an elevated position. This elevation allows for the opening of the tote bag's discharge port, which may be equipped with a valve or other opening mechanism. Once the tote bag is elevated and the discharge port is opened, the conveyor's internal components, including a hopper and a conveyor belt or screw mechanism, come into play. The material is then discharged from the tote bag into the hopper and subsequently transported along the conveyor system to the desired destination. The entire process is often automated, with sensors and control systems monitoring the flow rate, ensuring consistent and controlled material transfer. The system may also include features like level sensors to detect the material level in the hopper, preventing overfilling or underfilling. Additionally, some models incorporate dust collection systems to manage airborne particles and maintain a clean working environment. The integration of these components ensures that the tote bag unloading powder conveyor operates efficiently, minimizing downtime and maximizing productivity.
Key Features of Tote Bag Unloading Powder Conveyors
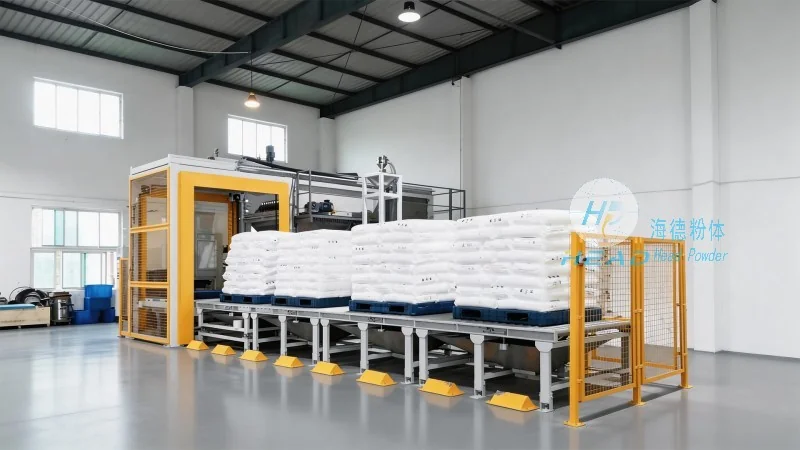
HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design and manufacturing of high-quality tote bag unloading powder conveyors. These systems are engineered with several key features that enhance their performance and reliability. One of the primary features is the robust lifting mechanism, which is designed to handle the weight of the tote bags and the material within them. The lifting system is typically equipped with safety features, such as overload protection, to prevent damage to the equipment and ensure operator safety. The discharge port of the tote bag is often equipped with a valve or other opening mechanism that allows for controlled discharge of the material. This feature helps to prevent spillage and ensures that the material is transferred in a controlled manner. The conveyor system itself is designed to handle various types of powders, including fine powders, granules, and bulk materials. The internal components, such as the hopper and conveyor belt or screw, are constructed from materials that are resistant to corrosion and wear, ensuring long-term durability. The system may also include adjustable speed controls, allowing operators to regulate the flow rate of the material based on processing requirements. Additionally, the conveyor is equipped with sensors and monitoring systems that provide real-time feedback on the material flow, helping to detect any issues or inefficiencies. The integration of these features makes the tote bag unloading powder conveyor a versatile and reliable solution for bulk material handling in various industries.
Applications and Benefits in Industrial Settings
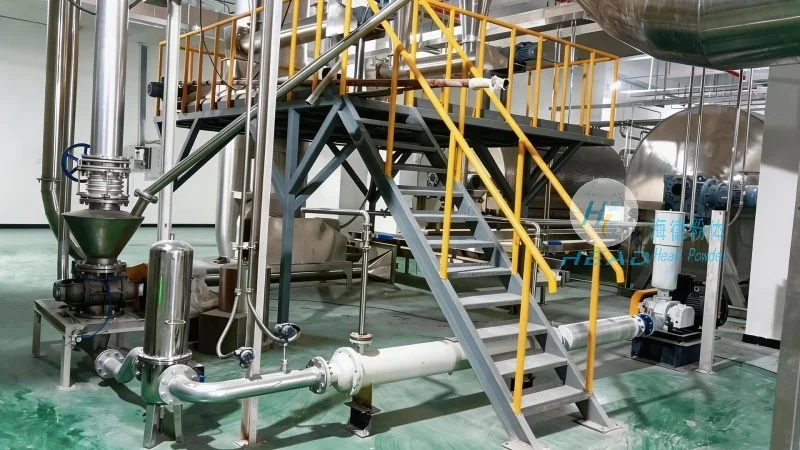
The tote bag unloading powder conveyor is widely used in various industrial sectors, including pharmaceuticals, food processing, chemical manufacturing, and mining. In these industries, the efficient handling of bulk powders is crucial for maintaining production efficiency and product quality. The conveyor system helps to reduce manual labor, as the process of unloading tote bags is automated, minimizing the risk of human error and improving safety. The system also helps to maintain a clean and controlled environment, as the discharge of material is contained within the conveyor system, preventing dust and contamination. The ability to handle various types of powders makes the conveyor versatile and suitable for different applications. The system's design allows for easy integration with existing processing systems, ensuring seamless operation. The benefits of using a tote bag unloading powder conveyor include increased productivity, reduced downtime, and improved material handling efficiency. The system's reliability and durability also contribute to lower maintenance costs over time. By streamlining the process of unloading tote bags, the conveyor helps to improve overall operational efficiency and reduce the risk of material loss or contamination.




