HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder silo pneumatic conveying systems. These systems are engineered to efficiently handle bulk powder materials, ensuring smooth and reliable material transfer from storage silos to processing equipment. The following sections will explore the fundamental working principle and key features of these systems, highlighting their importance in modern industrial applications.
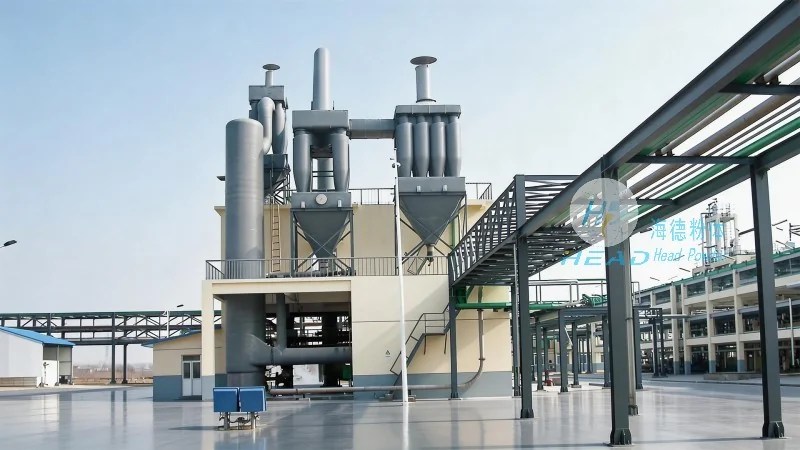
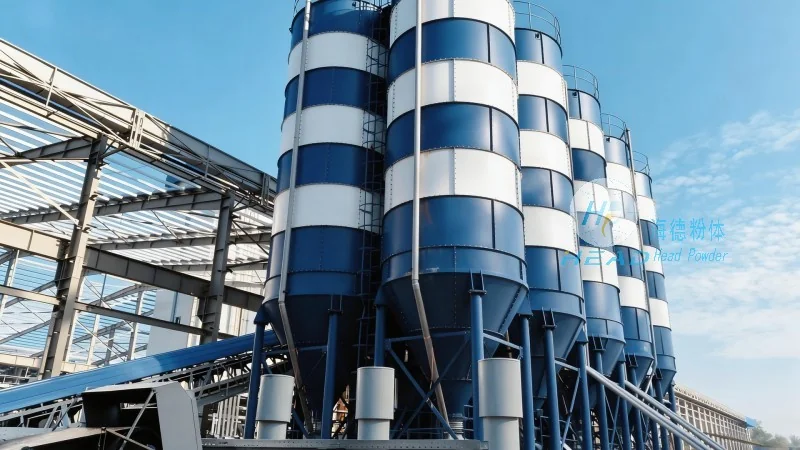
The Working Principle of Powder Silo Pneumatic Conveying Systems
The core operation of a powder silo pneumatic conveying system involves the use of compressed air to transport powder materials through a network of pipes. The process typically begins with the powder being drawn from the storage silo into a hopper or feeder. From there, the powder is introduced into a conveying line where it is mixed with the air stream, creating a dense or dilute phase flow depending on the system design. The compressed air, often supplied by a blower or compressor, provides the necessary force to move the powder particles through the pipeline. As the powder travels, it may encounter various components such as bends, filters, and control valves that regulate the flow and ensure the material reaches its destination without clogging or degradation. The system's efficiency is largely determined by the air pressure, flow rate, and the characteristics of the powder being conveyed, including particle size, density, and moisture content.
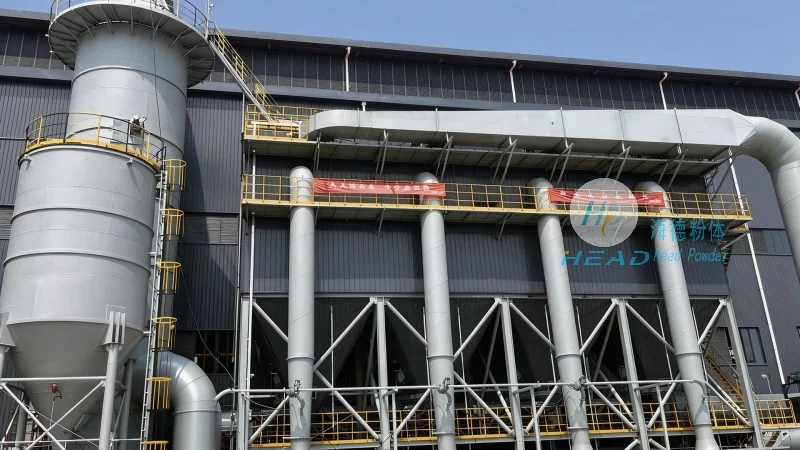
Key Features of Powder Silo Pneumatic Conveying Systems
HeadPowder's powder silo pneumatic conveying systems are characterized by several notable features that enhance their performance and reliability. Firstly, the systems are designed for high efficiency, minimizing material loss and ensuring consistent flow rates. This is achieved through optimized air-powder ratios and advanced control mechanisms that maintain stable operation under varying load conditions. Secondly, the equipment is built for durability and long-term performance, utilizing high-quality materials and robust construction to withstand the abrasive nature of powder handling. The systems also incorporate safety features, such as pressure relief valves and particle filters, to protect against overpressure and contamination. Additionally, the modular design allows for easy integration with existing industrial setups, making it suitable for both new installations and retrofits. Another key feature is the ability to handle a wide range of powder types, from fine powders like cement and flour to bulk materials like plastic pellets and chemical powders, without requiring significant modifications to the system. This versatility makes the systems adaptable to diverse industrial applications, including pharmaceuticals, food processing, and chemical manufacturing.
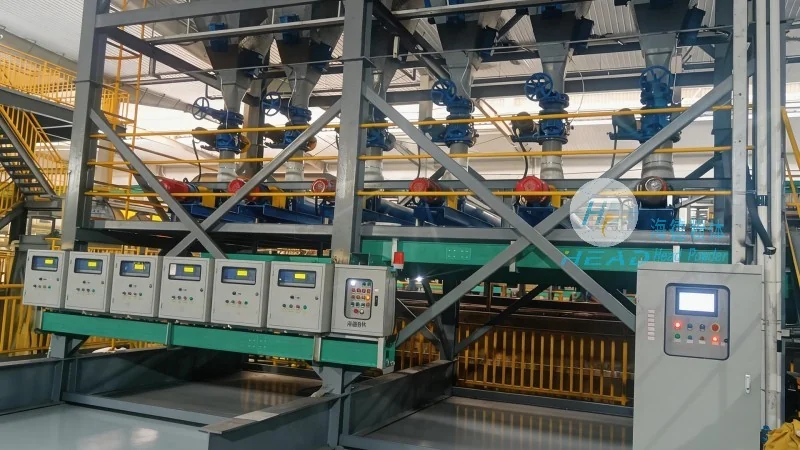
Applications and Benefits in Industrial Settings
Powder silo pneumatic conveying systems from HeadPowder find extensive applications across various industries, offering significant benefits to manufacturers. In the food and beverage sector, these systems ensure hygienic and efficient transfer of ingredients like flour, sugar, and spices, maintaining product quality and preventing cross-contamination. In the pharmaceutical industry, the systems are critical for handling sensitive powders, as they provide a closed-loop operation that minimizes exposure to environmental factors and ensures compliance with regulatory standards. The chemical industry also benefits from these systems, as they enable safe and controlled transfer of reactive or hazardous powders, reducing the risk of accidents and improving workplace safety. The primary benefits of using such systems include improved operational efficiency, reduced labor costs, and enhanced product quality. By eliminating manual handling and reducing material waste, the systems contribute to cost savings and increased productivity. Furthermore, the closed-loop design helps maintain a clean and controlled environment, which is essential for industries where product purity is paramount.




