

Working Principle and Features of Cement Tank Truck Pneumatic Conveying Systems
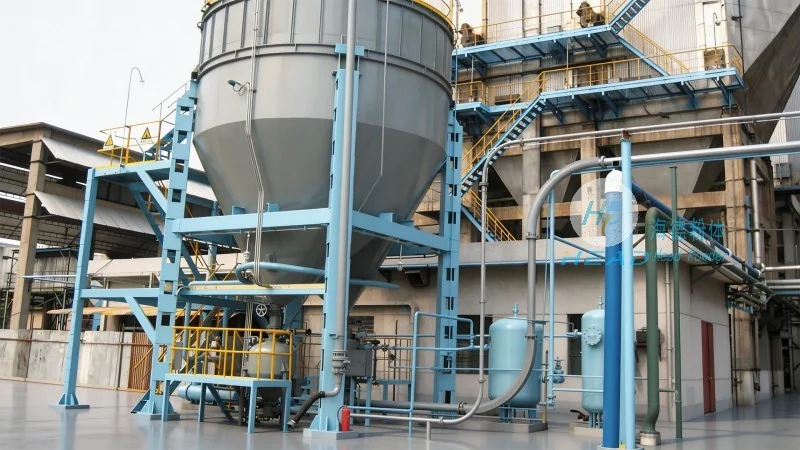
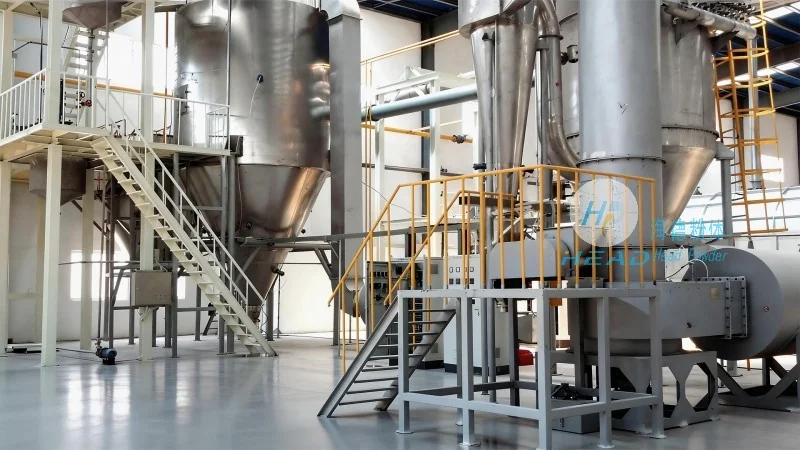
Cement tank truck pneumatic conveying systems operate based on the fundamental principle of using compressed air to transport bulk materials like cement. The process begins with the cement being loaded into the tank truck, where it is then transferred to a receiving hopper or silo through a series of air-driven mechanisms. The system typically involves a blower that generates high-pressure air, which is directed into the conveying line. As the air flows through the pipeline, it creates a low-pressure zone that draws the cement particles into the air stream. This mixture of air and cement travels through the pipeline to the destination, where it is separated from the air and deposited into the storage facility. The entire process is controlled by a system of valves, regulators, and sensors that ensure efficient and safe material transfer.
Key Features of Cement Tank Truck Pneumatic Conveying Systems
One of the primary advantages of cement tank truck pneumatic conveying systems is their high efficiency in material handling. Unlike traditional methods such as bucket elevators or belt conveyors, pneumatic systems can transport cement over longer distances with minimal labor and operational costs. The systems are also highly flexible, allowing for easy integration with existing infrastructure and the ability to adapt to varying production demands. Additionally, pneumatic conveying offers superior control over the material flow, reducing the risk of dust emissions and ensuring a cleaner working environment. The technology is designed to handle different types of cement, including powdered and granular varieties, making it versatile for various industrial applications. Another notable feature is the system's ability to maintain consistent material quality by preventing contamination and ensuring uniform mixing during transport. The use of advanced materials and engineering in the construction of the conveying lines further enhances durability and longevity, reducing maintenance requirements over time.
Applications and Benefits in Cement Industry Operations
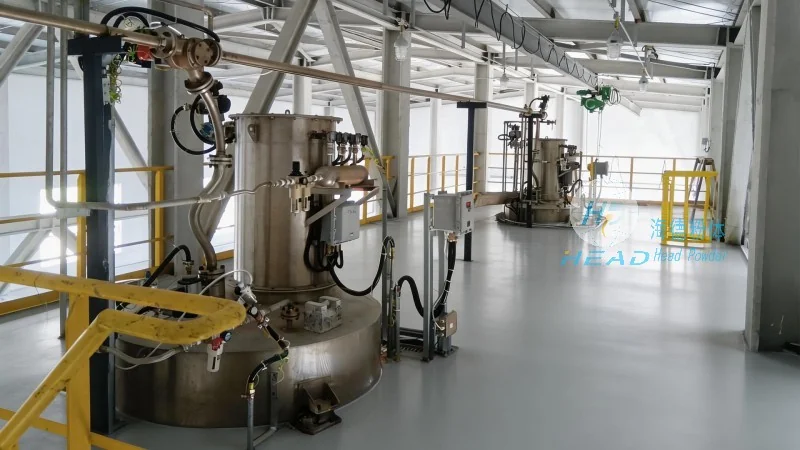
Cement tank truck pneumatic conveying systems are widely used in the cement industry for both internal and external material transfer. Internally, they facilitate the movement of cement from production plants to storage silos or distribution centers, ensuring a smooth supply chain. Externally, these systems enable the efficient delivery of cement to construction sites, reducing the time and cost associated with traditional truck loading and unloading. The systems are particularly beneficial in areas where space is limited or where the need for quick, reliable delivery is critical. By minimizing downtime and improving operational efficiency, pneumatic conveying systems contribute to increased productivity and reduced operational costs for cement manufacturers. The technology also supports environmental compliance by reducing dust emissions and improving air quality at industrial sites. Overall, the integration of pneumatic conveying systems in cement operations enhances both operational performance and sustainability for its clients.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
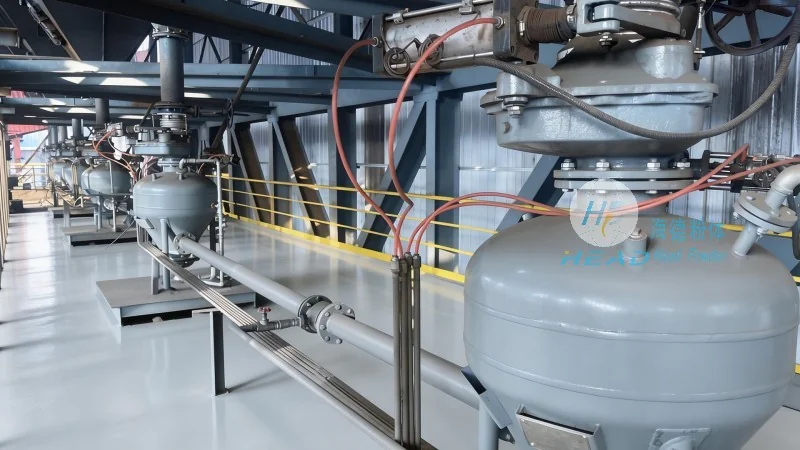
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial material handling solutions, specializes in the design, manufacturing, and installation of cement tank truck pneumatic conveying systems. With a strong commitment to quality and innovation, the company has established itself as a trusted partner in the cement industry. HeadPowder's expertise lies in developing customized solutions that meet the specific needs of clients, ensuring optimal performance and reliability. The company's facilities are located in Shandong, China, where it leverages advanced technology and skilled workforce to deliver high-quality products. By adhering to international standards and employing rigorous quality control measures, HeadPowder ensures that its pneumatic conveying systems are durable, efficient, and cost-effective. The company's focus on customer satisfaction and long-term partnerships has earned it a reputation for excellence in the industry. With a dedicated team of engineers and technicians, HeadPowder continues to advance the technology of cement handling, providing solutions that enhance operational efficiency and sustainability for its clients.