

Working Principle and Features of Rare Earth Powder Pneumatic Conveying Systems
When it comes to efficiently transporting rare earth powders, the pneumatic conveying system stands out as a highly effective solution. This technology utilizes air or gas to move powders through a pipeline, offering a clean, dust-free, and flexible method for material handling. The working principle of such a system typically involves several key components and processes that work in tandem to ensure smooth operation.
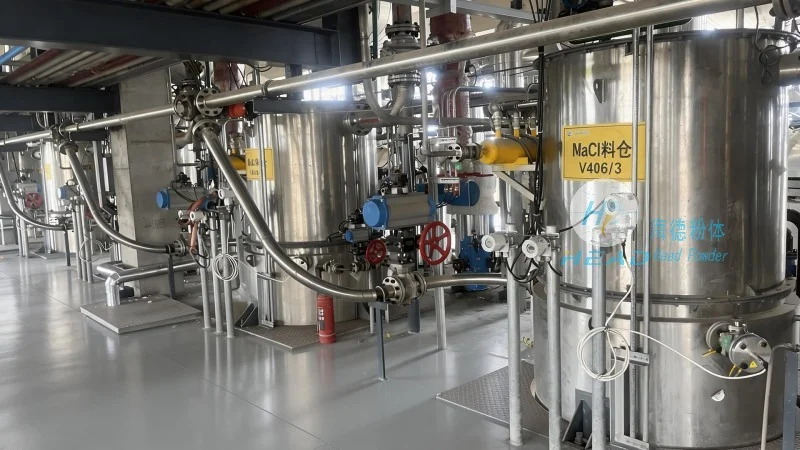
At the core of a rare earth powder pneumatic conveying system is the material feed section. Here, the rare earth powder is introduced into the system, often through a hopper or a feeder that controls the flow rate. This initial step is crucial for maintaining consistent material supply and preventing blockages. The powder then moves into the conveying line, where it is carried by the air flow. The system may employ different types of conveyors, such as positive pressure or negative pressure systems, depending on the specific requirements of the application.
Positive pressure systems, for instance, use a blower or a compressor to generate air pressure that pushes the powder through the pipeline. This method is particularly effective for long-distance or high-capacity conveying. On the other hand, negative pressure systems create a vacuum that draws the powder into the pipeline, which is often preferred for applications where dust control is a priority. The choice between these systems depends on factors like the powder's properties, the distance to be covered, and the desired flow rate.
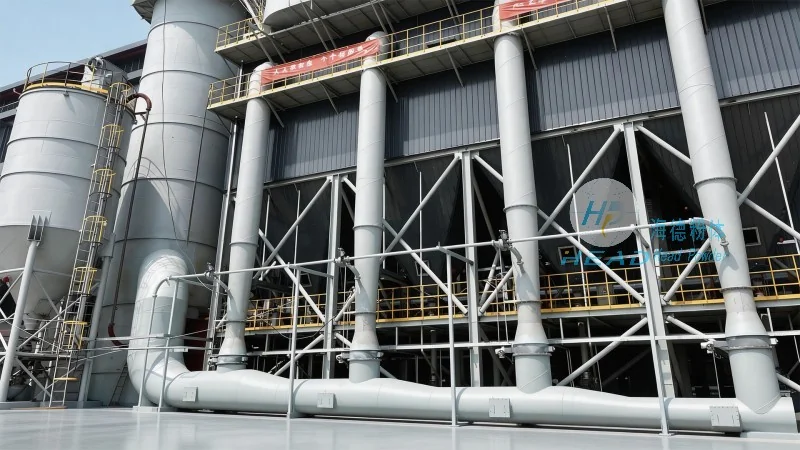
Another critical component is the air separation and cleaning system. As the powder travels through the pipeline, it eventually reaches a separator where the air and powder are separated. The powder is then collected in a receiving hopper or a storage tank, while the air is either filtered and recycled or discharged. This step is vital for maintaining system efficiency and ensuring that the powder remains in a clean state, free from contaminants that could affect downstream processes.
Now, let's explore the key features that make rare earth powder pneumatic conveying systems advantageous. First, the system offers a dust-free operation, which is essential for handling rare earth powders that can be hazardous if inhaled. By containing the material within a sealed pipeline, the risk of dust exposure is significantly reduced, enhancing workplace safety. Second, the flexibility of the system allows for easy integration with existing production lines. The pipelines can be configured in various shapes and sizes to suit the layout of the facility, making it adaptable to different operational needs.
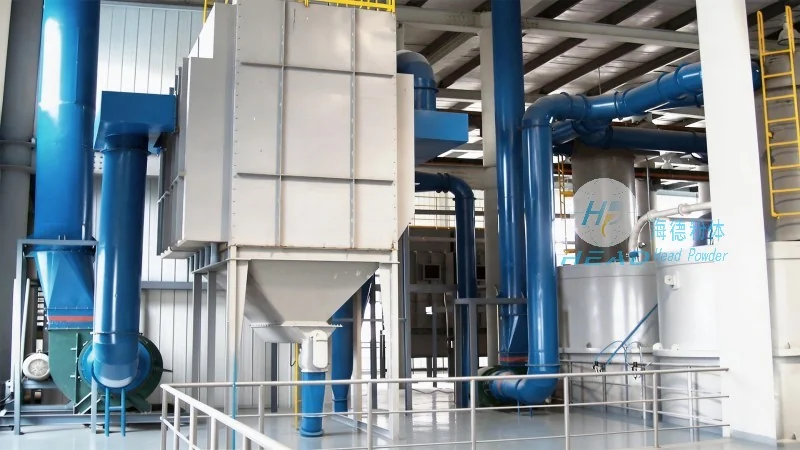
Third, the system provides a high degree of control over the material flow. By adjusting the air pressure or flow rate, operators can precisely control the speed and volume of the powder being conveyed. This level of control is particularly important in processes where the quality of the material is critical, such as in the production of rare earth magnets or other high-value applications. Additionally, the system can handle a wide range of powder characteristics, including different particle sizes, densities, and moisture contents, making it versatile for various rare earth powder types.
Fourth, the pneumatic conveying system contributes to energy efficiency and cost savings. Compared to traditional methods like belt conveyors or bucket elevators, pneumatic systems can reduce energy consumption and maintenance costs. The absence of moving parts in the conveying line minimizes wear and tear, leading to lower operational expenses over time. Moreover, the system's ability to handle materials in a closed environment reduces the need for additional dust collection equipment, further enhancing cost-effectiveness.
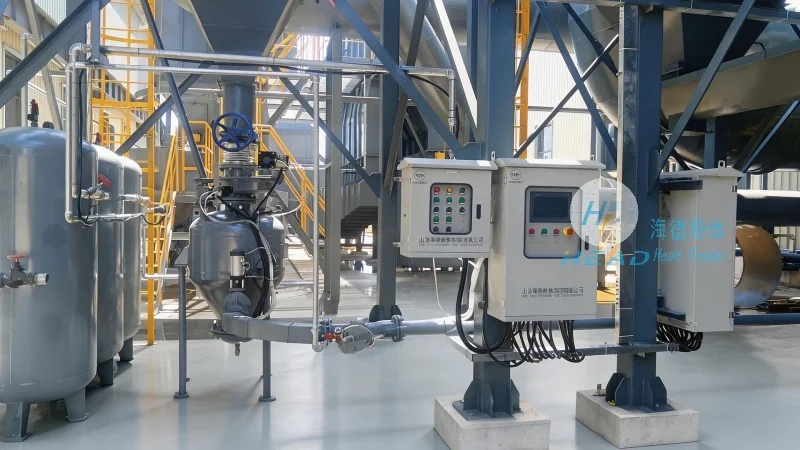
For companies dealing with rare earth powders, the choice of a suitable conveying system is paramount. The rare earth powder pneumatic conveying system, as offered by Shandong HeadPowder Engineering Co., Ltd., combines advanced technology with robust design to meet the demanding requirements of the industry. With a focus on efficiency, safety, and adaptability, this system ensures reliable and consistent material handling, supporting the smooth operation of production processes. The company's expertise in engineering and manufacturing ensures that each system is tailored to the specific needs of the client, providing a customized solution that enhances productivity and reduces operational risks.
Shandong HeadPowder Engineering Co., Ltd., based in China, specializes in the design, manufacturing, and installation of pneumatic conveying systems for various industrial applications. Their commitment to quality and innovation has made them a trusted partner in the rare earth powder processing industry. By leveraging years of experience and advanced engineering capabilities, the company delivers systems that are not only efficient but also durable and easy to maintain. Whether for short or long-distance conveying, the system from HeadPowder Engineering Co., Ltd. offers a reliable solution that meets the highest standards of performance and safety.