Mineral particle conveying is a critical process in various industrial sectors, including mining, chemical manufacturing, and food processing. The efficient and reliable transport of mineral particles from one location to another is essential for maintaining production efficiency and ensuring product quality. Over the years, several methods have been developed to handle this task, with each offering unique advantages and limitations. This article provides an overview of the primary mineral particle conveying methods, with a particular focus on the advantages and features of pneumatic conveying, a widely used technology in the industry.
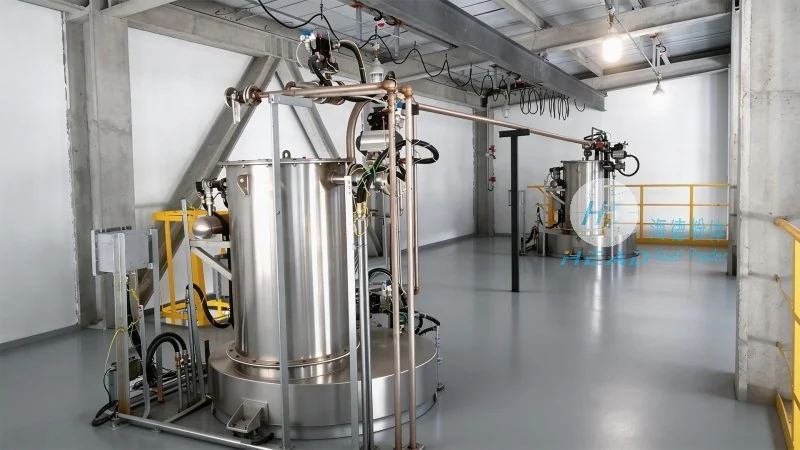
Common Conveying Methods for Mineral Particles
Before delving into the specifics of pneumatic conveying, it is important to understand the broader landscape of mineral particle transport. Traditional methods such as belt conveyors, screw conveyors, and bucket elevators have been the workhorses of material handling for decades. Belt conveyors, for instance, are ideal for long-distance horizontal or slightly inclined transport of bulk materials, including minerals. They are cost-effective and can handle large volumes, but they require significant space and may be prone to wear and tear from abrasive particles. Screw conveyors, on the other hand, are suitable for vertical or inclined transport and are often used in applications where space is limited. However, they are less effective with very fine or sticky particles and can experience clogging issues. Bucket elevators are designed for vertical transport and are particularly useful in applications where the material needs to be lifted to a significant height. Despite their effectiveness, these mechanical systems often face challenges related to maintenance, energy consumption, and the ability to handle diverse particle sizes and characteristics.
Pneumatic Conveying: A Detailed Overview
Pneumatic conveying, also known as air conveying, is a method that uses a pressurized or vacuum system to transport solid particles through a pipeline using air or other gases. This technology has gained significant popularity in the mineral processing industry due to its versatility and ability to handle a wide range of particle sizes, shapes, and moisture content. Unlike mechanical conveyors, pneumatic systems do not require physical contact with the material, reducing the risk of contamination and wear. The process typically involves a hopper or feeder where the mineral particles are introduced into a pipeline. The air, either under pressure or suction, then carries the particles through the system, delivering them to the desired destination. Pneumatic conveying can be categorized into two main types: pressure and vacuum systems. Pressure systems use compressed air to push the material through the pipeline, while vacuum systems use a vacuum to draw the material into the pipeline. Each type has its own set of applications and advantages, making them suitable for different operational requirements.
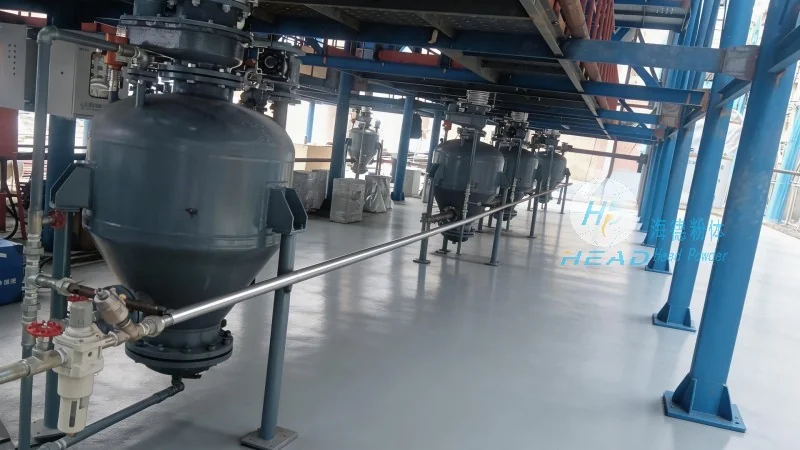
Key Advantages of Pneumatic Conveying for Mineral Particles
The adoption of pneumatic conveying for mineral particles is driven by several key advantages that make it a preferred choice in many industrial settings. One of the most significant benefits is the ability to handle diverse particle characteristics. Pneumatic systems can efficiently transport fine powders, coarse granules, and even wet or sticky materials without the risk of clogging or degradation. This versatility is particularly valuable in industries where the material properties vary widely, such as in mining operations where ore types and sizes can differ significantly. Another major advantage is the reduced risk of contamination. Since the material is conveyed through a closed pipeline system, it is protected from external contaminants, including dust, moisture, and other environmental factors. This is crucial in applications where product purity is paramount, such as in pharmaceutical or food processing industries. Additionally, pneumatic conveying offers improved safety and hygiene. The enclosed system minimizes dust emissions, reducing the risk of respiratory issues for workers and preventing product contamination from airborne particles. This makes it an ideal solution for applications where environmental and health regulations are stringent.
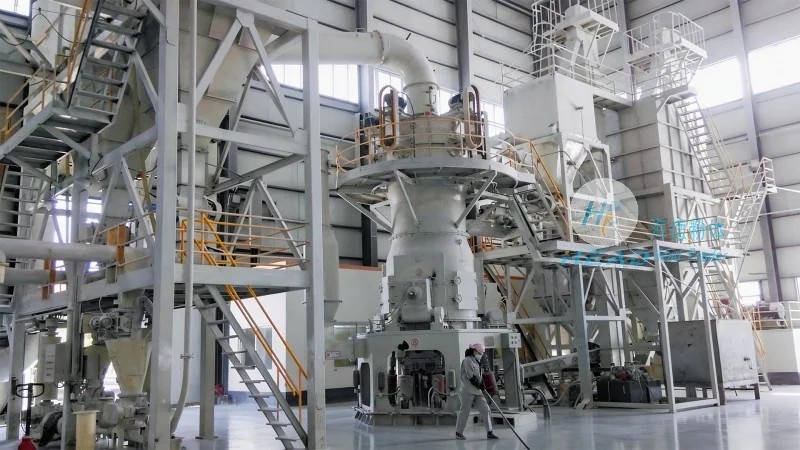
Technical Features and Applications
Pneumatic conveying systems for mineral particles are equipped with several technical features that enhance their performance and reliability. These features include variable speed drives, which allow for precise control over the conveying rate, ensuring consistent material flow. The use of high-quality materials, such as stainless steel or special alloys, in the construction of the pipeline and components ensures durability and resistance to corrosion, particularly in environments with aggressive minerals or chemicals. Advanced control systems, including sensors and monitoring devices, provide real-time feedback on system performance, enabling operators to detect and address issues promptly. This proactive approach to maintenance helps to minimize downtime and maximize operational efficiency. The applications of pneumatic conveying in the mineral processing industry are diverse and widespread. In mining operations, it is used for transporting ore from the mine to processing facilities, as well as for conveying tailings and waste materials. In chemical plants, it is employed to move raw materials and finished products through various stages of production. In food processing, it is utilized for handling grains, powders, and other food ingredients, ensuring hygienic and efficient transport. The flexibility of pneumatic systems allows them to be integrated into existing production lines or used as standalone solutions, making them a versatile choice for a wide range of industrial applications.
Conclusion and Company Information
Mineral particle conveying is a complex process that requires careful consideration of the material properties, operational requirements, and environmental factors. While traditional mechanical conveyors have served the industry well, pneumatic conveying has emerged as a superior solution in many applications due to its versatility, efficiency, and safety features. The advantages of pneumatic conveying, including its ability to handle diverse particle characteristics, reduced contamination risk, and improved safety, make it an attractive option for industries seeking to enhance their material handling processes. As the demand for efficient and reliable mineral processing technologies continues to grow, pneumatic conveying is likely to remain a key component of industrial operations. For businesses looking to implement or upgrade their mineral particle conveying systems, it is essential to partner with experienced and reputable suppliers who can provide tailored solutions that meet specific operational needs. Shandong HeadPowder Engineering Co., Ltd., a leading provider of mineral processing equipment, offers a range of pneumatic conveying solutions designed to meet the diverse requirements of the industry. With a focus on quality, innovation, and customer satisfaction, HeadPowder provides comprehensive support, from system design and installation to maintenance and troubleshooting. Located in Shandong, China, HeadPowder leverages its expertise and advanced technology to deliver reliable and efficient mineral particle conveying solutions that help businesses optimize their operations and achieve their production goals.




