Understanding the operational principles of a corn cob pneumatic conveying system is crucial for optimizing material handling efficiency in agricultural processing facilities. This system, designed by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, leverages pneumatic technology to transport corn cobs with precision and reliability.
System Overview and Core Components
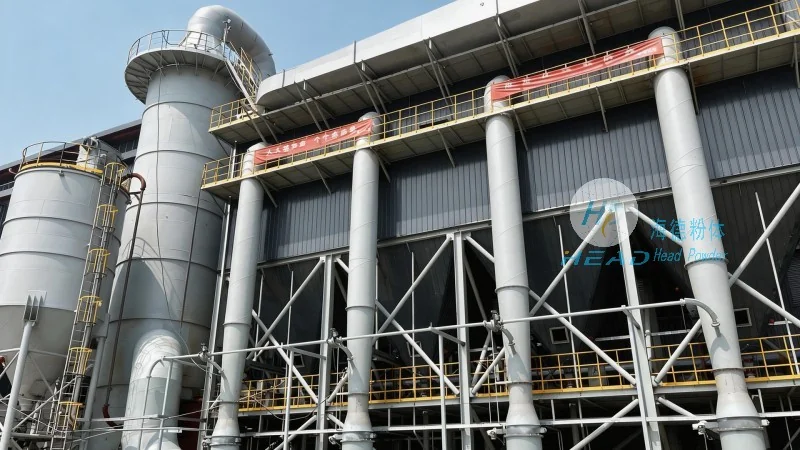
The corn cob pneumatic conveying system consists of several key components that work in tandem to facilitate the movement of corn cobs from the source to the destination. These include a hopper for material storage, a conveyor line equipped with air ducts, a pressure vessel or receiver to collect the conveyed material, and a control system to regulate airflow and pressure. Each component is engineered to ensure seamless integration and minimal downtime, making the system suitable for continuous operation in industrial settings.
Working Principle of Pneumatic Conveying
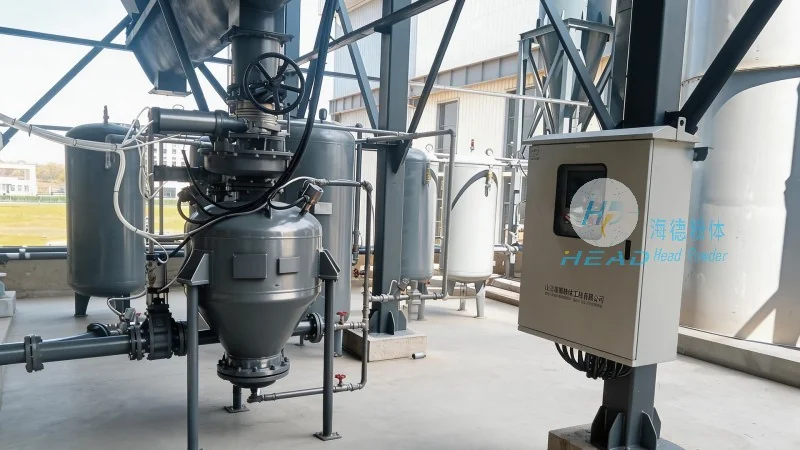
The fundamental principle behind the corn cob pneumatic conveying system is the use of air pressure to move solid materials. In this system, corn cobs are introduced into the hopper, where they are then drawn into the conveyor line by a vacuum or pressure differential created by the system's blower. The air, carrying the corn cobs, travels through the ductwork to the receiving vessel. As the material is deposited, the air is filtered and recycled back into the system, maintaining a closed-loop operation that reduces energy consumption and environmental impact.
Advantages of the Corn Cob Pneumatic Conveying System
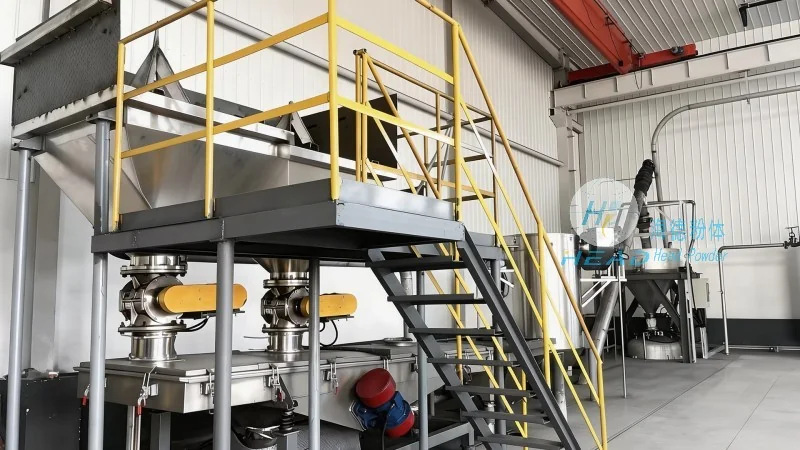
Compared to traditional mechanical conveyors, the pneumatic system offers several advantages that enhance operational efficiency and product quality. Firstly, it eliminates the need for physical contact between the corn cobs and the conveyor components, reducing the risk of material damage or contamination. Secondly, the system can handle a wide range of particle sizes and moisture contents, making it versatile for different processing stages. Additionally, the enclosed design minimizes dust emissions, contributing to a cleaner working environment and compliance with environmental regulations. The system's ability to operate at varying speeds and capacities also allows for flexible integration into existing production lines.
Application in Agricultural Processing
Shandong HeadPowder Engineering Co., Ltd. has tailored the corn cob pneumatic conveying system for various applications within the agricultural processing industry. These include transporting corn cobs from storage silos to processing machines, moving material between different stages of the corn cob processing line, and delivering finished products to packaging areas. The system's adaptability ensures that it can be customized to meet the specific requirements of each client, whether for small-scale or large-scale operations. By streamlining the material handling process, the system helps to improve overall productivity and reduce labor costs in agricultural processing facilities.
Company Background and Expertise
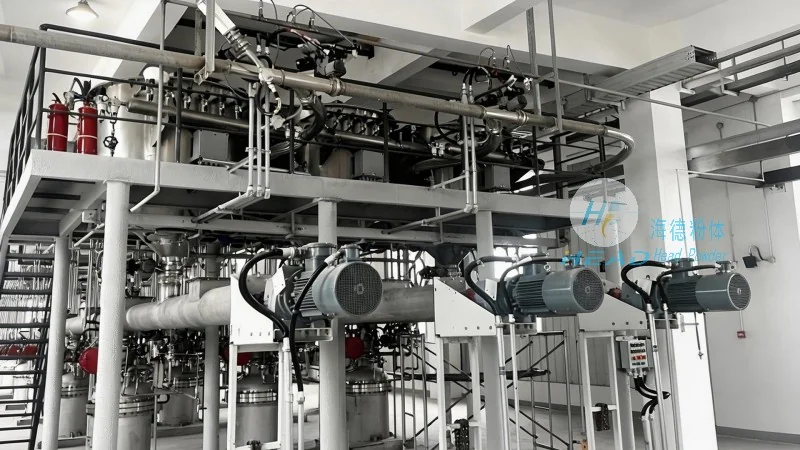
HeadPowder, as the brand of Shandong HeadPowder Engineering Co., Ltd., has established itself as a trusted name in the engineering and manufacturing of pneumatic conveying systems. With a focus on innovation and customer satisfaction, the company has developed a range of solutions tailored to the unique needs of the agricultural sector. HeadPowder's team of engineers and technicians brings extensive experience in designing and implementing efficient material handling systems, ensuring that each project is completed to the highest standards. The company's commitment to quality and reliability has earned it a reputation for delivering durable and long-lasting systems that provide consistent performance over time.




