Pneumatic conveying technology has become an essential method for transporting bulk materials, including white sugar, due to its efficiency, flexibility, and ability to handle delicate products without damage. This article provides an in-depth look at the principles, practical applications, and emerging trends in bulk sugar pneumatic conveying, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd. (HeadPowder), a leading provider in this field based in Shandong, China.
Overview of Pneumatic Conveying for White Sugar
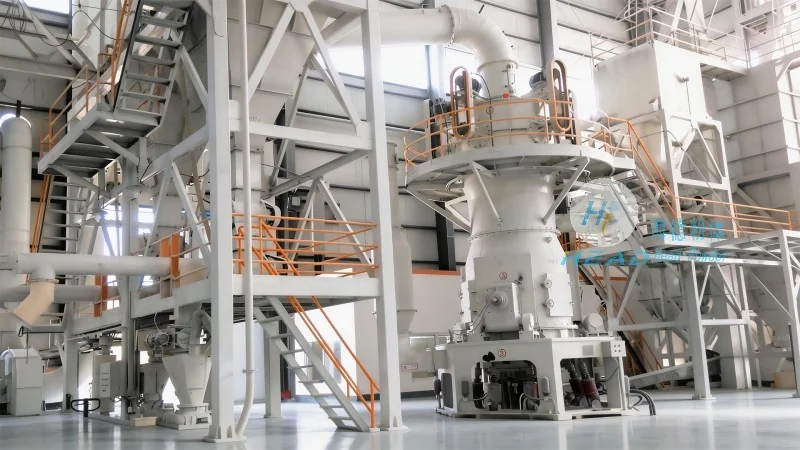
Pneumatic conveying involves the use of air or gas to transport solid materials through a pipeline system. For white sugar, this technology offers several advantages over traditional methods like belt conveyors or bucket elevators. It minimizes product contamination, reduces the risk of breakage or caking, and allows for a more hygienic and controlled environment, which is critical in the food industry. The process typically involves a hopper where the sugar is loaded, a conveyor line with a series of pipes, and a control system that regulates air pressure and flow.
Working Principles of Bulk Sugar Pneumatic Conveying
The core principle of pneumatic conveying for white sugar is based on the creation of a pressure differential that moves the material through the system. There are two main types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems use low air velocity and high material velocity, suitable for short distances and moderate material loads. Dense-phase systems, on the other hand, use higher air pressure and lower material velocity, which is ideal for longer distances and more sensitive products like white sugar, as it reduces the risk of product degradation. The system operates by drawing air into the conveyor line using a vacuum pump (in the case of suction systems) or pushing air through the line using a blower (in the case of pressure systems). The sugar is then entrained by the air and transported to the destination.
Applications in the White Sugar Industry
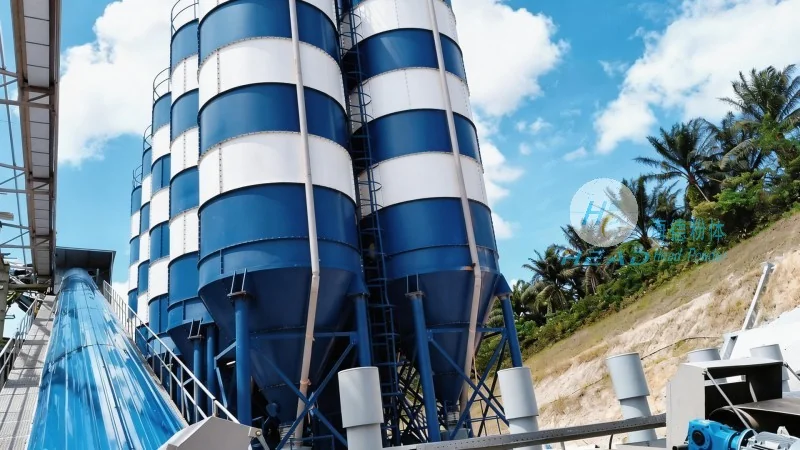
HeadPowder's pneumatic conveying solutions are widely applied in various stages of the white sugar production and handling process. In sugar mills, the technology is used to transport raw sugar from storage silos to processing units, ensuring a continuous and clean flow. During the refining process, pneumatic conveyors help move refined sugar from the crystallization tanks to packaging areas, maintaining product purity. In storage facilities, the system efficiently transfers sugar from bulk storage to intermediate bins or directly to packaging lines, optimizing space utilization and reducing manual handling. Additionally, in food processing plants, the technology is employed to transport sugar for blending with other ingredients, ensuring consistent quality and preventing cross-contamination. The versatility of pneumatic conveying allows it to adapt to different operational requirements, from high-volume production lines to smaller, more specialized applications.
Key Features and Benefits for White Sugar Handling
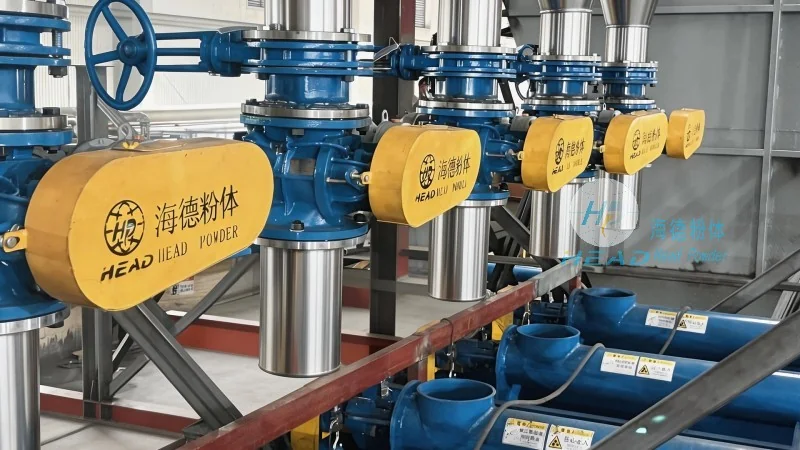
When implementing pneumatic conveying for white sugar, several key features contribute to its effectiveness. First, the system's ability to handle fine, powdery materials without causing caking or blockages is crucial. HeadPowder's designs incorporate specialized hopper and valve configurations that prevent material buildup, ensuring smooth operation. Second, the hygienic design of the equipment, including smooth surfaces and easy-to-clean components, meets the stringent standards of the food industry. This is achieved through materials like stainless steel and the use of sanitary fittings, which minimize the risk of bacterial growth and product contamination. Third, the energy efficiency of pneumatic conveying systems is a significant advantage. By optimizing air pressure and flow rates, HeadPowder's solutions reduce energy consumption compared to traditional mechanical conveyors, leading to lower operational costs over time. Finally, the flexibility of the system allows for easy integration with existing production lines and the ability to adjust conveying rates based on demand, enhancing overall operational efficiency.
Emerging Trends and Technological Advancements
The field of bulk sugar pneumatic conveying is continuously evolving, with several trends shaping its future. One key trend is the integration of advanced control systems and automation. Modern pneumatic conveying systems now feature real-time monitoring and control, allowing operators to adjust parameters such as air pressure, flow rate, and material feed rate based on real-time data. This not only improves efficiency but also enhances safety by preventing over-pressurization or system failures. Another trend is the use of intelligent sensors and IoT (Internet of Things) technology. These sensors can monitor factors like material flow rate, air pressure, and temperature, providing valuable data for predictive maintenance and performance optimization. By analyzing this data, companies can identify potential issues before they become major problems, reducing downtime and maintenance costs. Additionally, there is a growing focus on sustainability and environmental impact. HeadPowder is exploring the use of energy-efficient motors and renewable energy sources to power pneumatic conveying systems, reducing the carbon footprint of sugar handling operations. This aligns with the industry's push towards more sustainable practices and regulatory requirements. Finally, the development of more compact and modular systems is another emerging trend. These systems are designed for easier installation and maintenance, making them suitable for both new and retrofit applications. By reducing the footprint and complexity of the equipment, they offer cost savings and faster deployment times.
Conclusion and Future Outlook
Pneumatic conveying technology remains a cornerstone of efficient and reliable white sugar handling, offering significant advantages over traditional methods. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., the technology continues to evolve, incorporating advanced features and sustainable practices to meet the demands of modern sugar production. As the industry moves towards higher efficiency, hygiene, and sustainability, pneumatic conveying is poised to play an even more critical role in the future of bulk material handling. By leveraging the latest technological advancements and maintaining a focus on quality and innovation, HeadPowder and similar companies are positioned to provide solutions that enhance operational performance and support the long-term success of the white sugar industry.




