Wheat conveyance is a critical process in agricultural and industrial operations, ensuring efficient movement of grain from storage, processing, or packaging stages. Various methods are employed to handle wheat, each with distinct advantages based on the application, scale, and operational environment. This article explores the primary methods of wheat conveyance, focusing on the technologies and equipment used by Shandong HeadPowder Engineering Co., Ltd. (commonly known as HeadPowder), a leading manufacturer based in Shandong, China. The company specializes in designing and manufacturing high-efficiency conveyance systems tailored to the unique needs of wheat handling facilities, from small farms to large-scale industrial operations.
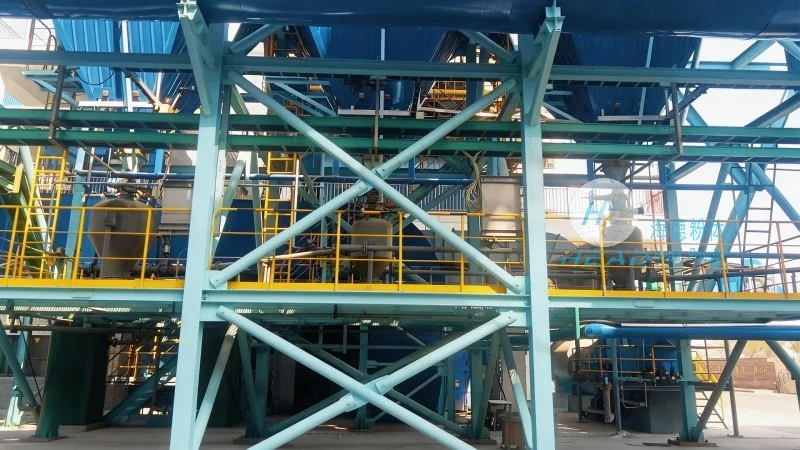
1. Belt Conveyors for Wheat Transport
Belt conveyors are among the most common and versatile equipment for wheat conveyance. These systems utilize a continuous belt, typically made of rubber or synthetic materials, to transport wheat in a linear or inclined path. The belt is supported by rollers and idlers, allowing it to move wheat from one location to another with minimal friction and energy consumption. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality belt conveyors tailored to the specific needs of wheat handling facilities. Their belt conveyors are engineered to handle varying capacities, from small-scale farms to large industrial grain processing plants, ensuring reliable and consistent performance. The company’s expertise in material selection and mechanical design ensures that the conveyors can withstand the abrasive nature of wheat and maintain optimal operational efficiency over extended periods.
2. Bucket Elevators for Vertical Wheat Transport
Vertical transport of wheat often requires bucket elevators, which are ideal for moving grain from lower to higher elevations in a compact and efficient manner. Bucket elevators consist of a vertical or inclined casing with a continuous chain or belt that carries buckets attached to it. As the conveyor rotates, the buckets scoop up wheat from the bottom and discharge it at the top, enabling vertical movement without the need for additional horizontal space. Shandong HeadPowder Engineering Co., Ltd. offers advanced bucket elevator systems that are robust, durable, and capable of handling high volumes of wheat. These elevators are designed with heavy-duty components to resist wear and tear, ensuring long service life and minimal maintenance. The company’s engineers consider factors such as grain size, moisture content, and bulk density when customizing bucket elevators to meet the unique requirements of each client.
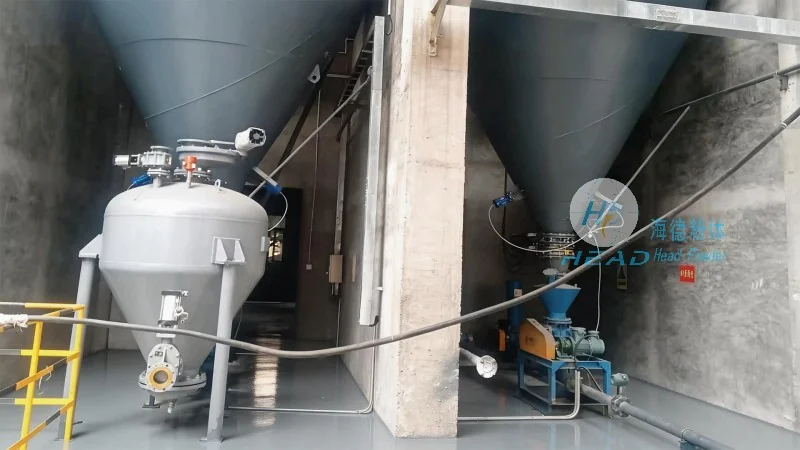
3. Screw Conveyors for Horizontal Wheat Transport
Screw conveyors, also known as augers, are widely used for horizontal or slightly inclined transport of wheat. These systems consist of a rotating screw (helix) enclosed in a cylindrical trough. As the screw rotates, it pushes wheat forward along the trough, allowing for smooth and continuous movement. Screw conveyors are particularly effective for transporting wheat in confined spaces or when a gentle slope is required. Shandong HeadPowder Engineering Co., Ltd. provides screw conveyors with adjustable speed and capacity, enabling operators to control the flow rate of wheat based on processing needs. The company’s screw conveyors are constructed with corrosion-resistant materials and precision-engineered components, ensuring reliable operation in various environments. They are also designed to minimize product degradation, preserving the quality of wheat during transport.
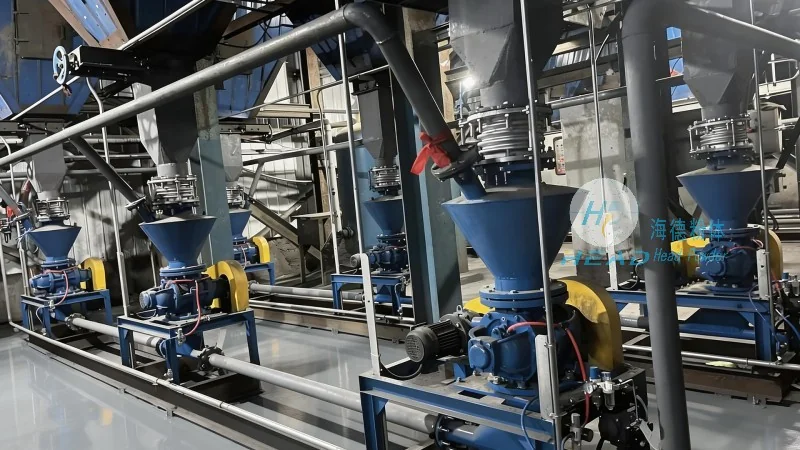
4. Pneumatic Conveying Systems for Wheat Handling
Pneumatic conveying systems use air pressure to transport wheat through a network of pipes, making them suitable for long-distance or complex routing of grain. These systems can be classified as positive or negative pressure systems, depending on whether air is forced into the system or extracted. Positive pressure systems blow air into the pipe, pushing wheat forward, while negative pressure systems create a vacuum to draw wheat into the pipe. Shandong HeadPowder Engineering Co., Ltd. offers pneumatic conveying solutions that are energy-efficient and capable of handling fine or bulk wheat particles. The company’s systems are equipped with advanced controls to regulate air flow and pressure, ensuring consistent and safe transport. Pneumatic conveyors are particularly advantageous in environments where dust control and hygiene are critical, as they can be enclosed and sealed to prevent contamination.
5. Combination Systems for Integrated Wheat Conveyance
In many industrial settings, a single conveyance method may not be sufficient to meet all operational requirements. Shandong HeadPowder Engineering Co., Ltd. specializes in designing integrated conveyance systems that combine multiple technologies to optimize wheat handling. For example, a facility might use a belt conveyor to transport wheat from storage to a bucket elevator, which then moves it vertically to a processing line. The company’s engineers work closely with clients to develop customized solutions that integrate belt conveyors, bucket elevators, screw conveyors, and pneumatic systems into a cohesive workflow. These combination systems enhance overall efficiency, reduce downtime, and improve the quality of wheat handling by minimizing manual intervention and ensuring smooth transitions between stages. The company’s expertise in system integration ensures that each component works in harmony, maximizing the performance and reliability of the entire conveyance process.




