Understanding the design and operational principles of nitrile rubber pneumatic conveying systems is crucial for industries that handle this specialized material. These systems are engineered to efficiently transport nitrile rubber, a polymer known for its excellent resistance to oil, fuel, and various chemicals, while maintaining the integrity of the material and ensuring safe, reliable operation.
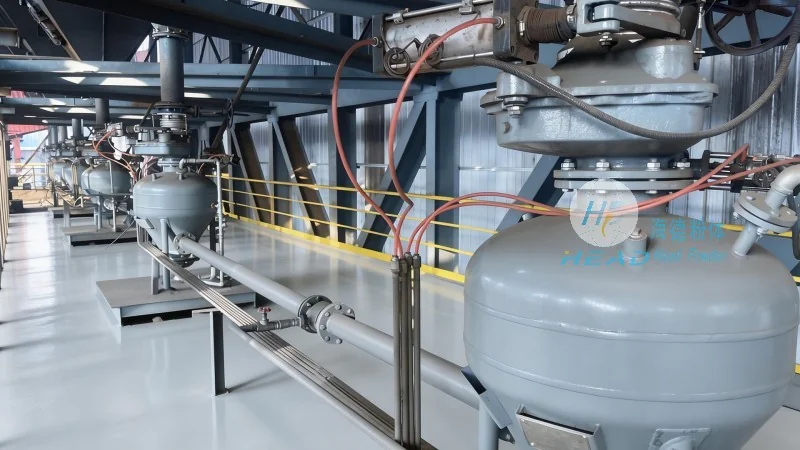
Structural Components and Working Principles
The core components of a nitrile rubber pneumatic conveying line typically include a hopper for material storage, a feeder to control the flow rate, a conveying pipeline, a dust collector to manage airborne particles, and a discharge unit for material release. The system operates on the principle of air flow, where compressed air is used to create a vacuum or pressure differential that propels the nitrile rubber particles through the pipeline. This method eliminates the need for mechanical components like belts or chains, reducing wear and maintenance requirements.
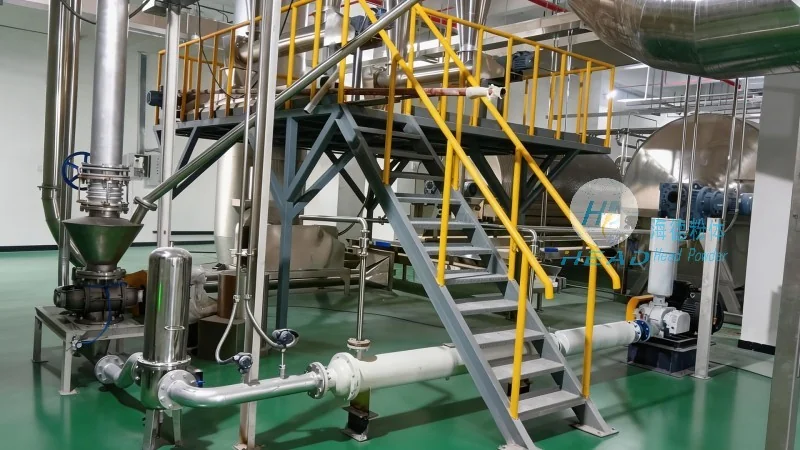
Key Features and Advantages
One of the primary advantages of nitrile rubber pneumatic conveying systems is their ability to handle abrasive or sticky materials without causing degradation. The smooth interior surfaces of the pipelines and the controlled air flow minimize material friction and prevent clogging. Additionally, these systems offer flexibility in layout, allowing for vertical, horizontal, or mixed-direction transport, which is beneficial for complex production environments. The enclosed design also enhances safety by containing dust and preventing exposure to hazardous materials.
Application Scenarios and Industry Relevance
Nitrile rubber pneumatic conveying lines are widely used in the manufacturing of automotive parts, seals, and gaskets, where the material's chemical resistance is critical. They are also employed in the production of industrial hoses, rubber flooring, and medical devices that require high-quality, contamination-free rubber components. The systems are particularly suitable for applications requiring high throughput and consistent material quality, as they can maintain stable flow rates and prevent material degradation during transport.
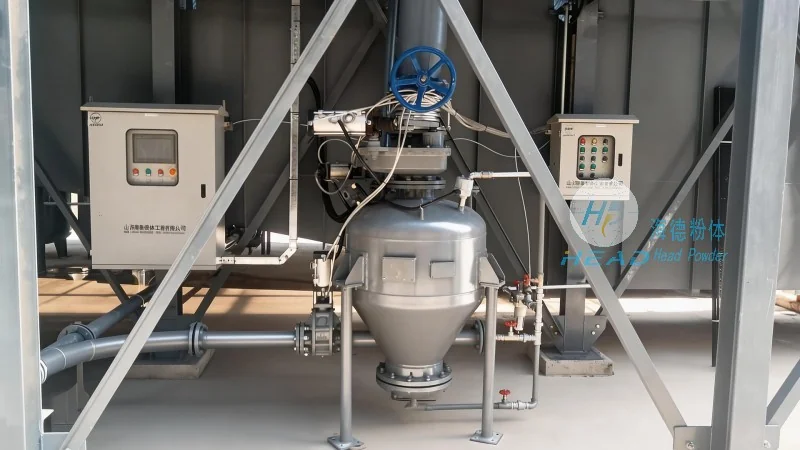
Company Profile and Professional Support
HeadPowder, a leading provider of engineering solutions, specializes in designing and manufacturing nitrile rubber pneumatic conveying systems tailored to the needs of various industries. With a focus on quality and innovation, the company's products are engineered to meet stringent industry standards and deliver reliable performance. HeadPowder's team of experienced engineers and technicians ensures that each system is customized to the client's specific requirements, including material handling capacity, pipeline layout, and operational environment. The company's headquarters is located in Shandong, China, where it leverages advanced manufacturing facilities and rigorous quality control processes to deliver superior products and comprehensive after-sales support.




