The dust removal coke powder pneumatic conveying system is a specialized industrial equipment designed for the efficient and safe transportation of coke powder, which is often generated during the coking process in steel and chemical industries. This system is engineered to handle the unique challenges associated with coke powder, such as its fine particle size, potential dust explosion risks, and the need for thorough dust removal to comply with environmental regulations.
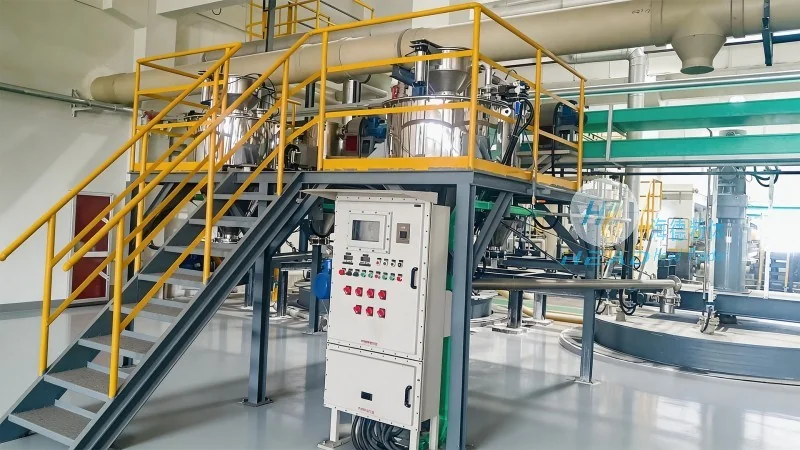
The core function of the system is to transport coke powder from the production site to storage or processing facilities while minimizing dust emissions and ensuring operational safety. It achieves this through a combination of air flow management, filtration systems, and specialized conveying components that are tailored to the physical properties of coke powder.
Structural Components and Working Principles
Next, we delve into the structural components and working principles of the system. The system typically consists of several key parts: a dust removal unit, a conveying pipeline, a blower or air compressor, and a control system. The dust removal unit is crucial as it captures and filters the fine coke powder particles from the air stream, preventing them from being released into the environment. This unit often includes cyclone separators, bag filters, or electrostatic precipitators, depending on the specific requirements and the dust concentration levels.
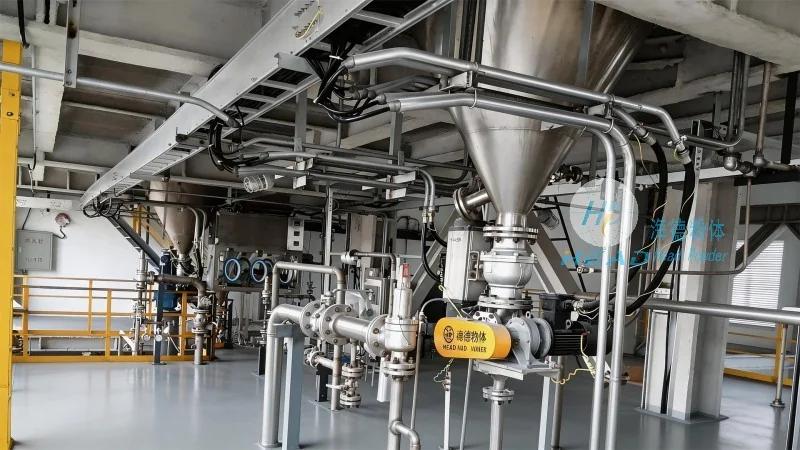
The conveying pipeline is designed to withstand the abrasive nature of coke powder and the pressure differentials created by the air flow. It is usually made of corrosion-resistant materials like stainless steel or special alloys to ensure long-term durability and prevent material degradation. The pipeline layout is carefully planned to minimize pressure losses and ensure smooth flow, with appropriate bends and fittings that are optimized for the powder's characteristics.
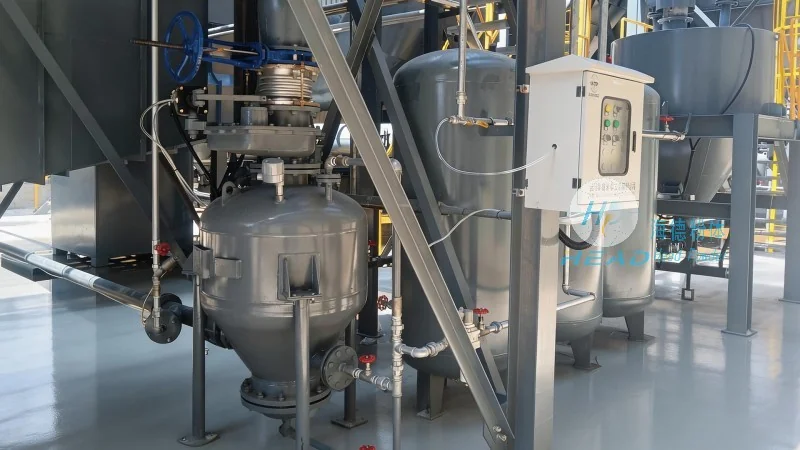
The blower or air compressor provides the necessary air pressure to move the coke powder through the pipeline. It is selected based on the required flow rate, pressure, and the specific properties of the powder, such as its density and moisture content. The control system monitors and regulates the air flow, pressure, and dust removal efficiency, ensuring the system operates within safe and optimal parameters.
In terms of the working principle, the system operates by creating a negative pressure or positive pressure environment within the pipeline. In a negative pressure system, the blower draws air and coke powder from the source, while the dust removal unit filters the air before it is released. In a positive pressure system, the blower pushes air and powder through the pipeline, with the dust removal unit capturing particles at the source or along the pipeline. Both systems are designed to maintain a consistent flow and prevent blockages, which can occur due to the cohesive nature of coke powder.
Advantages of Integrated Dust Removal and Conveying
The integration of dust removal and conveying in a single system is a key feature that sets this equipment apart from traditional methods. By combining these functions, the system not only transports the powder efficiently but also ensures compliance with environmental standards and enhances workplace safety. This approach reduces the need for separate dust collection and handling equipment, simplifying the overall process and lowering operational costs.
Customization and Scalability
The design of the dust removal coke powder pneumatic conveying system is highly customizable to meet the specific needs of different industrial applications. Factors such as the volume of coke powder to be transported, the distance between the source and destination, and the existing infrastructure are considered during the design phase. The system can be scaled from small-scale units for laboratory or pilot plants to large-scale systems for full production lines, making it versatile for various industrial settings.
Conclusion
In summary, the dust removal coke powder pneumatic conveying system is a sophisticated piece of equipment that addresses the challenges of handling coke powder while ensuring environmental compliance and operational safety. Its integrated design, robust construction, and efficient operation make it an essential component in modern industrial processes, particularly in the steel and chemical industries where coke powder is a byproduct of the coking process.
About HeadPowder: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, as the name suggests, is a professional engineering company specializing in the design, manufacturing, and installation of industrial conveying systems. With a strong presence in Shandong, China, HeadPowder has established itself as a reliable partner for businesses in the steel, chemical, and related industries. The company's expertise lies in developing customized solutions that meet the unique demands of each client, ensuring optimal performance and long-term reliability of the equipment.




