For industries dealing with bulk materials such as aggregates and powders, efficient and reliable material handling is crucial. The aggregate powder conveying system equipment, provided by Shandong HeadPowder Engineering Co., Ltd., is designed to meet these demands with advanced technology and robust construction. This equipment plays a vital role in ensuring smooth material flow from storage to processing or packaging stages, enhancing overall operational efficiency.
Company Overview
HeadPowder, as the brand under Shandong HeadPowder Engineering Co., Ltd., specializes in engineering solutions for material handling systems. With a focus on innovation and customer-centric design, the company has established itself as a trusted provider in the industry. Headquartered in Shandong, China, HeadPowder leverages local manufacturing expertise and global standards to deliver high-quality conveying equipment tailored to diverse industrial needs.
Key Components and Working Principle
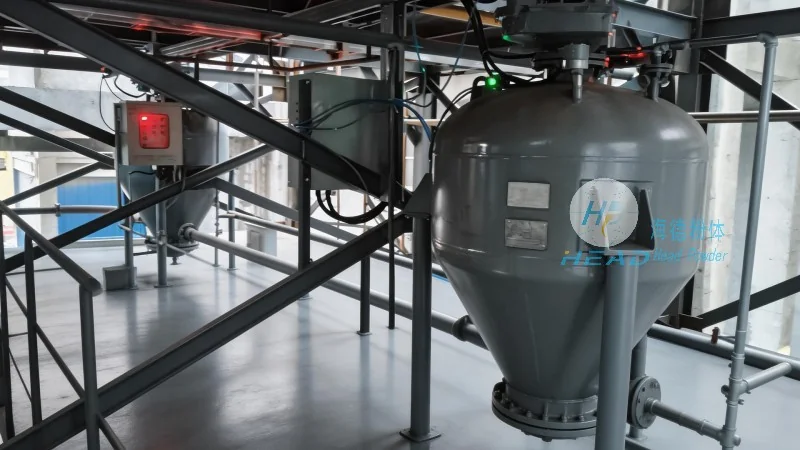
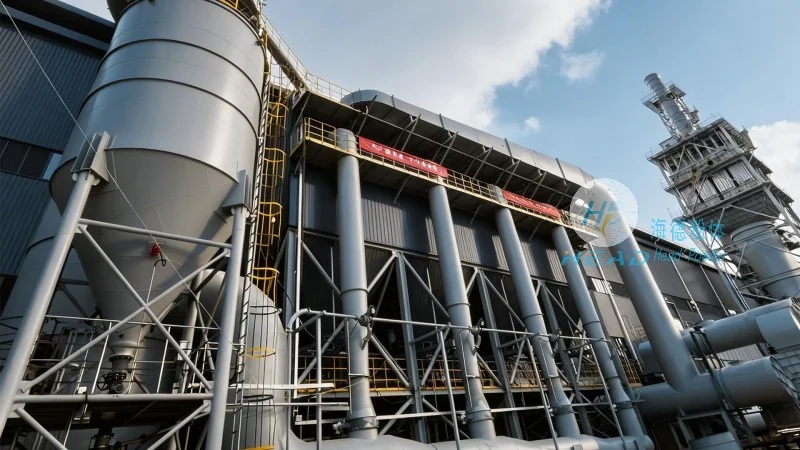
The aggregate powder conveying system equipment typically consists of several core components that work in tandem to achieve efficient material transport. The primary components include a hopper for material storage, a conveyor mechanism (such as screw conveyors, pneumatic systems, or belt conveyors), and control systems for regulating flow and speed. The working principle revolves around the movement of material through these components, utilizing mechanical or pneumatic forces to ensure consistent and controlled delivery.
Operation Process: Step-by-Step Overview
The operation process of the aggregate powder conveying system equipment begins with material loading into the hopper. Once the hopper is filled, the conveyor system activates, transporting the material through the system. The speed and direction of the conveyor are controlled by the integrated system to maintain optimal flow rates. At the discharge end, the material is collected and directed to the next stage of processing or storage. This process is designed to minimize downtime and maximize throughput, ensuring that material handling operations run smoothly and efficiently.
Advantages and Applications
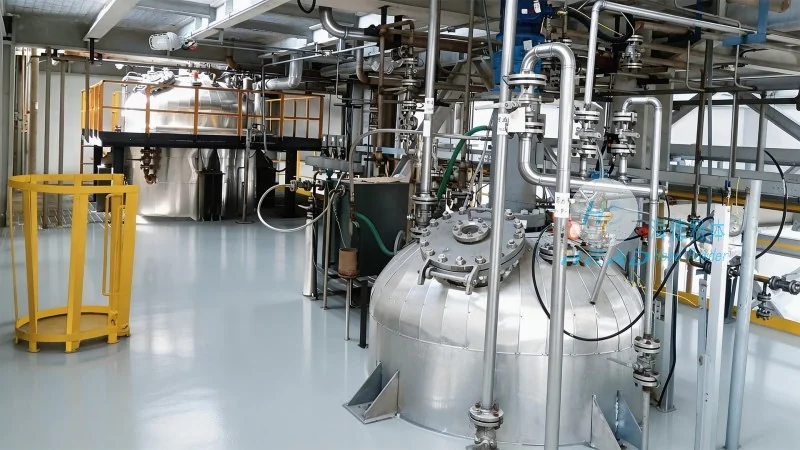
The aggregate powder conveying system equipment offers several advantages, including high capacity, low maintenance requirements, and adaptability to various material types. It is widely used in industries such as construction, mining, food processing, and chemical manufacturing, where the handling of bulk materials is essential. The system's ability to handle different particle sizes and moisture content makes it suitable for a broad range of applications, from transporting sand and gravel to processing powders like cement or flour.




