HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced powder handling solutions. The mixed positive and negative pressure powder conveying system is a sophisticated piece of equipment designed to efficiently transport bulk powders over long distances with precision and reliability. This system integrates both positive and negative pressure technologies to achieve optimal performance in various industrial applications.
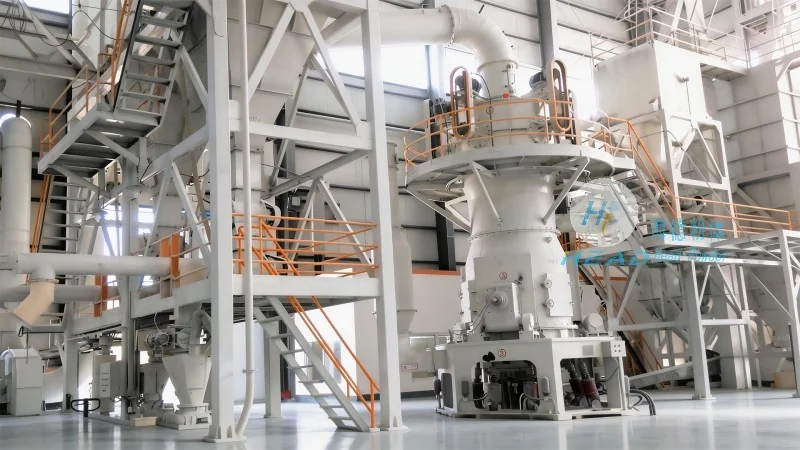
Working Principle of the Mixed Positive and Negative Pressure Powder Conveying System
The core of the mixed positive and negative pressure powder conveying system lies in its dual-pressure mechanism. Positive pressure is used to create an air flow that draws the powder from the source, while negative pressure is applied at the discharge end to ensure the powder is discharged smoothly. This combination allows for a balanced and controlled flow of powder, minimizing particle degradation and ensuring consistent material handling. The system typically consists of a series of components including a positive pressure blower, a negative pressure vacuum unit, a conveying pipe network, and control valves. The positive pressure blower generates an air stream that carries the powder particles through the pipeline, while the negative pressure unit at the discharge end creates a vacuum that pulls the powder out of the pipe and into the receiving container. The integration of these two pressure systems enables the equipment to handle a wide range of powder types, from fine powders to bulk materials, with minimal pressure loss and high efficiency.
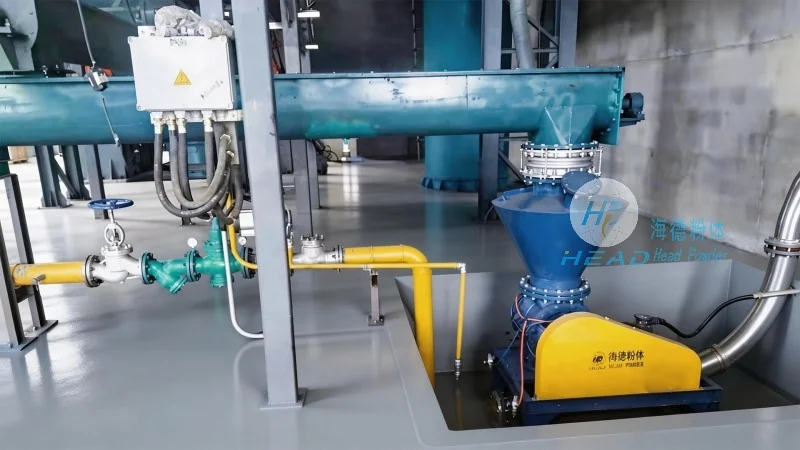
Operation Process of the Mixed Positive and Negative Pressure Powder Conveying System
The operation process of the mixed positive and negative pressure powder conveying system begins with the preparation phase. Before starting, the system is checked for proper air supply, pressure settings, and the condition of all components. The source container is positioned, and the receiving container is prepared. The control panel is then activated, and the system is set to the desired operating parameters. The positive pressure blower is started first, creating an air flow that draws the powder from the source into the conveying pipe. Simultaneously, the negative pressure unit at the discharge end is activated to create a vacuum that pulls the powder out of the pipe and into the receiving container. The system operates continuously as long as the source container has material and the receiving container has capacity. During operation, the pressure and flow rates are monitored to ensure optimal performance. If any issues arise, such as blockages or pressure fluctuations, the system has built-in safety features that automatically shut down or adjust parameters to prevent damage. The shutdown process involves first stopping the negative pressure unit, then the positive pressure blower, and finally closing all valves to prevent backflow. The system is then ready for maintenance or the next batch of material handling.
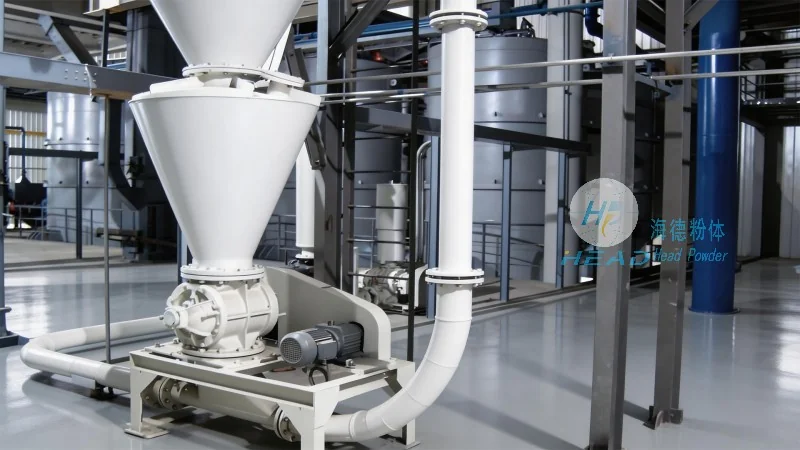
Key Features and Advantages of the Mixed Positive and Negative Pressure Powder Conveying System
The mixed positive and negative pressure powder conveying system offers several key features that make it an ideal choice for industrial powder handling. One of the primary advantages is its ability to handle a wide variety of powder types, including fine, cohesive, and abrasive powders, without causing particle degradation or segregation. The dual-pressure mechanism ensures a consistent and controlled flow, reducing the risk of blockages and improving overall system efficiency. Another advantage is the system's ability to operate over long distances, making it suitable for applications where the source and receiving points are far apart. The equipment is also designed for easy maintenance, with accessible components and clear operational indicators. Additionally, the system is energy-efficient, as it optimizes air usage and minimizes pressure loss, leading to lower operational costs. The integration of positive and negative pressure technologies also allows for flexible operation, as the system can be adjusted to handle different powder loads and flow rates.
Applications and Industries Served by the Mixed Positive and Negative Pressure Powder Conveying System
The mixed positive and negative pressure powder conveying system is widely used in various industries that require efficient and reliable powder handling. These industries include pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical industry, the system is used to transport raw materials and finished products with high precision, ensuring compliance with regulatory standards. In food processing, the system handles ingredients like flour, sugar, and spices, maintaining product quality and hygiene. In chemical manufacturing, the system transports bulk chemicals and powders, reducing the risk of contamination and improving safety. In mining, the system is used to transport ore and other materials from the source to processing facilities. The system's ability to handle different powder types and operate over long distances makes it suitable for a wide range of applications in these industries.
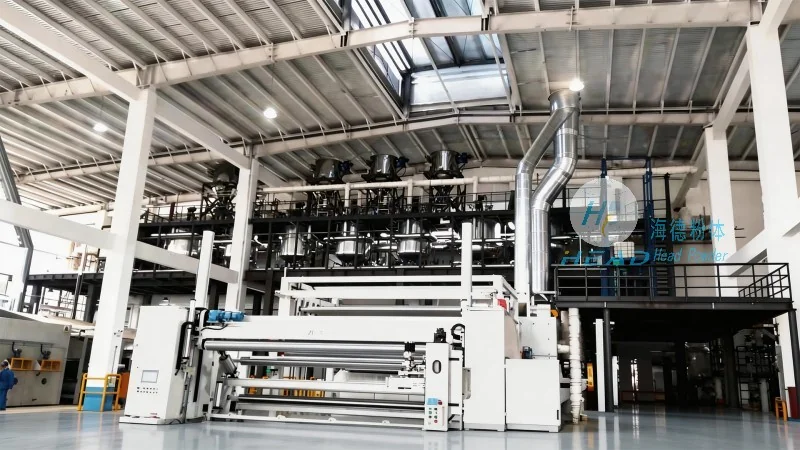
Conclusion and Company Information
HeadPowder, based in Shandong, China, is a trusted provider of advanced powder handling solutions. The mixed positive and negative pressure powder conveying system is a testament to the company's commitment to innovation and quality. With its efficient operation, reliable performance, and ability to handle a wide range of powder types, the system is an essential tool for industries that require precise and consistent powder handling. HeadPowder's expertise in designing and manufacturing such systems ensures that clients receive equipment that meets their specific needs and operational requirements. The company's focus on customer satisfaction and technical support makes it a preferred choice for businesses seeking reliable powder handling solutions.




