HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for handling rare earth crystal powders. This article delves into the fundamental principles of such systems and highlights the key characteristics of their operational environments, providing a comprehensive overview for industry professionals and potential clients.
Understanding the Core Principle of Rare Earth Crystal Powder Pneumatic Conveying
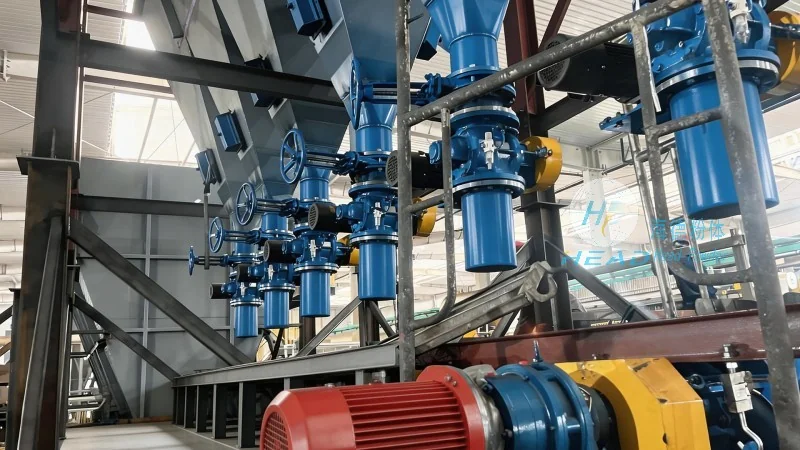
The pneumatic conveying line for rare earth crystal powders operates on the principle of transporting bulk materials through a pipeline using a gas stream, typically air or a combination of air and other gases. This method eliminates the need for mechanical components like belts, buckets, or screws, offering a more efficient and flexible solution for handling fine, abrasive, or valuable powders such as rare earth crystals. The system typically consists of a feeding device, a conveying pipeline, a control system, and a discharge unit. The feeding device, often a rotary valve or a feeder with a controlled flow rate, introduces the powder into the pipeline. The gas stream, generated by a blower or a compressor, then propels the powder particles through the pipeline to the discharge point. The control system ensures the proper flow of gas and material, maintaining consistent pressure and flow rates to prevent blockages or material degradation. The discharge unit, which may include a filter or a cyclone separator, collects the powder at the end of the pipeline, separating it from the gas stream for safe and efficient collection.
Key Working Scene Characteristics of the Pneumatic Conveying System
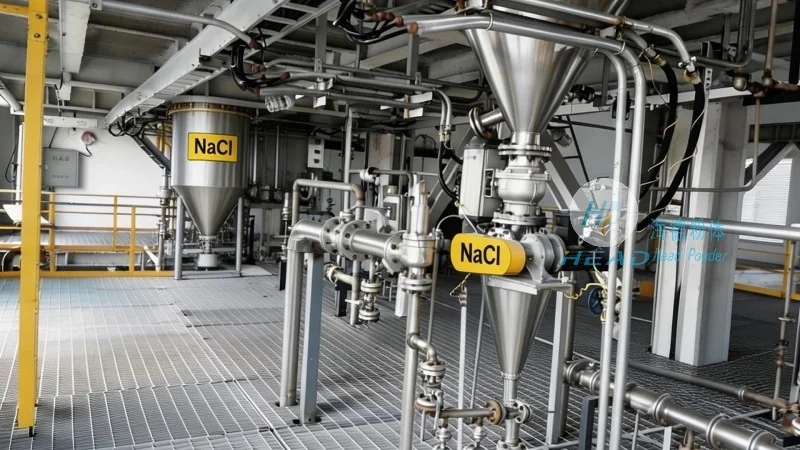
The operational environment of a rare earth crystal powder pneumatic conveying line is characterized by several critical factors that influence its performance and efficiency. Firstly, the material properties of rare earth crystals, such as their fine particle size, high density, and potential for static charge accumulation, require specialized equipment to prevent clogging and ensure smooth flow. The system must be designed with materials that are resistant to corrosion and wear, as rare earth powders can be abrasive and may cause damage to standard metal components over time. Secondly, the working scene often involves strict environmental and safety regulations due to the value and potential hazards of rare earth materials. The system must incorporate features like dust collection and filtration to minimize airborne particle emissions and protect both the environment and personnel. Thirdly, the flexibility of the system is a key characteristic, as rare earth processing facilities may require the conveyance of materials over varying distances and to multiple destinations. The modular design of pneumatic conveying lines allows for easy expansion or reconfiguration, adapting to changing production needs without significant downtime or capital investment. Additionally, the system's ability to handle materials in a closed pipeline reduces the risk of contamination and exposure to external elements, maintaining the purity of the rare earth crystals throughout the conveying process.
Application Scenarios and Operational Efficiency
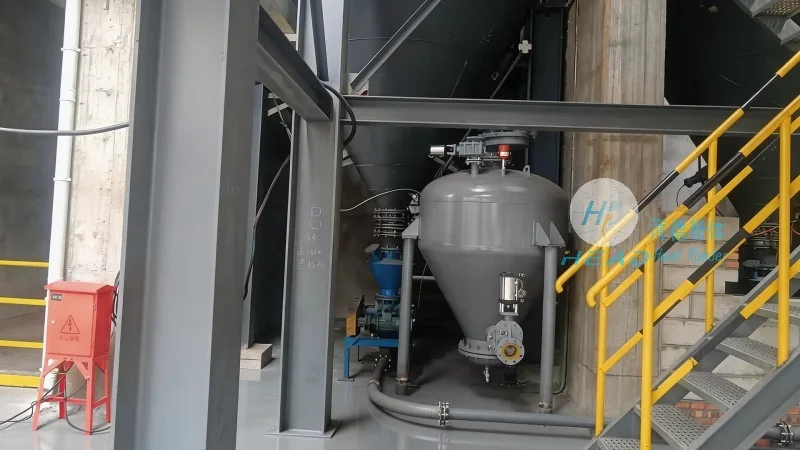
HeadPowder's pneumatic conveying systems for rare earth crystal powders are widely applied in various industrial settings, including rare earth mining and processing plants, material recovery facilities, and research laboratories. In mining operations, the system efficiently transports raw rare earth ores from extraction sites to processing plants, ensuring a continuous supply of material for subsequent grinding and separation. In processing plants, the system is used to convey fine rare earth powders between different stages of production, such as from grinding mills to magnetic separation units or from storage silos to packaging lines. The closed-loop design of the system minimizes material loss and contamination, which is crucial for maintaining the high purity standards required in rare earth applications. Furthermore, the system's ability to handle materials at high speeds and over long distances enhances operational efficiency, reducing the time and labor required for material transport compared to traditional methods like manual handling or mechanical conveyors. The consistent flow and controlled pressure provided by the pneumatic system also help in maintaining stable production processes, minimizing downtime and improving overall productivity.
Conclusion and Company Overview
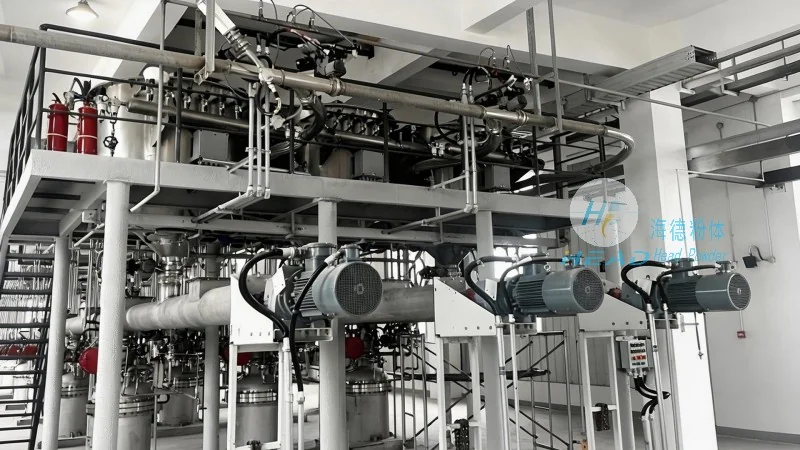
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted partner in the development and implementation of advanced pneumatic conveying solutions for rare earth crystal powder applications. With a focus on innovation and customer satisfaction, the company designs systems tailored to the specific needs of each client, ensuring optimal performance and reliability. The principles and characteristics of rare earth crystal powder pneumatic conveying lines, as outlined above, highlight the importance of specialized equipment and careful system design in handling these valuable materials. By leveraging the expertise of HeadPowder, industries can enhance their material handling processes, improve operational efficiency, and maintain the high standards required for rare earth crystal applications.




