Automatic bulk bag opening and powder pneumatic conveying machines represent a critical technology in modern industrial material handling, particularly for the efficient and safe transfer of bulk powders. These systems are designed to streamline the process of handling large quantities of powder materials, from initial unloading from bulk bags to final delivery to processing equipment. The integration of automated bag opening mechanisms with pneumatic conveying technology ensures high operational efficiency and minimal human intervention, making them indispensable in various industrial sectors.
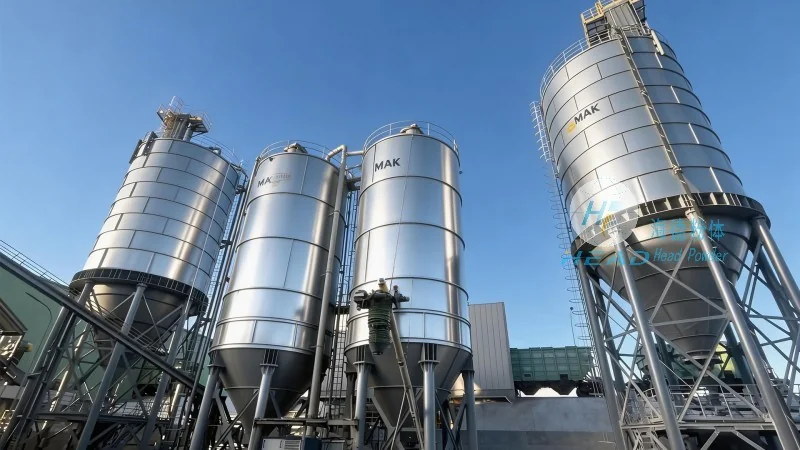
Introduction to Automatic Bulk Bag Opening and Powder Pneumatic Conveying Systems
At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design, manufacturing, and implementation of advanced bulk bag handling solutions. Our systems are engineered to meet the stringent requirements of industries such as chemical, food, pharmaceutical, and agricultural, where the handling of powders demands precision, safety, and reliability. The core functionality of these machines revolves around two main components: the automatic bulk bag opening system and the pneumatic conveying system, both of which work in tandem to ensure seamless material transfer.
Principle of Pneumatic Conveying Technology
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials through a pipeline using air as the conveying medium. The technology can be categorized into two main types: positive pressure (or pressure) systems and negative pressure (or vacuum) systems. In a positive pressure system, air is forced through the pipeline at a pressure higher than the ambient air, pushing the powder forward. Conversely, a negative pressure system creates a vacuum in the pipeline, drawing the powder into the system. The choice between these systems depends on factors such as the material's properties, the distance to be conveyed, and the required flow rate. The automatic bulk bag opening machine typically uses a combination of mechanical and pneumatic components to release the powder from the bag into the conveying line, ensuring a controlled and dust-free transfer.
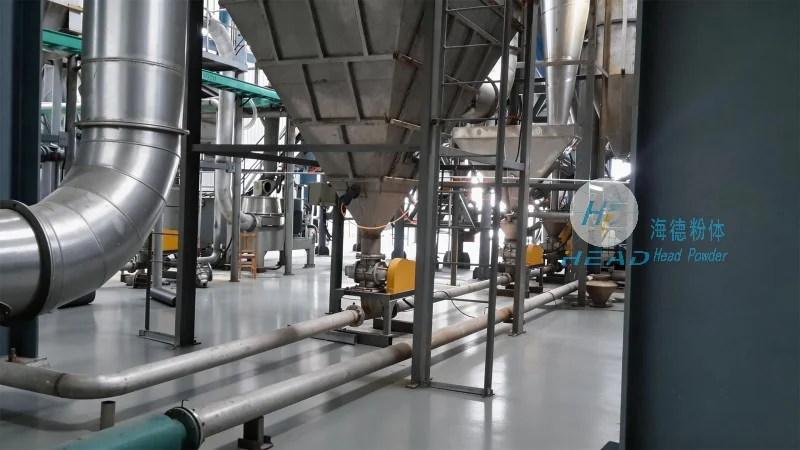
Automatic Bulk Bag Opening Mechanism
The automatic bulk bag opening mechanism is a sophisticated system that eliminates the need for manual intervention during the unloading process. It typically includes a series of components such as a lifting frame, a bag clamp, and pneumatic valves. The process begins with the placement of the bulk bag onto the machine's frame. The lifting mechanism raises the bag to the appropriate height, while the clamp secures the bag's top opening. Pneumatic actuators then activate to release the bag's inner liner or open the top seal, allowing the powder to flow into the hopper. This mechanism is designed to be safe and efficient, with features like dust collection and air filtration to maintain a clean working environment. The automation of this step significantly reduces labor costs and minimizes the risk of dust exposure and material contamination.
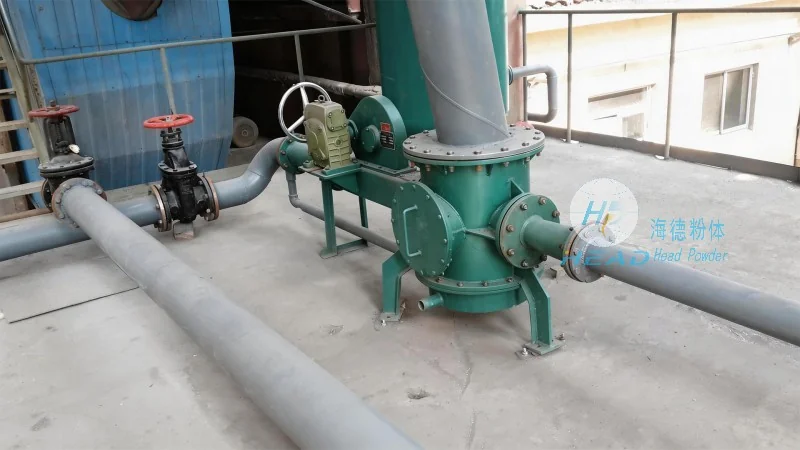
Key Working Scene Characteristics
The working scene characteristics of these machines are tailored to the specific needs of different industrial applications. In the chemical industry, for example, the system must handle a wide range of powders, from fine chemicals to bulk raw materials, while maintaining strict safety protocols due to the potential hazards of certain substances. In the food and beverage sector, the equipment must comply with stringent hygiene standards, ensuring that the powder handling process is clean and free from contaminants. The pharmaceutical industry, particularly in the context of GMP (Good Manufacturing Practice) compliance, requires the highest level of precision and cleanliness, with the system designed to prevent cross-contamination and maintain product integrity. Each of these sectors presents unique challenges, and the design of the automatic bulk bag opening and pneumatic conveying machine is customized to address these challenges effectively.
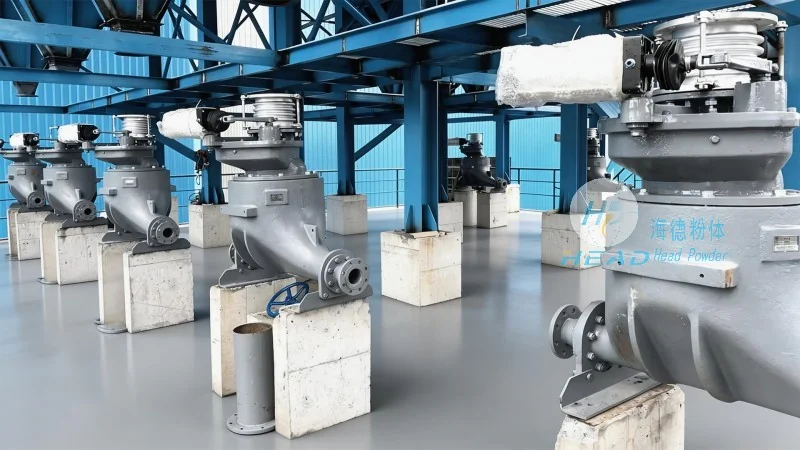
Application Scenarios in Industrial Settings
In industrial settings, the automatic bulk bag opening and powder pneumatic conveying machine is widely used in various processes. For instance, in a chemical plant, the system may be used to transport raw materials such as limestone or sulfur to the production reactors. In a food processing facility, it could handle ingredients like flour or sugar, ensuring a consistent supply to the production line. The pharmaceutical industry utilizes these systems for the handling of active pharmaceutical ingredients (APIs) and excipients, where the purity and consistency of the powder are critical. Agricultural applications may involve the transfer of fertilizers or animal feed, where the system's ability to handle bulk quantities efficiently is essential. The versatility of the system allows it to adapt to different production scales and material types, making it a valuable asset in modern manufacturing environments.
Advantages in Practical Operations
The implementation of automatic bulk bag opening and powder pneumatic conveying systems offers several advantages in practical operations. Firstly, the automation of the unloading process reduces labor costs and minimizes the risk of human error, leading to increased operational efficiency. Secondly, the system provides a dust-free and controlled environment, which is crucial for maintaining product quality and safety standards. Thirdly, the pneumatic conveying technology allows for the transport of powders over long distances without the need for complex mechanical components, such as conveyor belts or elevators. This not only reduces maintenance costs but also enhances the flexibility of the production layout. Additionally, the system's ability to handle a wide range of powder materials makes it a versatile solution for diverse industrial needs. Overall, the combination of automated bag opening and pneumatic conveying technology provides a reliable and efficient method for bulk powder handling, contributing to improved productivity and reduced operational risks.




