HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced powder handling solutions, including specialized pneumatic conveying systems for sodium hexafluorophosphate. This article explores the fundamental principles behind such equipment and highlights the key working scene characteristics that define its operational effectiveness in industrial settings.
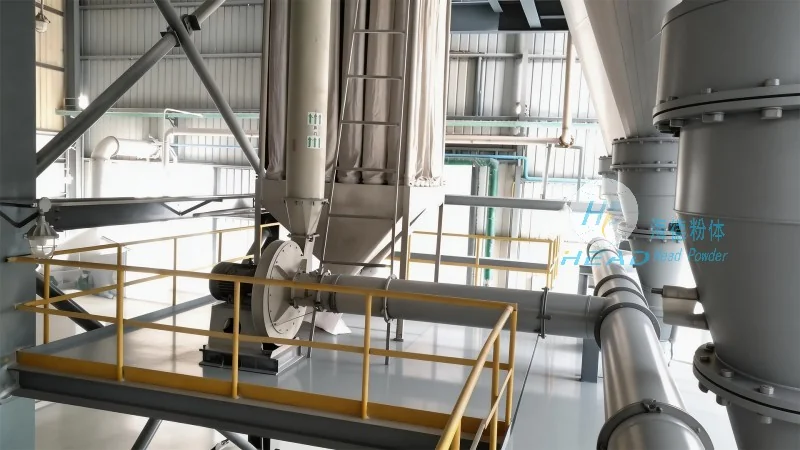
Introduction to Sodium Hexafluorophosphate Pneumatic Conveying Systems
Sodium hexafluorophosphate (NaPF₆) is a critical chemical compound widely used in various industries, including pharmaceuticals, electronics, and chemical manufacturing. Efficient and reliable transport of this fine powder is essential to maintain product quality and operational efficiency. Pneumatic conveying systems offer a non-contact, low-damage method for moving such powders, making them an ideal choice for handling sodium hexafluorophosphate. These systems utilize compressed air or other gases to transport the powder through a pipeline, ensuring minimal product degradation and contamination.
The Core Principle of Pneumatic Conveying for Sodium Hexafluorophosphate
The fundamental principle of pneumatic conveying involves creating a flow of air or gas that propels the powder particles through a duct. This process can be categorized into two main types: dilute phase and dense phase. In dilute phase conveying, the powder is suspended in the air stream, allowing for high-velocity transport over longer distances. Dense phase conveying, on the other hand, involves a slower, more controlled flow where the powder is carried in a slurry-like state, reducing the risk of particle degradation and ensuring precise delivery. For sodium hexafluorophosphate, the choice between these methods depends on the specific application requirements, such as the distance to be covered and the need for product integrity.
Key Working Scene Characteristics of the Equipment
The operational characteristics of sodium hexafluorophosphate powder pneumatic conveying equipment are tailored to meet the demands of diverse industrial environments. These characteristics include:
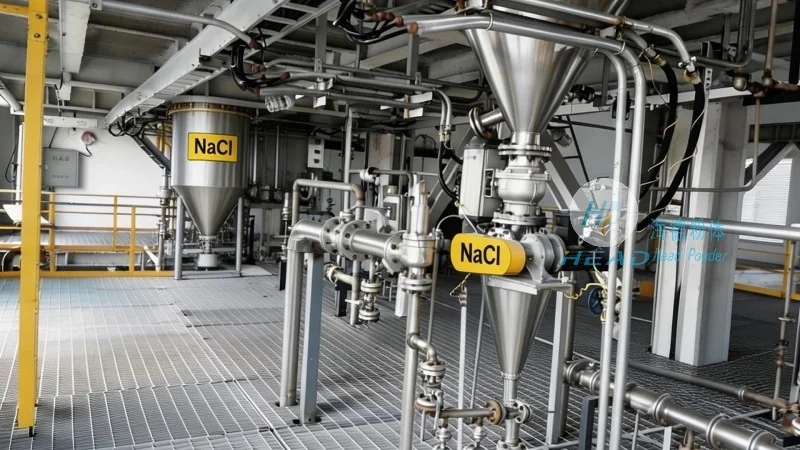
1. Low Product Contamination: The non-contact nature of pneumatic conveying minimizes the risk of contamination from external sources, which is crucial for pharmaceutical and electronic applications where product purity is paramount.
2. Efficient Material Handling: The system can handle high volumes of powder with minimal downtime, enhancing overall production throughput. This is particularly beneficial in continuous manufacturing processes where consistent material flow is essential.
3. Space Efficiency: Pneumatic conveying systems are compact and can be installed in tight spaces, making them suitable for facilities with limited floor area. This is advantageous in urban industrial settings where space is at a premium.
4. Versatility in Application: The equipment can be adapted to various working scenarios, including vertical and horizontal transport, as well as transfer between different processing units. This flexibility allows for integration into existing production lines without major modifications.
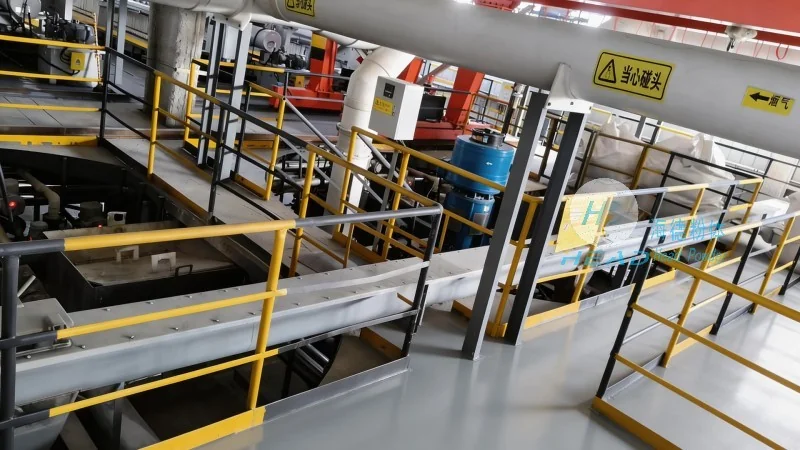
Industrial Applications and Operational Scenarios
Sodium hexafluorophosphate is utilized in a range of industrial processes, and the pneumatic conveying equipment is designed to support these applications effectively. For instance, in pharmaceutical manufacturing, the system ensures the safe and hygienic transfer of raw materials to production lines, maintaining compliance with regulatory standards. In chemical synthesis, the equipment facilitates the precise delivery of sodium hexafluorophosphate to reactors, optimizing reaction efficiency and reducing waste. Additionally, in the electronics industry, the system helps transport the powder for use in cleaning and etching processes, where particle size and purity are critical.
Advantages in Specific Working Environments
The working scene characteristics of the pneumatic conveying system make it particularly effective in environments where traditional mechanical conveying methods may be unsuitable. For example, in dusty or hazardous areas, the enclosed system prevents the release of powder particles into the air, enhancing workplace safety. Moreover, the system's ability to handle fine powders without clogging or blockages is beneficial in applications where the powder has a tendency to agglomerate. This ensures consistent performance and reduces maintenance requirements, contributing to long-term operational reliability.
Conclusion
HeadPowder's sodium hexafluorophosphate powder pneumatic conveying equipment exemplifies advanced powder handling technology, combining efficiency, reliability, and adaptability. By understanding the core principles and working scene characteristics, industries can leverage this equipment to enhance their production processes, ensure product quality, and maintain operational excellence. With its roots in Shandong, China, HeadPowder continues to innovate and provide tailored solutions that meet the evolving needs of modern industrial applications.




