HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling systems tailored for industrial applications. This article delves into the operational principles and distinctive working scene characteristics of the sodium nitrate material handling system equipment, highlighting its efficiency and adaptability in various industrial settings.
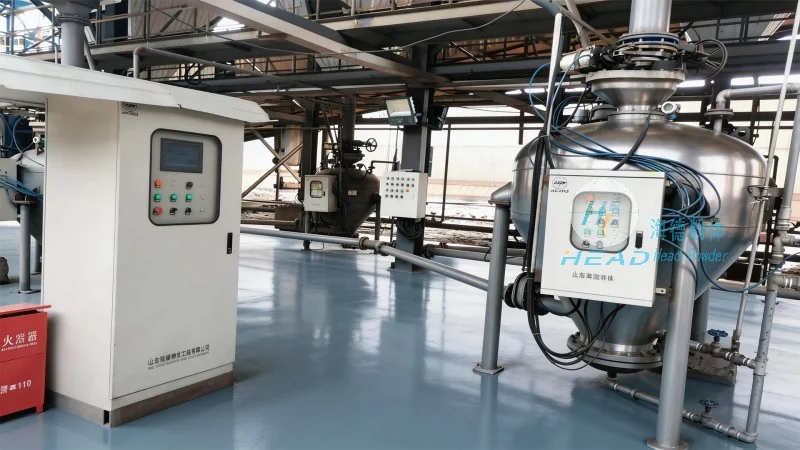
Overview of Sodium Nitrate Material Handling Systems
Sodium nitrate, a critical industrial chemical used in fertilizer production, food preservation, and other sectors, requires specialized handling equipment to ensure safety and operational efficiency. The material handling system for sodium nitrate typically integrates multiple components, including storage silos, conveyors, feeding mechanisms, and control systems, all designed to manage the bulk material from storage to processing or packaging. HeadPowder’s expertise lies in optimizing these systems to meet the unique demands of sodium nitrate handling, ensuring compliance with safety standards and maximizing throughput.
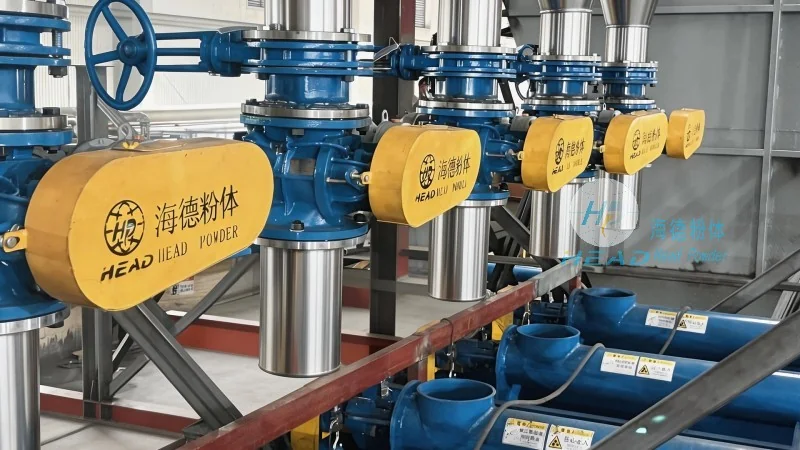
Core Operational Principles
The fundamental principle of the sodium nitrate material handling system is to maintain a continuous and controlled flow of the material while minimizing the risk of dust generation and ensuring proper containment. The system operates through a series of interconnected processes: first, the material is stored in a sealed silo to prevent moisture absorption and contamination. Then, an automated feeding mechanism, often equipped with a rotary valve or screw feeder, regulates the discharge of sodium nitrate into the conveyor system. The conveyor, which may be a belt conveyor or a pneumatic conveyor depending on the application, transports the material to the next processing stage. Advanced control systems monitor the flow rate, pressure, and temperature to maintain optimal conditions and prevent system failures.
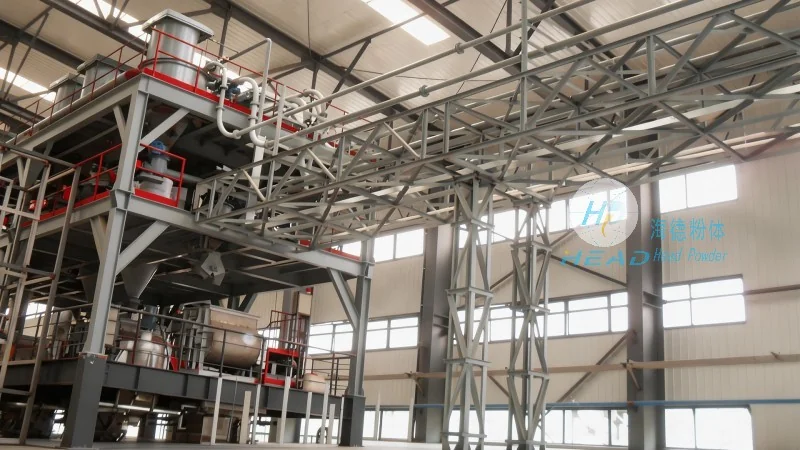
Working Scene Characteristics
The working scene characteristics of the sodium nitrate material handling system are tailored to the specific requirements of industrial environments where sodium nitrate is processed. These systems are designed for high-volume operations, often handling large quantities of material per hour, and are built to withstand the corrosive and abrasive nature of sodium nitrate. Key characteristics include:
- High Efficiency and Throughput: The system is engineered to handle high volumes of sodium nitrate, ensuring smooth and continuous operation with minimal downtime. This is crucial for industrial plants that rely on consistent material supply for production.
- Safety and Containment: Given the potential hazards associated with sodium nitrate, such as dust explosion risks and environmental contamination, the system incorporates robust containment measures. Sealed silos, dust collection systems, and explosion-proof components are standard features to ensure worker safety and environmental compliance.
- Adaptability to Industrial Settings: The material handling system can be customized to fit various industrial layouts, whether in a fertilizer plant, chemical processing facility, or food processing plant. HeadPowder’s engineering team works closely with clients to design systems that integrate seamlessly with existing infrastructure, minimizing installation time and costs.
- Maintenance and Durability: The equipment is constructed from corrosion-resistant materials, such as stainless steel, to withstand the chemical properties of sodium nitrate. Regular maintenance schedules and easy access to components ensure long-term reliability and reduce operational costs.
Application Scenarios
The sodium nitrate material handling system is widely used in several industrial applications, including:
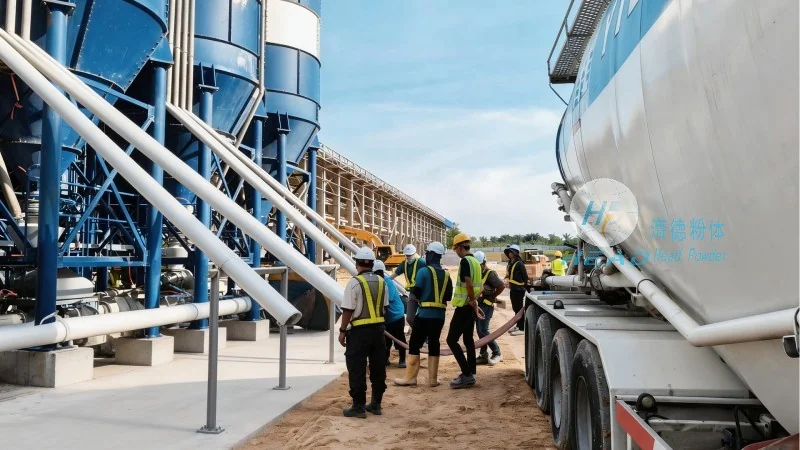
- Fertilizer Production: In fertilizer manufacturing, sodium nitrate is a key ingredient in nitrogen-based fertilizers. The material handling system ensures a steady supply of sodium nitrate to the production line, supporting high-yield and efficient fertilizer production.
- Food Industry: In food processing, sodium nitrate is used as a preservative and color enhancer in meat products. The system’s ability to handle the material hygienically and safely is critical for maintaining food quality and compliance with food safety regulations.
- Chemical Processing: Beyond agriculture and food, sodium nitrate is used in the production of other chemicals, such as nitric acid and explosives. The material handling system’s robust design and safety features make it suitable for these high-risk applications.
Conclusion
HeadPowder’s sodium nitrate material handling system equipment exemplifies advanced engineering and industrial design, combining efficiency, safety, and adaptability to meet the diverse needs of modern industrial operations. By leveraging years of experience in material handling solutions, HeadPowder ensures that clients receive systems that not only optimize material flow but also enhance overall operational performance and safety in sodium nitrate processing environments.




