HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced carbon material conveying systems. These systems are engineered to efficiently handle various carbon-based materials, including powders, granules, and other bulk materials, ensuring smooth and reliable material transport in industrial applications. The core of these systems lies in their sophisticated design, which integrates multiple components to achieve optimal performance under diverse operational conditions.
Principles of Carbon Material Conveying Systems
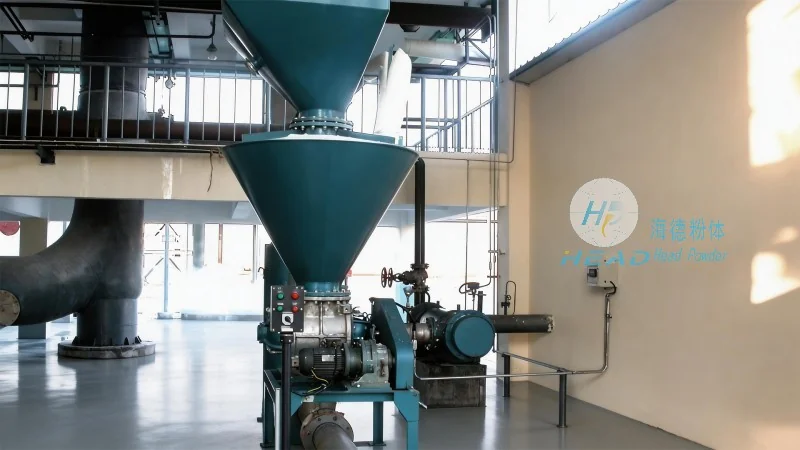
The fundamental principle of carbon material conveying systems revolves around the use of mechanical or pneumatic mechanisms to transport bulk materials from one location to another. These systems typically consist of a feeding unit, a conveying mechanism (such as a screw conveyor, pneumatic conveyor, or belt conveyor), and a discharge unit. The feeding unit ensures uniform material input, while the conveying mechanism provides the necessary force to move the material through the system. Pneumatic conveying systems, for instance, utilize compressed air to create a flow of material through a pipeline, which is particularly effective for transporting fine powders without generating dust or causing material degradation. Mechanical conveying systems, like screw conveyors, rely on rotating screws to push material forward, offering high efficiency for bulkier materials. The selection of the appropriate conveying mechanism depends on factors such as material properties, particle size, and the required conveying distance, ensuring that the system operates at peak efficiency.
Key Working Scene Characteristics
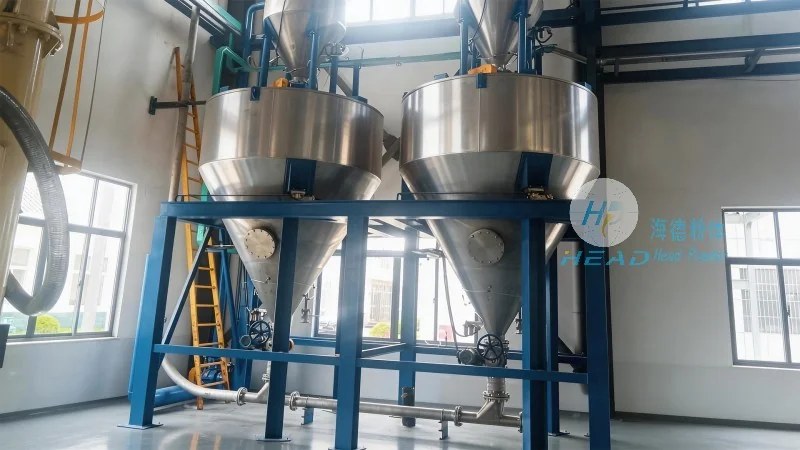
The working scene characteristics of carbon material conveying systems are tailored to meet the specific demands of industrial environments. In manufacturing facilities, these systems are commonly used in carbon black production, graphite processing, and battery material handling, where the need for precise material control and minimal contamination is critical. The systems are designed to operate in harsh conditions, with robust construction to withstand high temperatures, corrosive substances, and heavy loads. For example, in battery material processing, the conveying system must maintain strict particle size distribution and prevent moisture ingress, which could affect the quality of the final product. In carbon black production, the system must handle fine powders that are prone to agglomeration, requiring specialized feeding and conveying mechanisms to ensure consistent flow. Additionally, the systems are often integrated with automation controls, allowing for real-time monitoring and adjustment of operational parameters to optimize performance and reduce downtime.
Application Examples and Operational Efficiency
Real-world applications of carbon material conveying systems demonstrate their versatility and effectiveness in various industrial settings. In a carbon black manufacturing plant, the conveying system efficiently transports raw carbon materials from storage silos to processing units, ensuring a continuous supply of material for production. The system’s ability to handle high volumes of fine powders without clogging or loss of material is crucial for maintaining production rates. Similarly, in a graphite processing facility, the conveying system transports graphite flakes and powders to different stages of the production line, including grinding, classification, and packaging. The system’s design allows for gentle handling of the material, preserving its structural integrity and preventing damage that could affect the final product’s quality. Operational efficiency is enhanced through features such as variable speed controls, which adjust the conveying rate based on material flow, and automatic shut-off mechanisms that prevent overloading or system failure. These features contribute to reduced maintenance costs and increased overall productivity in industrial operations.
Conclusion and Company Overview
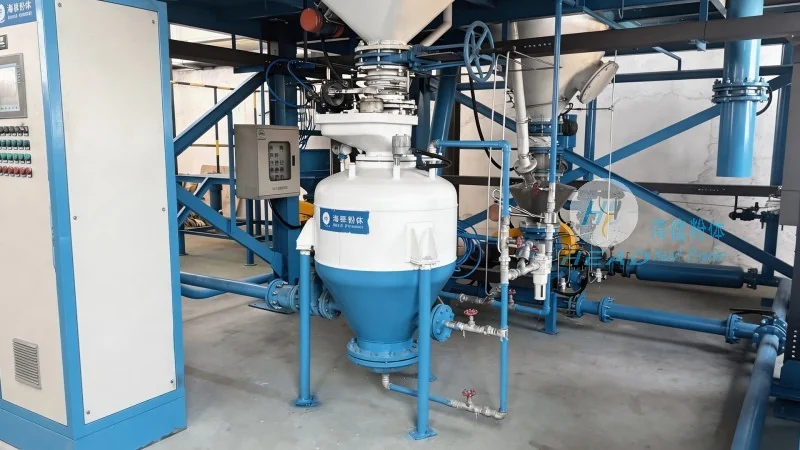
Carbon material conveying systems, as developed by Shandong HeadPowder Engineering Co., Ltd., represent a sophisticated solution for the efficient handling of carbon-based materials in industrial applications. By integrating advanced engineering principles and robust construction, these systems ensure reliable performance, minimal material loss, and optimal operational efficiency. The company’s commitment to innovation and customer-centric design has made its conveying systems a preferred choice in industries such as battery manufacturing, carbon black production, and graphite processing. With a strong presence in Shandong, China, HeadPowder continues to provide high-quality solutions tailored to the evolving needs of industrial clients, ensuring that material transport processes remain efficient, safe, and cost-effective.




