HeadPowder, a leading enterprise in the field of powder conveying technology, specializes in providing advanced solutions for the transportation of desulfurization and denitrification agents. This article delves into the core principles and operational characteristics of the powder conveying systems designed for these critical industrial applications.
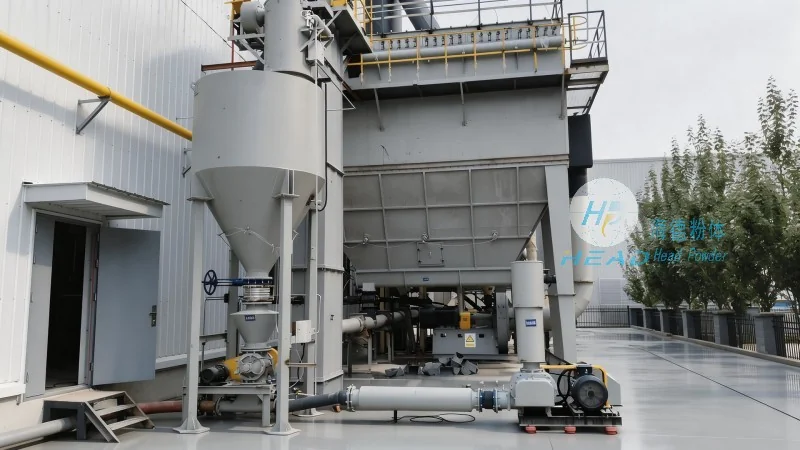
Company Overview
Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is dedicated to developing and manufacturing high-efficiency powder handling equipment. With years of experience and a commitment to innovation, HeadPowder has established itself as a trusted partner for industries requiring reliable and efficient powder transportation solutions. The company's focus on precision engineering and customer-centric design ensures that their systems meet the stringent demands of modern industrial processes.
Principle of Powder Conveying Systems
The desulfurization and denitrification agent powder conveying system operates on the principle of pneumatic or mechanical transport, depending on the specific requirements of the application. For bulk powder handling, pneumatic conveying is commonly employed, utilizing air pressure to move the material through pipelines. This method offers advantages such as low maintenance, minimal product contamination, and the ability to handle a wide range of particle sizes and moisture contents. Mechanical conveying systems, on the other hand, rely on positive displacement or screw mechanisms to transport powders, providing consistent flow rates and suitable for applications where air quality or product purity is a concern.
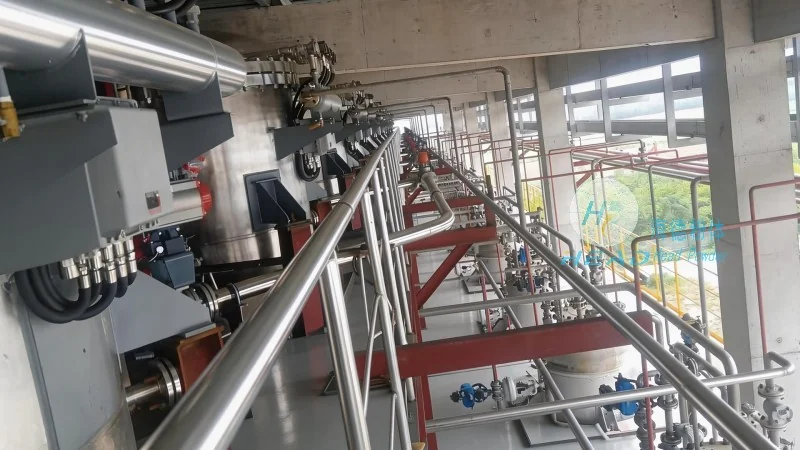
Working Scene Characteristics
The working scene characteristics of these systems are tailored to the specific needs of desulfurization and denitrification processes, which are integral to reducing air pollution from industrial emissions. The systems are designed to handle powders with varying properties, including high moisture content, corrosive nature, or abrasive characteristics. In industrial settings, these systems are typically integrated into larger production lines, ensuring seamless material transfer from storage silos to reaction units or treatment equipment. The operational efficiency of the system is critical, as it directly impacts the overall performance of the desulfurization and denitrification processes. Key characteristics include high conveying capacity, low energy consumption, and the ability to maintain consistent flow rates under varying load conditions. Additionally, the systems are engineered to minimize product degradation and ensure compliance with environmental regulations, making them essential components in modern pollution control technologies.
Key Features and Benefits
HeadPowder's powder conveying systems for desulfurization and denitrification agents are equipped with several key features that enhance their performance and reliability. These include advanced control systems that allow for real-time monitoring and adjustment of conveying parameters, ensuring optimal operation. The systems are also designed with robust materials to withstand the corrosive and abrasive nature of the powders being handled. Another significant benefit is the reduction in labor costs and operational downtime, as the automated nature of the systems minimizes the need for manual intervention. Furthermore, the compact design of the equipment allows for easy integration into existing industrial facilities, without requiring extensive modifications to the plant layout.
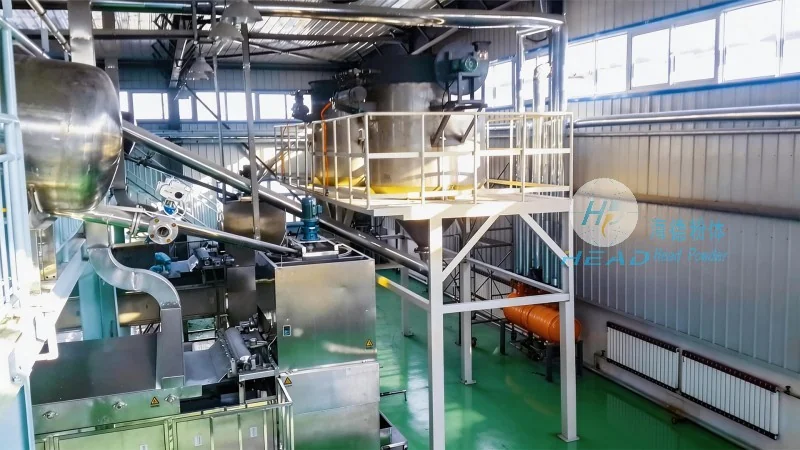
Application in Industrial Processes
The desulfurization and denitrification agent powder conveying systems are widely used in power plants, chemical manufacturing facilities, and other industrial sectors where air pollution control is a priority. In power plants, these systems are crucial for transporting limestone or other sorbents to the flue gas desulfurization (FGD) units, where they react with sulfur dioxide to form calcium sulfite or calcium sulfate. Similarly, in denitrification processes, the systems deliver ammonia or urea-based reagents to the selective catalytic reduction (SCR) units, facilitating the conversion of nitrogen oxides into harmless nitrogen gas. The reliability and efficiency of the powder conveying systems directly contribute to the effectiveness of these pollution control measures, helping industries meet stringent environmental standards while maintaining operational productivity.
Conclusion
HeadPowder's desulfurization and denitrification agent powder conveying systems represent a sophisticated solution for the efficient handling of critical industrial powders. By combining advanced engineering principles with practical application insights, these systems ensure reliable performance in demanding industrial environments. As industries continue to prioritize environmental sustainability and operational efficiency, the role of such specialized powder conveying equipment becomes increasingly vital. Shandong HeadPowder Engineering Co., Ltd. remains at the forefront of this technology, providing innovative solutions that meet the evolving needs of modern industrial applications.




