Principle and Working Scene Characteristics of Sodium Nitrate Powder Conveyors
Release time:2026-09-19 06:01:30
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Sodium nitrate, a vital chemical raw material utilized across diverse industrial sectors, demands efficient and reliable conveying systems to ensure seamless material handling. The sodium nitrate powder conveying equipment developed by Shandong HeadPowder Engineering Co., Ltd. (referred to as HeadPowder) is specifically engineered to address the unique challenges associated with transporting this substance. This article will explore the working principles of these conveyors and highlight their key characteristics in various operational scenarios.
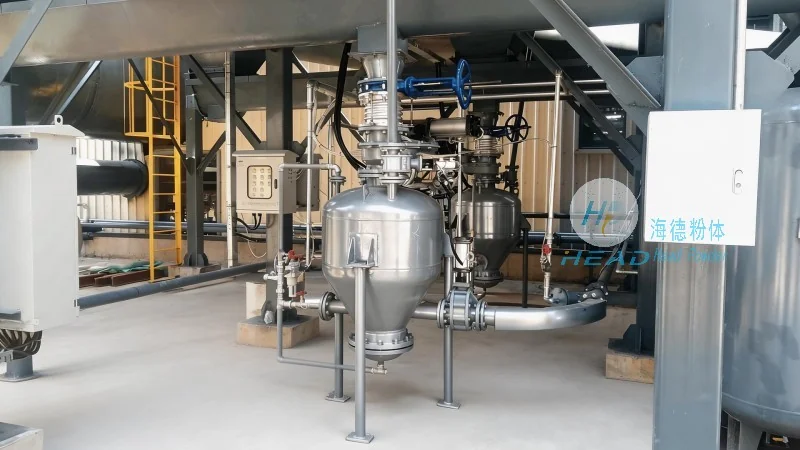
The Principle of Sodium Nitrate Powder Conveyors
The fundamental principle of sodium nitrate powder conveyors centers on the efficient transfer of bulk powder materials from one location to another. HeadPowder's equipment typically leverages advanced technologies such as pneumatic conveying, screw conveyors, or bucket elevators, tailored to the physical properties of sodium nitrate. For instance, pneumatic conveying systems utilize air pressure to move the powder through pipelines, which is particularly effective for handling fine powders like sodium nitrate that are prone to caking or bridging. The design of these conveyors accounts for factors like the material's flowability, moisture content, and potential for dust generation, ensuring safe and efficient operation. The mechanical components—including feeders, hoppers, and discharge mechanisms—are engineered to minimize material degradation and maintain consistent flow rates. By integrating these principles, HeadPowder's conveyors provide a reliable solution for sodium nitrate transportation in industrial settings.
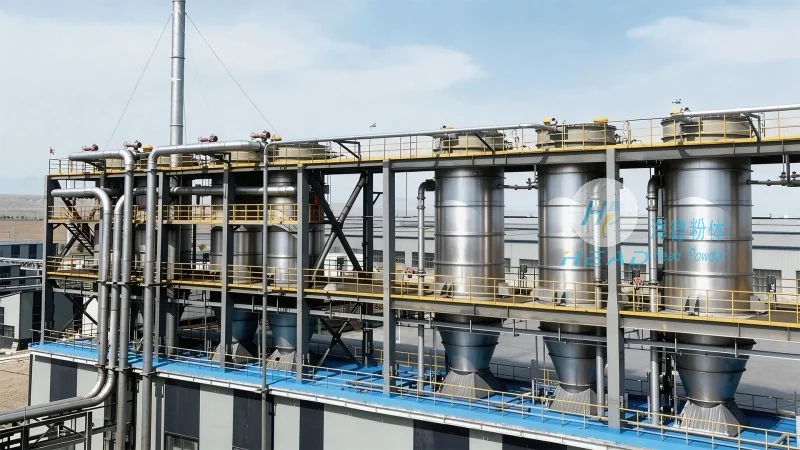
Working Scene Characteristics of Sodium Nitrate Powder Conveyors
The application scenarios of sodium nitrate powder conveyors vary across different industries, each presenting distinct requirements that the equipment must meet. In chemical manufacturing plants, these conveyors are essential for transferring sodium nitrate from storage silos to processing units, ensuring a continuous supply of raw material. The equipment is designed to handle high volumes with minimal downtime, which is crucial for maintaining production efficiency. In warehousing and logistics operations, the conveyors facilitate the movement of sodium nitrate between storage areas and loading docks, optimizing inventory management and reducing handling time. The working scene characteristics also include considerations for environmental safety, as sodium nitrate is a potentially hazardous material. The conveyors are equipped with dust collection systems and explosion-proof features to mitigate risks and comply with safety regulations. Additionally, the design allows for easy integration with existing production lines, enabling seamless operation without significant modifications to the facility. The versatility of HeadPowder's conveyors makes them suitable for a wide range of applications, from small-scale laboratory use to large-scale industrial production.
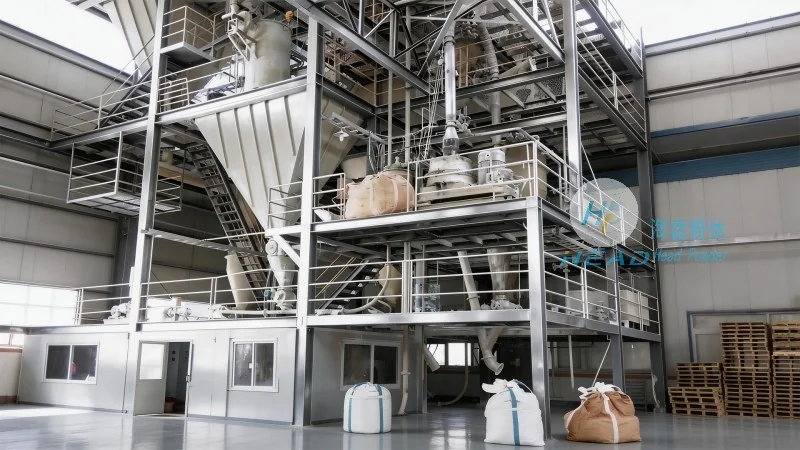
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of powder handling equipment, has established itself as a trusted partner in the chemical industry. With its headquarters in Shandong, China, the company specializes in developing customized solutions for bulk material transportation. The company's team of engineers and technicians brings extensive experience in designing and manufacturing conveyors for various challenging materials, including sodium nitrate. HeadPowder's commitment to quality and innovation is reflected in its state-of-the-art production facilities and rigorous testing processes. The company adheres to international standards and continuously invests in research and development to enhance the performance and reliability of its products. By combining technical expertise with a customer-centric approach, HeadPowder ensures that its sodium nitrate powder conveyors meet the specific needs of each client, delivering long-term value and operational efficiency. The company's presence in the market is a testament to its dedication to excellence and its role in supporting the growth of industries that rely on efficient material handling solutions.




