Coffee bean powder conveying is a critical process in the coffee production and processing industry, ensuring efficient and reliable movement of coffee powder from one stage to another. This article explores the fundamental principles behind coffee bean powder conveying systems and highlights the key operational characteristics that define their effectiveness in various industrial settings.
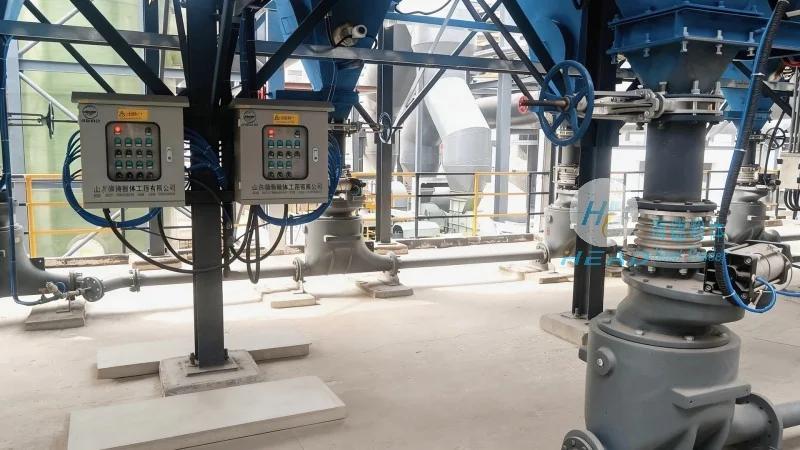
Understanding the Core Principles of Coffee Bean Powder Conveying
The primary goal of coffee bean powder conveying is to transport coffee powder—whether it's freshly ground coffee, instant coffee powder, or other coffee-derived products—between different equipment and storage areas without compromising product quality or integrity. The process relies on several key principles, including gravity, air pressure, and mechanical force, which are tailored to the specific properties of coffee powder, such as its density, moisture content, and flowability.
One of the most common methods is gravity-based conveying, where coffee powder is allowed to flow down chutes or hoppers due to gravity. This approach is ideal for short-distance transfers and when the powder has good flow characteristics. However, for longer distances or when dealing with powders that tend to clog or segregate, other methods like air-assisted conveying are employed. Air-assisted systems use a combination of air flow and mechanical components (like rotary valves or pneumatic actuators) to move the powder through pipelines, ensuring consistent and controlled transport.
Key Operational Characteristics of Coffee Bean Powder Conveying Systems
The effectiveness of coffee bean powder conveying systems is determined by several operational characteristics that must be optimized for each application. These include:
1. Flowability and Bulk Density: Coffee powder's ability to flow freely through conveying equipment is crucial. Factors like particle size distribution, moisture content, and the presence of clumps can significantly impact flowability. Systems are designed to maintain consistent bulk density to prevent bridging or segregation, which can lead to uneven product distribution.
2. Dust Control and Air Quality: Coffee powder is often fine and can generate significant dust during conveying. Effective dust control measures, such as sealed conveying lines, filtration systems, and proper ventilation, are essential to maintain air quality and prevent product contamination. This is particularly important in food processing environments where hygiene standards are strict.
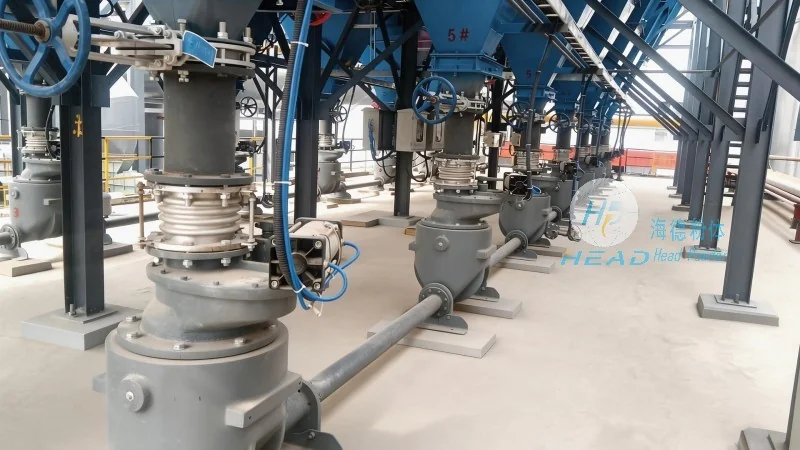
3. Energy Efficiency: The energy consumption of conveying systems is a critical operational characteristic. Modern systems, including those from companies like Shandong HeadPowder Engineering Co., Ltd. (headpowder), incorporate energy-efficient designs, such as variable speed drives and optimized air flow, to reduce operational costs while maintaining performance.
4. Scalability and Flexibility: Coffee processing facilities often require conveying systems that can adapt to varying production volumes and product types. Scalable systems that can be easily expanded or reconfigured are essential for meeting changing operational needs. This flexibility allows businesses to maintain efficiency during peak production periods and adjust to seasonal demand fluctuations.
Work Scenarios and Applications in Coffee Production
Coffee bean powder conveying systems are used in a wide range of work scenarios across the coffee supply chain. These include:
1. Post-Baking and Cooling: After coffee beans are roasted, they are often ground into powder and then cooled. Conveying systems transport the freshly ground coffee from the roasting and grinding equipment to cooling chambers or storage silos. This step is critical to prevent overheating and ensure the coffee retains its flavor and aroma.
2. Storage and Packaging: Once cooled, coffee powder is typically stored in large silos or bulk containers. Conveying systems move the powder from storage to packaging lines, where it is filled into bags, cans, or other containers. This ensures a smooth transition from storage to final product packaging, minimizing downtime and maximizing throughput.
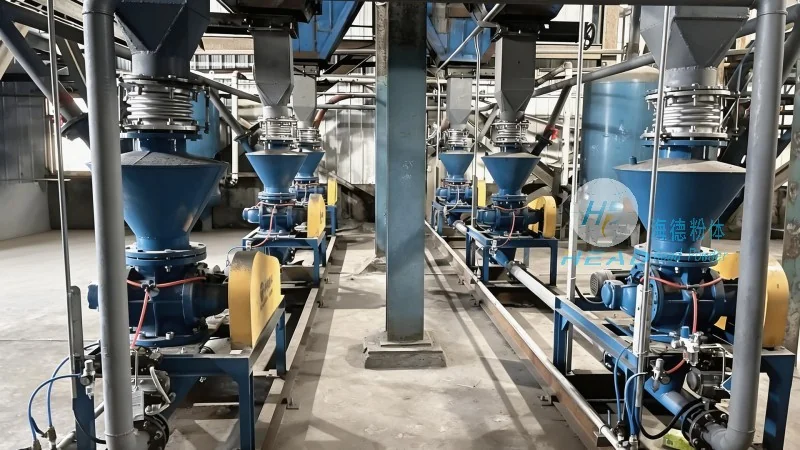
3. Industrial Processing: In larger coffee processing facilities, multiple stages of processing may require powder transport. For example, in the production of instant coffee, coffee powder is often mixed with other ingredients (like sugar or milk powder) and then conveyed to drying or blending equipment. The efficiency of the conveying system directly impacts the overall production speed and product quality.
4. Quality Control and Sampling: Conveying systems can also be integrated with quality control processes. For instance, sample ports can be installed along the conveying line to collect representative samples for testing. This allows for real-time monitoring of product consistency and helps maintain quality standards throughout the production process.
HeadPowder's Expertise in Coffee Bean Powder Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of specialized conveying solutions for the coffee industry. With a deep understanding of coffee powder properties and the unique challenges faced by coffee processing facilities, headpowder designs and manufactures systems tailored to meet the specific needs of each client.
Headpowder's expertise lies in integrating advanced technologies with practical, field-proven solutions. Their systems are engineered to optimize flowability, minimize dust generation, and enhance energy efficiency, ensuring that coffee powder is transported safely and efficiently. The company's commitment to quality and customer satisfaction has made it a trusted partner for coffee producers worldwide.
Headpowder's facilities are located in Shandong, China, where the company leverages local resources and expertise to deliver high-quality products and services. By focusing on the operational characteristics that matter most to coffee producers—such as reliability, durability, and cost-effectiveness—headpowder helps businesses streamline their operations and improve overall productivity.




