HeadPowder, a leading enterprise in the field of material handling technology, specializes in the design, manufacturing, and application of advanced pneumatic conveying systems for powdered ores. This article delves into the fundamental principles behind these systems and explores the key working scene characteristics that make them indispensable in modern industrial operations.
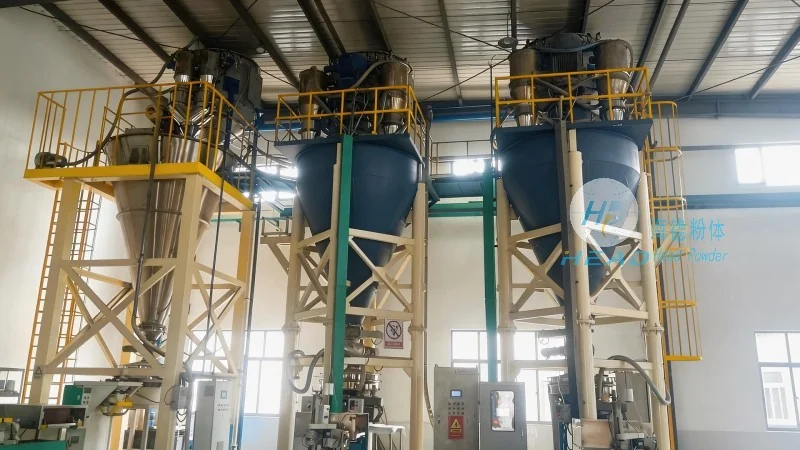
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials like powdered ores through a pipeline using compressed air or vacuum. The core principle involves creating a pressure differential to move the material. In positive pressure systems, a fan or blower generates high-pressure air that propels the ore particles through the pipeline. Conversely, negative pressure systems use a vacuum to draw the material into the pipeline. For powdered ores, which often have fine particles and varying moisture content, the choice of system depends on factors such as material properties, distance, and environmental requirements.
The working scene characteristics of powdered ore pneumatic conveying systems are tailored to meet the demands of specific industrial applications. In mining operations, these systems are crucial for transporting ore from extraction sites to processing facilities, ensuring efficient and dust-free material transfer. The high efficiency and flexibility of pneumatic conveyors make them ideal for handling ore with high moisture content or abrasive particles, which can damage traditional mechanical conveyors. Additionally, the ability to transport materials over long distances without the need for multiple transfer points reduces operational costs and improves safety by minimizing manual handling.
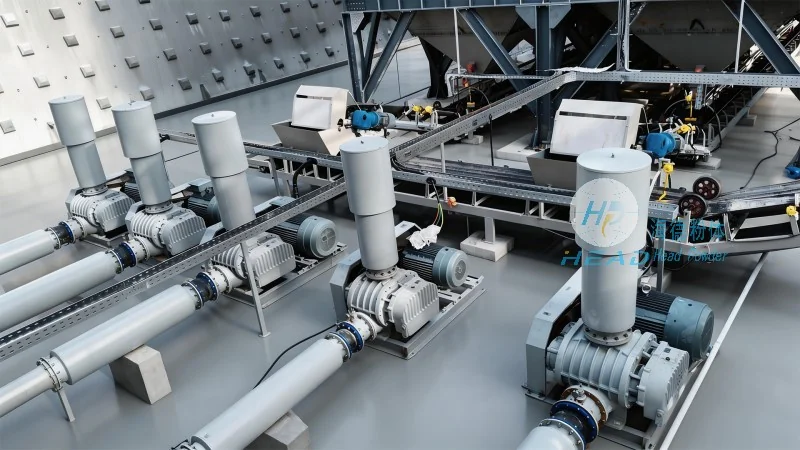
In the cement industry, pneumatic conveying is widely used to transport raw materials like limestone, clinker, and additives. The systems are designed to handle large volumes of material while maintaining consistent flow rates, which is critical for the quality control of cement production. The dust control features of these systems are particularly important in cement plants, as they help to comply with environmental regulations and protect equipment from corrosion. Furthermore, the modular design of pneumatic conveying systems allows for easy integration with existing production lines, making them a cost-effective solution for modern cement manufacturers.
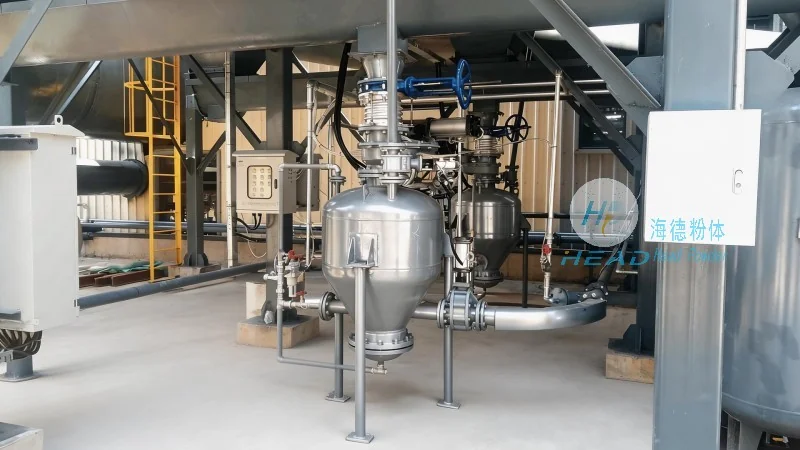
Chemical and pharmaceutical industries also benefit from the application of powdered ore pneumatic conveying systems. These sectors require precise control over material handling to ensure product purity and safety. The systems are often equipped with advanced control mechanisms that monitor pressure, flow rate, and particle size, allowing for real-time adjustments to maintain optimal performance. The hygienic design of these conveyors is essential in pharmaceutical applications, where contamination must be strictly avoided. By using pneumatic conveying, companies can achieve seamless material transfer while maintaining high standards of cleanliness and efficiency.
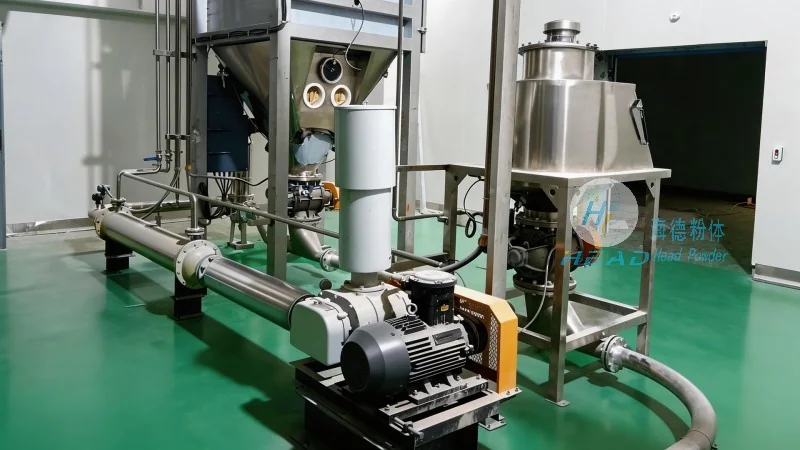
Another key aspect of the working scene characteristics is the adaptability of these systems to different ore types and particle sizes. Whether dealing with fine powders or coarse granules, the design of the conveying pipeline and the selection of the appropriate air velocity can be adjusted to ensure reliable transport. The use of flexible hoses or rigid pipes depends on the specific application, with flexible systems being preferred for applications requiring frequent changes in direction or layout. The durability of the components, such as the fan, pipeline, and valves, is also a critical factor in the working scene, as they must withstand the abrasive nature of powdered ores and the corrosive effects of certain chemicals.
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of customized pneumatic conveying solutions tailored to the unique needs of each client. With years of experience in the industry, the company has developed a deep understanding of the principles and applications of powdered ore pneumatic conveying systems. By combining advanced technology with expert engineering, HeadPowder delivers systems that are not only efficient and reliable but also cost-effective and environmentally friendly. The company's commitment to quality and customer satisfaction has made it a leading choice for businesses seeking to optimize their material handling processes.




