Ammonium nitrate with moisture is a common chemical material used in various industrial applications, and the efficient handling of such materials is crucial for ensuring safety and operational efficiency. The material handling system equipment designed for transporting this specific type of ammonium nitrate plays a vital role in modern industrial processes. This article will explore the working principle and key features of such systems, providing a comprehensive understanding for professionals in the field.
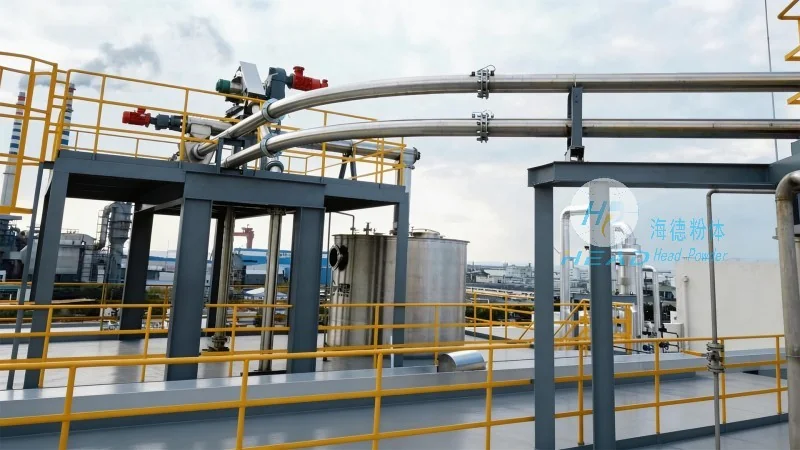
Overview of Ammonium Nitrate with Moisture Material Handling Systems
Ammonium nitrate with moisture refers to the form of this chemical where water is present, often as a result of processing or storage conditions. This moisture content can affect the material's flow characteristics and handling requirements. The material handling systems for this type of ammonium nitrate are engineered to address these specific challenges, ensuring safe and efficient transport from storage to processing or end-use applications. These systems are typically integrated into larger industrial setups, working in conjunction with other equipment to form a cohesive material flow management solution.
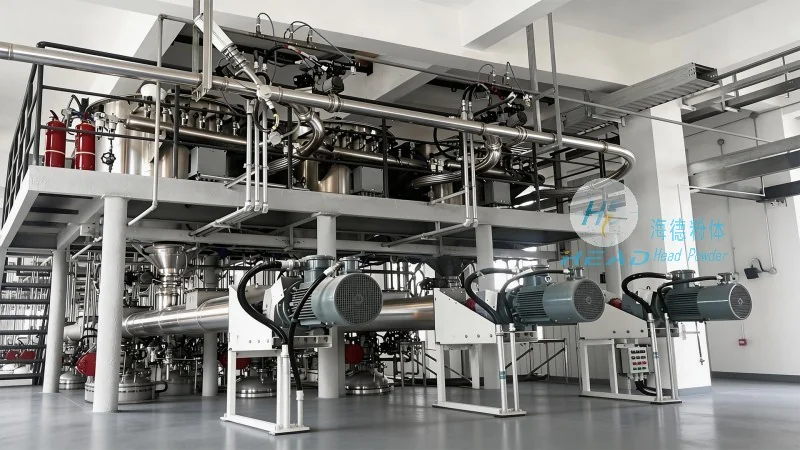
Working Principle of the Material Handling System
The core working principle of the ammonium nitrate with moisture material handling system revolves around the use of specialized equipment designed to handle bulk materials with moisture content. The system typically includes components such as feeders, conveyors, and storage silos, each playing a specific role in the material transport process. The feeders are responsible for uniformly distributing the material, while the conveyors transport it to the next stage of processing. The storage silos provide a controlled environment for storing the material before it is released for transport. The entire system operates based on a closed-loop mechanism, where sensors and control systems monitor the material flow and adjust operations as needed to maintain optimal performance. This closed-loop control ensures that the system can handle variations in moisture content and material flow rates without compromising safety or efficiency.
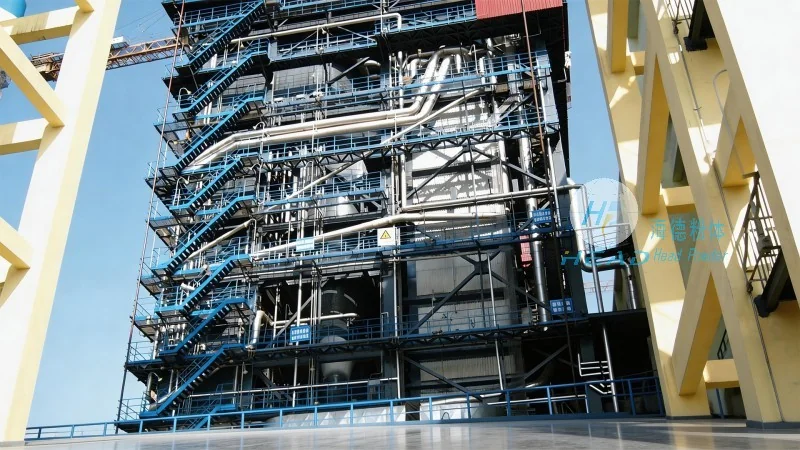
Key Features of the Material Handling Equipment
The material handling equipment for ammonium nitrate with moisture is characterized by several key features that enhance its performance and safety. One of the primary features is the use of specialized materials for construction, such as corrosion-resistant metals and coatings, to withstand the chemical properties of ammonium nitrate and the effects of moisture. The equipment is also designed with safety mechanisms, including overload protection and emergency stop functions, to prevent accidents and ensure the safety of operators. Another important feature is the integration of advanced control systems, which allow for precise monitoring and adjustment of the material flow. These systems can detect changes in moisture content or material density and adjust the operation of the feeders and conveyors accordingly. Additionally, the equipment is designed for easy maintenance and cleaning, which is essential for maintaining the quality of the material and preventing contamination. The features collectively contribute to the reliability and efficiency of the material handling system, making it a critical component in industrial operations involving ammonium nitrate with moisture.
Application and Benefits in Industrial Settings
The ammonium nitrate with moisture material handling system is widely used in various industrial sectors, including fertilizer production, chemical manufacturing, and mining. In fertilizer production, for example, the system is used to transport ammonium nitrate from storage to blending and packaging facilities. The benefits of using such a system include improved safety due to reduced manual handling, increased efficiency through automated material transport, and better control over the material's moisture content. These benefits contribute to higher productivity and lower operational costs for industrial facilities. The system's design also allows for scalability, enabling it to be adapted to different production volumes and requirements. This flexibility makes it suitable for a wide range of applications, from small-scale operations to large industrial plants.
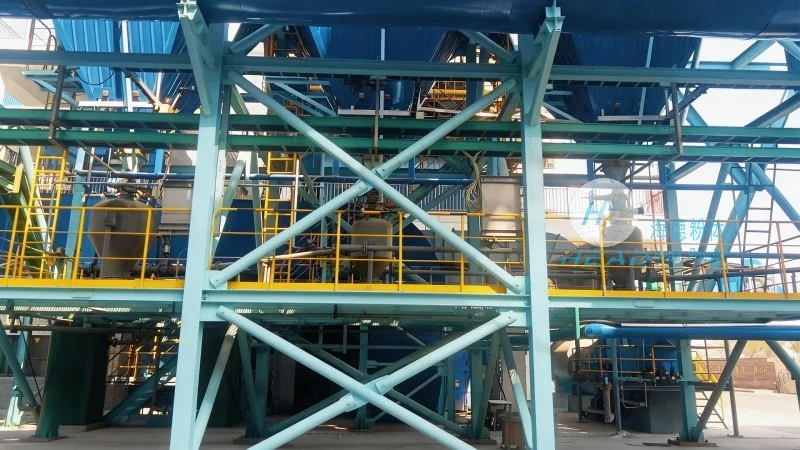
Conclusion and Company Information
In conclusion, the material handling system equipment for ammonium nitrate with moisture is a sophisticated solution designed to address the unique challenges of handling this chemical material. The working principle, which involves specialized equipment and closed-loop control, ensures efficient and safe transport. The key features, including corrosion-resistant construction, safety mechanisms, and advanced control systems, enhance the system's performance and reliability. The system's application in various industrial sectors highlights its importance in modern industrial operations. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such material handling systems, with a focus on meeting the specific needs of clients in the chemical and industrial sectors. Based in Shandong, China, the company leverages its expertise to deliver high-quality solutions that contribute to the safety and efficiency of industrial processes involving ammonium nitrate with moisture.




