Working Principle and Features of Small Bag Unpacking Material Conveying System Equipment
Release time:2026-09-17 23:01:22
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Small bag unpacking material conveying systems are essential in industrial settings where bulk materials are packaged in small bags and need to be efficiently transferred to processing or storage areas. These systems streamline material handling, reduce labor costs, and enhance overall operational efficiency. The following sections will explore the working principle and key features of such equipment, providing insights into how they operate and their benefits in industrial applications. Developed by Shandong HeadPowder Engineering Co., Ltd. (headpowder), these systems are engineered to meet the diverse needs of modern industrial operations.
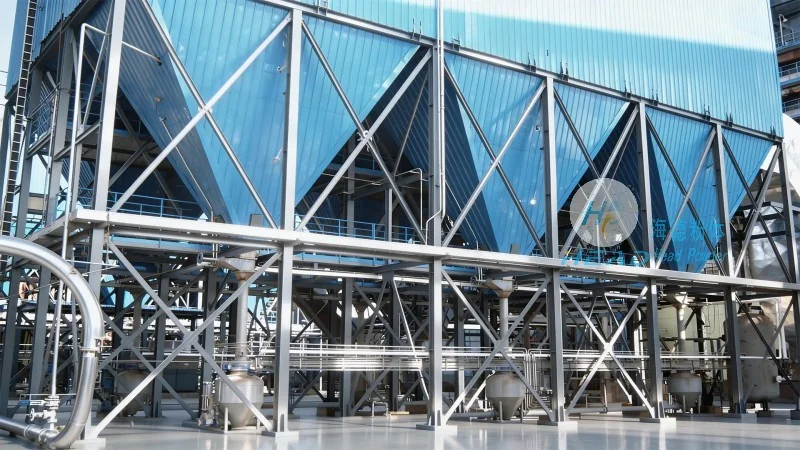
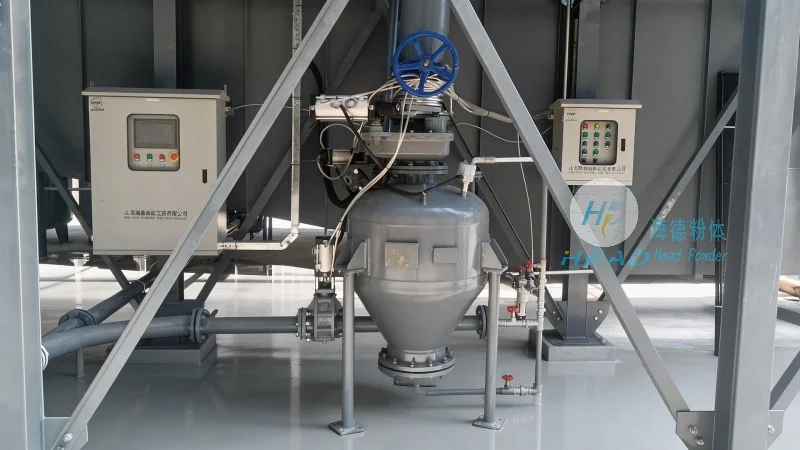
Working Principle of Small Bag Unpacking Material Conveying Systems
The working principle of a small bag unpacking material conveying system typically involves several integrated components working in sequence to handle the material from bag to conveyor. The process begins with the bag being placed on a feeding platform or hopper. A mechanical or pneumatic mechanism then opens the bag, allowing the contents to flow into a hopper or chute. From there, the material is transferred to a conveyor system, such as a belt conveyor or screw conveyor, which transports the material to the next stage of processing or storage. The system may also include features like bag emptying mechanisms, which can be designed to handle various bag sizes and materials, ensuring consistent performance.
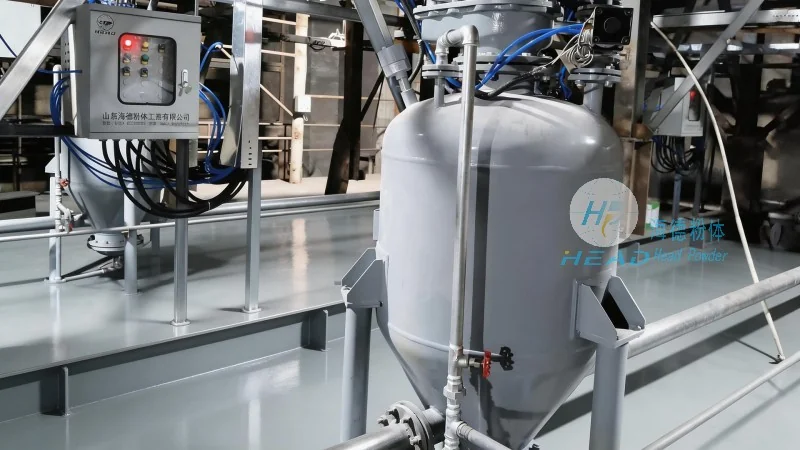
Key Features of Small Bag Unpacking Material Conveying Systems
Small bag unpacking material conveying systems are characterized by several key features that enhance their functionality and adaptability. One of the primary features is the bag opening mechanism, which can be designed to handle different bag types, including paper, plastic, or composite bags. This flexibility allows the system to accommodate a wide range of materials, from powders and granules to bulk solids. Another important feature is the material transfer mechanism, which may include a hopper or chute that efficiently directs the material from the bag to the conveyor. The conveyor system itself is often designed for high throughput and durability, with options for adjustable speed and load capacity to suit various production requirements. Additionally, many systems include safety features, such as emergency stop buttons and protective guards, to ensure operator safety during operation. The integration of these components results in a seamless material handling process that minimizes downtime and maximizes productivity.
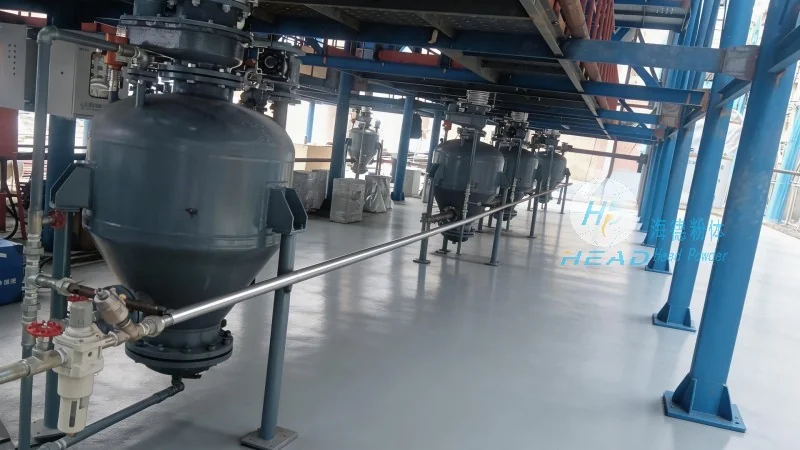
Advantages and Applications
Small bag unpacking material conveying systems offer several advantages in industrial applications. They significantly reduce the manual labor required for material handling, as the system can automatically unpack and transfer materials from bags to processing equipment. This not only improves efficiency but also enhances workplace safety by minimizing the risk of manual handling injuries. The systems are also highly adaptable, allowing them to be integrated into existing production lines or used as standalone units. They are commonly used in industries such as pharmaceuticals, food processing, chemicals, and mining, where bulk materials are packaged in small bags and need to be processed or stored efficiently. The consistent performance of these systems ensures that material flow is uninterrupted, leading to higher production output and reduced operational costs.




