Understanding the core mechanisms and advantages of vacuum material handling systems is crucial for industries seeking efficient and reliable material transport solutions. This article delves into the working principles and key characteristics of such systems, providing insights into how they operate and why they are preferred in various applications.
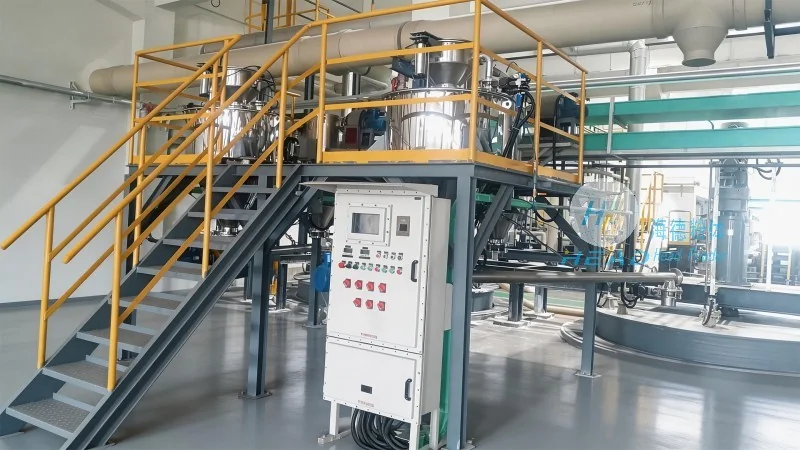
About HeadPowder: Your Trusted Partner in Vacuum Material Handling Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer based in Shandong, China. Specializing in vacuum material handling systems, the company has built a reputation for delivering high-quality, customized solutions tailored to the unique needs of clients across diverse industries. With a focus on innovation and precision engineering, HeadPowder ensures that every system meets the highest standards of performance and durability.
Working Principle of Vacuum Material Handling Systems
The fundamental principle behind vacuum material handling is the creation of a negative pressure (vacuum) within a sealed system. This is typically achieved through the use of a vacuum pump, which draws air out of the system, generating a pressure differential. As a result, external air pressure pushes the material into the vacuum chamber and along the conveying line. The process involves several key components, including a vacuum pump, inlet ports, conveying pipes, and discharge mechanisms. The vacuum pump continuously operates to maintain the negative pressure, ensuring a consistent flow of material. The system can handle a wide range of materials, from powders and granules to small particles, by adjusting the vacuum level and system design to suit the specific material properties.
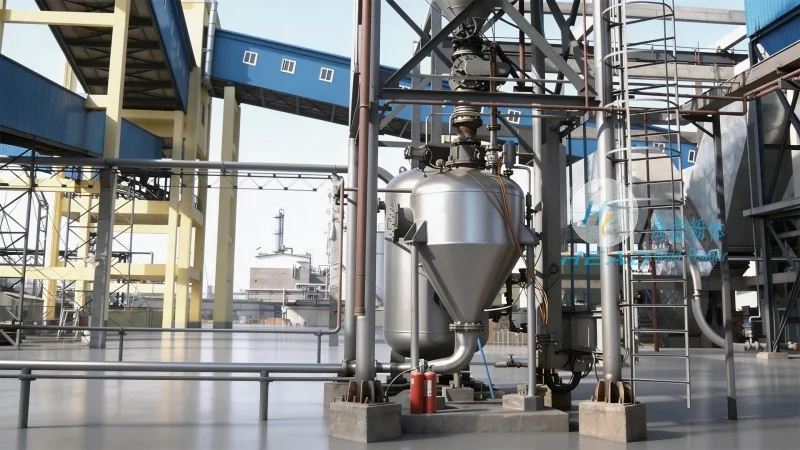
Key Features and Advantages of Vacuum Material Handling Systems
Vacuum material handling systems offer numerous advantages that make them ideal for modern industrial applications. One of the primary benefits is their ability to transport materials over long distances with minimal energy consumption. The sealed system design ensures that the material remains contained, reducing dust emissions and improving safety in the workplace. Additionally, these systems are highly flexible, allowing for easy integration with existing production lines and the ability to handle multiple material types without significant modifications. The automated operation of vacuum systems also enhances productivity by reducing manual labor and minimizing downtime. Furthermore, the compact design of many vacuum material handling solutions makes them suitable for installations with limited space, while the low maintenance requirements contribute to long-term cost savings. Overall, the combination of efficiency, safety, and adaptability makes vacuum material handling a preferred choice for industries such as pharmaceuticals, food processing, and chemical manufacturing.
Applications and Industries Benefiting from Vacuum Material Handling
Vacuum material handling systems are widely used across various industries due to their versatility and effectiveness. In the pharmaceutical industry, these systems are essential for handling sensitive powders and granules, ensuring contamination-free transport and maintaining product integrity. The food processing sector benefits from the hygienic design of vacuum systems, which helps prevent cross-contamination and meets stringent regulatory standards. Chemical manufacturers rely on vacuum material handling to transport hazardous materials safely, while the construction and mining industries use these systems for bulk material transport, improving operational efficiency and reducing labor costs. The adaptability of vacuum systems allows them to be customized for specific applications, making them a valuable asset in any industrial setting.
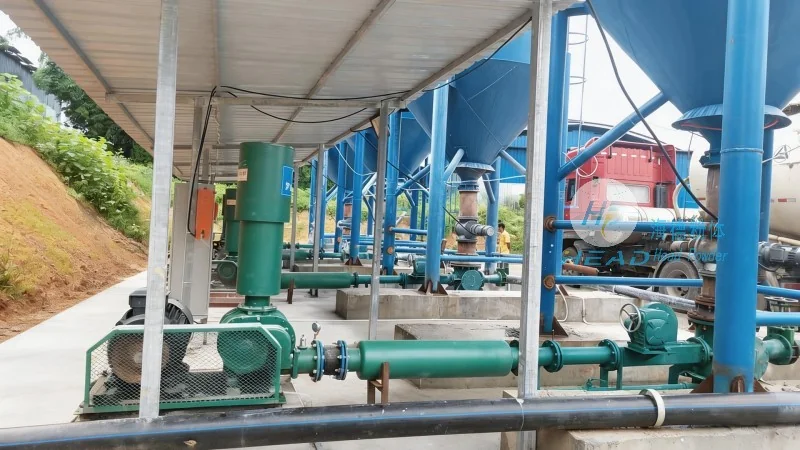
Customization and Integration Capabilities
HeadPowder understands that each client has unique requirements, which is why they offer comprehensive customization options for their vacuum material handling systems. Clients can specify the type of vacuum pump, the material of construction for the conveying pipes, and the discharge mechanism to suit their operational needs. The company also provides integration services to ensure that the new system works seamlessly with existing equipment and production processes. This approach ensures that the final solution is not only efficient but also cost-effective and easy to maintain. By working closely with clients, HeadPowder can develop tailored solutions that address specific challenges, such as material handling in confined spaces or the need for high-precision transport.
Conclusion: The Future of Material Handling with Vacuum Systems
In conclusion, vacuum material handling systems represent a sophisticated and efficient solution for transporting materials in modern industries. By leveraging the principles of negative pressure and sealed systems, these technologies offer significant advantages in terms of safety, productivity, and adaptability. HeadPowder, with its expertise and commitment to quality, continues to be a leading provider of vacuum material handling solutions, helping clients achieve their operational goals while maintaining the highest standards of performance. As industries evolve and demand more efficient material transport solutions, vacuum systems remain a reliable choice, ensuring that material handling remains a critical and effective component of industrial operations.




