Chili powder bulk conveyors are specialized equipment designed to efficiently transport and handle chili powder in industrial settings. As a key component in the processing and distribution of chili-based products, these conveyors play a crucial role in maintaining product quality and operational efficiency. This article will explore the working principle of chili powder bulk conveyors and highlight their key features, providing insights into how they contribute to the smooth operation of chili powder handling processes.
Working Principle of Chili Powder Bulk Conveyors
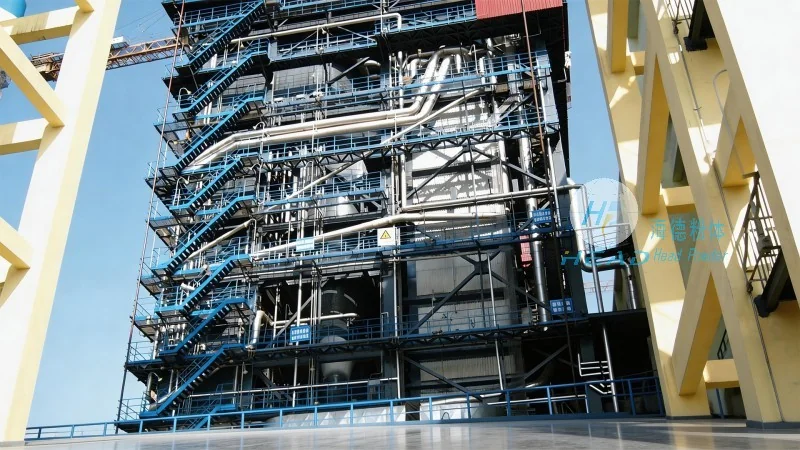
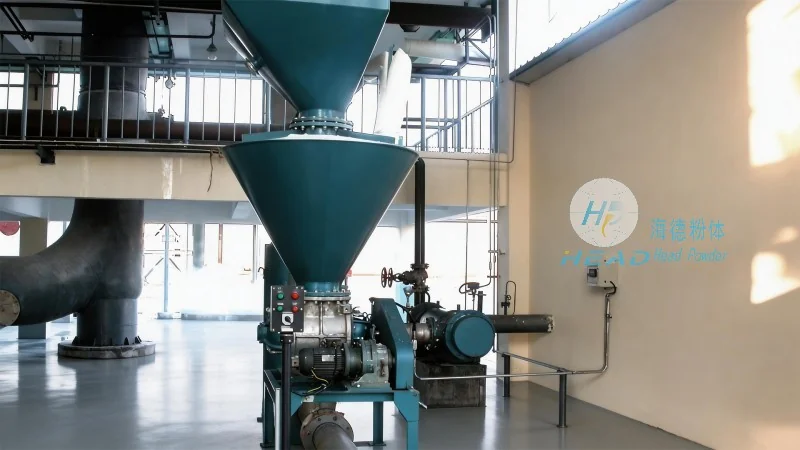
Chili powder bulk conveyors operate based on mechanical principles that enable the movement of bulk materials like chili powder from one location to another. The core mechanism typically involves a combination of components such as a hopper, conveyor belt or screw, and a control system. The process begins with the chili powder being fed into the hopper, where it is stored and prepared for transport. From the hopper, the powder is then transferred to the conveyor system, which moves it along a designated path to the discharge point. The conveyor may use gravity, motorized rollers, or a screw mechanism to propel the powder forward, ensuring consistent and controlled movement. Advanced models may incorporate features like variable speed controls and material flow sensors to optimize the conveying process and prevent issues such as clogging or uneven distribution. The working principle is designed to handle the unique properties of chili powder, including its fine particle size and potential for dust generation, by employing sealed systems and efficient sealing mechanisms to maintain product integrity and prevent contamination.
Key Features of Chili Powder Bulk Conveyors
Chili powder bulk conveyors are equipped with several features that enhance their performance and suitability for handling chili powder. One of the primary features is the use of stainless steel or food-grade materials in their construction, which ensures durability and compliance with hygiene standards in food processing industries. These conveyors are often designed with smooth, non-stick surfaces to minimize the adhesion of chili powder and facilitate easy cleaning, which is essential for maintaining sanitary conditions and preventing cross-contamination. Another important feature is the integration of dust control systems, such as dust collection hoods and filtration units, to manage the fine particles and reduce airborne dust, improving workplace safety and environmental compliance. Additionally, many conveyors are equipped with adjustable speed controls, allowing operators to regulate the flow rate of chili powder based on production requirements and system capacity. This flexibility helps in maintaining consistent product quality and preventing overloading or underloading of the conveyor system. The design also includes safety features like emergency stop buttons and overload protection mechanisms to ensure safe operation and prevent equipment damage during high-demand periods. Furthermore, some models incorporate monitoring systems that provide real-time data on material flow, temperature, and pressure, enabling operators to detect and address issues promptly, thereby enhancing overall operational efficiency.
Application and Benefits in Chili Powder Handling
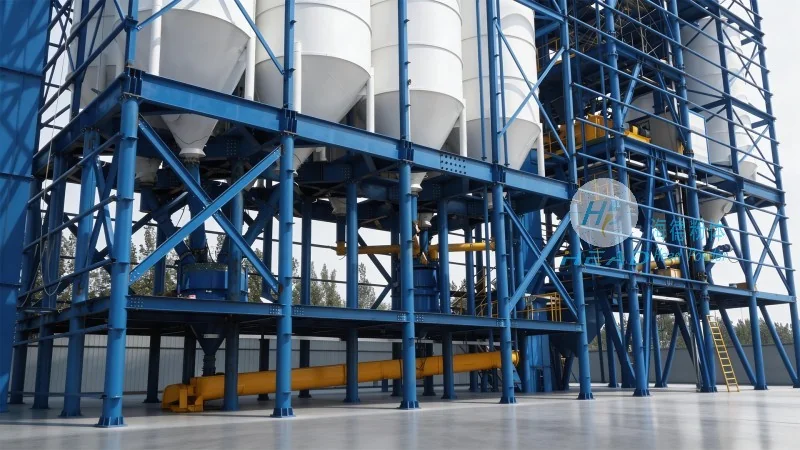
Chili powder bulk conveyors are widely used in various stages of chili powder processing, from raw material handling to packaging. In the raw material stage, they efficiently transport chili powder from storage silos or bulk containers to processing lines, ensuring a continuous supply of material. During processing, these conveyors can be integrated with other equipment such as grinding mills or mixing machines to facilitate the transfer of chili powder between different processing steps. In the packaging stage, they help move the finished chili powder from processing units to packaging lines, where it is packaged into bags or containers for distribution. The benefits of using chili powder bulk conveyors include improved operational efficiency, reduced labor costs, and enhanced product quality. By automating the material handling process, these conveyors minimize the risk of human error and ensure consistent product flow. They also help in maintaining the quality of chili powder by preventing exposure to moisture, air, or contaminants during transport. The ability to handle large volumes of chili powder at a time makes these conveyors ideal for high-volume production facilities, contributing to increased productivity and reduced downtime. Additionally, the sealed and dust-controlled design of these conveyors helps in maintaining a clean and safe working environment, which is crucial for compliance with food safety regulations and industry standards.
Conclusion
In summary, chili powder bulk conveyors are essential equipment for the efficient and safe handling of chili powder in industrial applications. Their working principle, which combines mechanical movement with advanced control systems, enables the smooth transport of chili powder while maintaining product integrity. The key features, including hygienic construction, dust control systems, and adjustable speed controls, enhance their performance and suitability for food processing environments. The applications of these conveyors span from raw material handling to packaging, contributing to improved operational efficiency and product quality. As a result, chili powder bulk conveyors play a vital role in supporting the production and distribution of chili-based products, ensuring that they meet the highest standards of quality and safety. The technology and design of these conveyors continue to evolve, with ongoing improvements aimed at enhancing their efficiency, reliability, and adaptability to the changing needs of the food processing industry.




