As an essential equipment in the powder handling industry, the nitrogen circulation powder conveying line plays a crucial role in ensuring the safe and efficient transportation of powder materials. This system is designed to maintain an inert atmosphere, which is vital for processes that require protection from oxygen and moisture. The following sections will delve into the working principle and key features of this advanced conveying line, providing a comprehensive understanding of its functionality and benefits.
Working Principle of the Nitrogen Circulation Powder Conveying Line
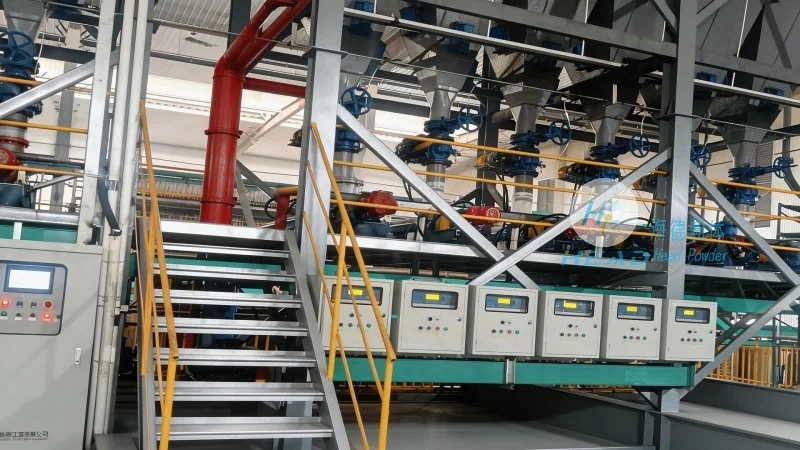
The nitrogen circulation powder conveying line operates on the principle of creating a closed-loop system where nitrogen gas is continuously recirculated to maintain a stable inert environment. The process begins with the introduction of nitrogen gas into the conveying system, which displaces air and other contaminants from the powder material. The system typically consists of several key components, including a nitrogen generator or supply unit, a conveying pipeline network, and a series of valves and control mechanisms. The nitrogen gas is pressurized and directed through the pipeline, carrying the powder particles along with it. As the powder moves through the system, the nitrogen gas is filtered and purified to remove any particulate matter or moisture, ensuring the quality of the gas remains consistent. The recirculation of nitrogen gas not only enhances the efficiency of the conveying process but also reduces operational costs by minimizing the need for continuous fresh gas supply. The control system monitors parameters such as pressure, flow rate, and temperature to maintain optimal performance and prevent any potential issues like blockages or leaks.
Key Features of the Nitrogen Circulation Powder Conveying Line
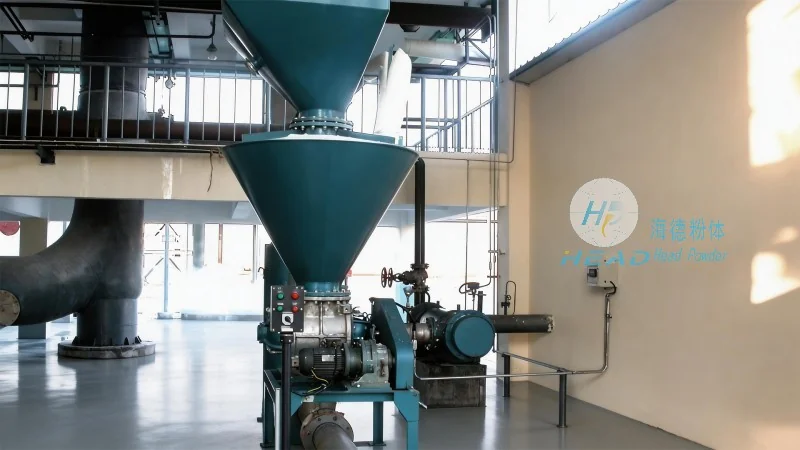
One of the primary features of this conveying line is its ability to maintain an inert atmosphere throughout the entire transportation process. This is achieved through the continuous circulation of nitrogen gas, which effectively prevents oxidation and moisture absorption in the powder material. The system is equipped with advanced filtration and drying units that ensure the nitrogen gas remains free from contaminants, thereby preserving the quality of the conveyed powder. Another notable feature is the high efficiency and low energy consumption of the system. By utilizing a closed-loop design, the nitrogen gas is reused rather than being discharged, resulting in significant energy savings and reduced environmental impact. The conveying line also offers flexibility in terms of material handling, as it can accommodate a wide range of powder types, including those that are sensitive to air exposure. The modular design of the system allows for easy integration with existing production lines and facilitates maintenance and repairs. Additionally, the system is equipped with safety features such as pressure relief valves and emergency shut-off mechanisms to ensure safe operation in case of any anomalies. The user-friendly control interface enables operators to monitor and adjust the system parameters with ease, enhancing operational efficiency and reducing the risk of human error.
Applications and Benefits in Industrial Settings
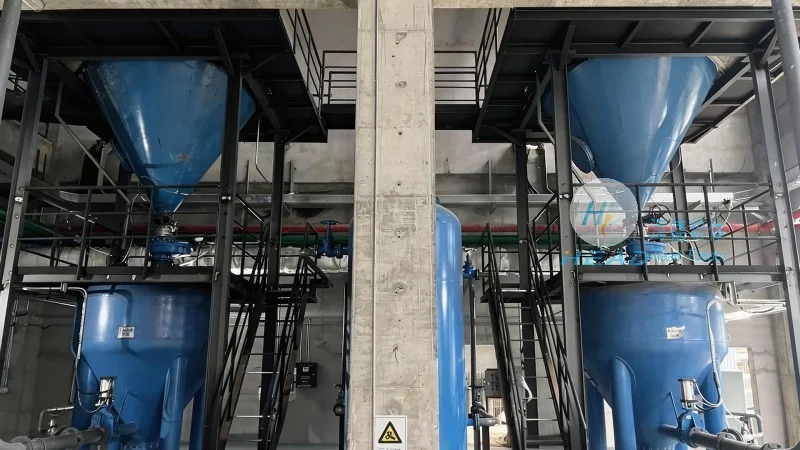
The nitrogen circulation powder conveying line finds extensive applications in various industries, including pharmaceuticals, food processing, and chemical manufacturing. In the pharmaceutical industry, it is used to transport sensitive active ingredients that require protection from moisture and oxygen, ensuring product quality and stability. In the food industry, the system is employed to convey powders like flour, sugar, and spices, maintaining their freshness and preventing contamination. The chemical industry benefits from the system's ability to handle reactive powders, preventing unwanted reactions and ensuring safe handling. The benefits of using this conveying line extend beyond just material handling; it also contributes to improved product quality, reduced waste, and enhanced operational safety. The consistent inert environment provided by the system helps maintain the purity of the powder, which is critical in industries where product specifications are stringent. Furthermore, the energy-efficient design of the system leads to lower operational costs over time, making it a cost-effective solution for long-term use. The reliability of the system, with its robust construction and advanced control mechanisms, ensures minimal downtime and maximizes productivity in industrial settings.
Conclusion and Company Information
In conclusion, the nitrogen circulation powder conveying line is a sophisticated and essential equipment for the safe and efficient handling of powder materials. Its working principle, based on the continuous recirculation of nitrogen gas, ensures an inert environment that protects the material from oxidation and moisture. The key features, including high efficiency, low energy consumption, and flexibility, make it a preferred choice in various industrial applications. The system's ability to maintain product quality, reduce waste, and enhance operational safety makes it a valuable asset for any production line. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such advanced conveying systems, with a strong commitment to quality and customer satisfaction. With its headquarters in Shandong, China, the company leverages its expertise and experience to deliver reliable and efficient solutions tailored to the specific needs of its clients. The nitrogen circulation powder conveying line, as part of the company's product portfolio, represents a significant advancement in powder handling technology, offering a sustainable and effective solution for modern industrial requirements.




