For agricultural and feed processing enterprises, the efficient and stable operation of corn feed powder conveying systems is crucial. This equipment is specifically designed to handle corn feed powders, ensuring smooth material transport from storage to processing or packaging stages. Understanding the core components and design principles of such systems is essential for optimizing production efficiency and maintaining product quality.
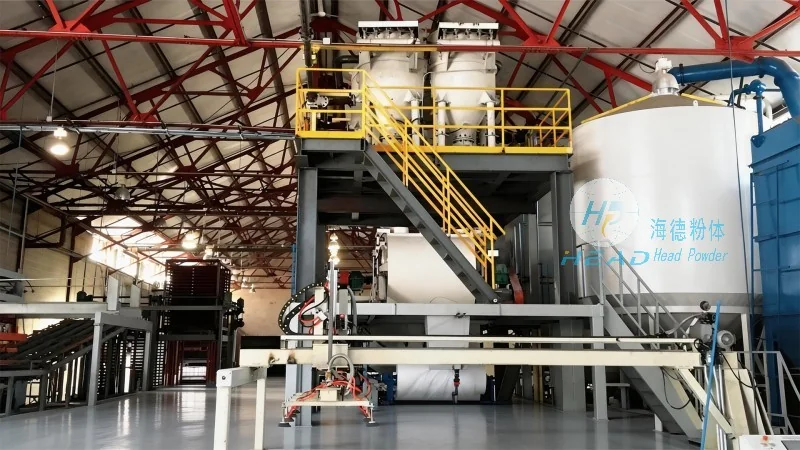
Key Components of the Corn Feed Powder Conveying System
The corn feed powder conveying system typically consists of several critical components that work in tandem to achieve effective material handling. These include feed hoppers, screw conveyors or pneumatic ducts, control valves, and dust collection systems. The feed hopper is responsible for storing and feeding the corn feed powder into the conveying line. Screw conveyors are often used for horizontal or slight incline transport, while pneumatic ducts are suitable for vertical or longer distance transport. Control valves regulate the flow rate and pressure within the system, ensuring stable operation. Dust collection systems are integrated to manage and control dust emissions, maintaining a safe and clean working environment.
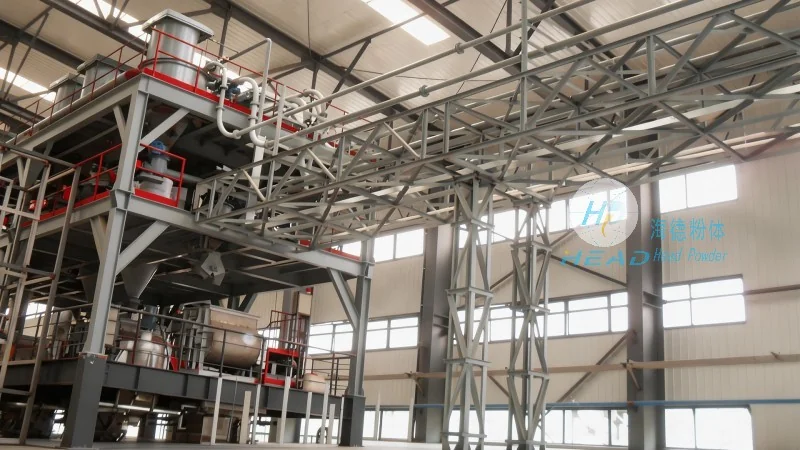
Design Principles of the Conveying System
The design of a corn feed powder conveying system follows several key principles to ensure optimal performance. First, the system must be designed to handle the specific physical properties of corn feed powders, such as particle size, moisture content, and flowability. This involves selecting appropriate materials for the hopper and conveyor components to prevent material buildup or blockages. Second, the system is engineered for energy efficiency, minimizing power consumption while maintaining high conveying capacity. This is achieved through the use of efficient motor drives and optimized conveyor designs. Third, the system prioritizes safety and operational reliability. This includes features like overload protection, emergency stop mechanisms, and regular maintenance access points. Additionally, the design considers the need for easy cleaning and maintenance to reduce downtime and operational costs.
Application Scenarios and Benefits
Corn feed powder conveying systems are widely used in various applications within the feed processing industry. They are commonly employed in feed mills, where corn feed is transported from storage silos to mixing and grinding equipment. The system ensures a consistent and continuous supply of raw materials, which is vital for maintaining production schedules and product consistency. Another application is in animal feed manufacturing facilities, where the system transports mixed feed powders to packaging lines. The benefits of using such a system include improved production efficiency, reduced labor costs, and enhanced product quality. By maintaining a stable flow of materials, the system minimizes the risk of material degradation or contamination, which is critical for producing high-quality animal feed.
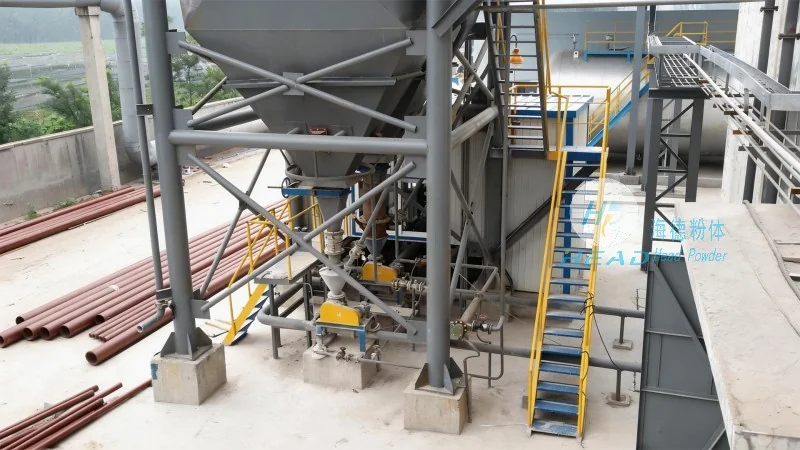
Company Information: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of powder handling equipment, specializes in providing customized solutions for corn feed powder conveying systems. With a strong focus on innovation and quality, the company has developed advanced technologies to meet the diverse needs of the feed processing industry. HeadPowder's products are designed to be durable, efficient, and reliable, ensuring long-term performance and low maintenance costs. The company's headquarters is located in Shandong, China, where it has a team of experienced engineers and technicians dedicated to research, development, and customer support. HeadPowder is committed to delivering high-quality equipment that meets international standards and customer expectations, helping feed processing enterprises achieve their production goals with optimal efficiency.




