When it comes to the efficient and reliable transportation of manganese carbonate, pneumatic conveying systems offer a sophisticated solution that addresses the unique challenges associated with handling this specific material. Manganese carbonate is widely used in various industrial applications, including battery production, steelmaking, and chemical manufacturing, making its safe and efficient movement from storage to processing facilities critical for operational success. Pneumatic conveying, as a technology, utilizes air or other gases to transport bulk materials like manganese carbonate through a pipeline network, eliminating the need for traditional mechanical conveying equipment such as belts or buckets.
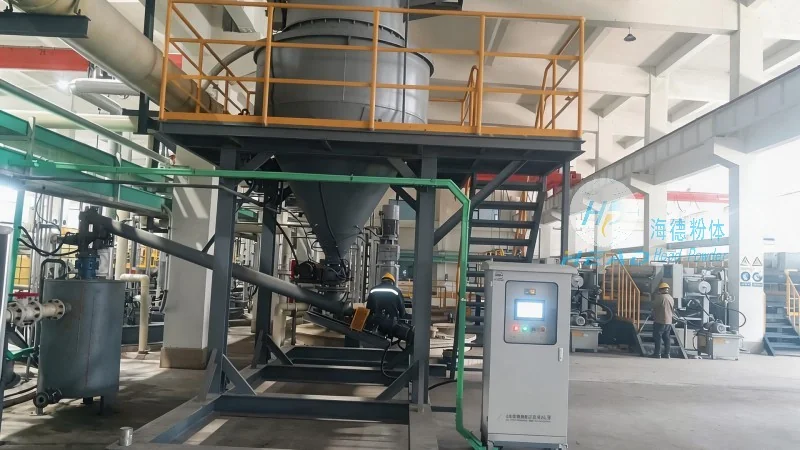
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in designing and implementing advanced pneumatic conveying solutions tailored to the demands of manganese carbonate handling. With a focus on innovation and precision engineering, the company has developed systems that optimize material flow, minimize dust generation, and ensure compliance with safety and environmental standards. The company's expertise lies in understanding the physical properties of manganese carbonate—such as its particle size, moisture content, and flow characteristics—and adapting the conveying system accordingly to achieve maximum efficiency and minimal operational disruptions.
Key Advantages of Pneumatic Conveying for Manganese Carbonate
One of the primary advantages of pneumatic conveying in the context of manganese carbonate transportation is its ability to handle materials with varying particle sizes and moisture levels without the need for pre-treatment or conditioning. Unlike mechanical conveyors, which may struggle with cohesive or sticky materials, pneumatic systems can effectively transport manganese carbonate even when it contains moisture, preventing blockages and ensuring consistent flow rates. Additionally, pneumatic conveying reduces the risk of material contamination, as the material remains enclosed within the pipeline, minimizing exposure to external elements and preventing cross-contamination with other substances.
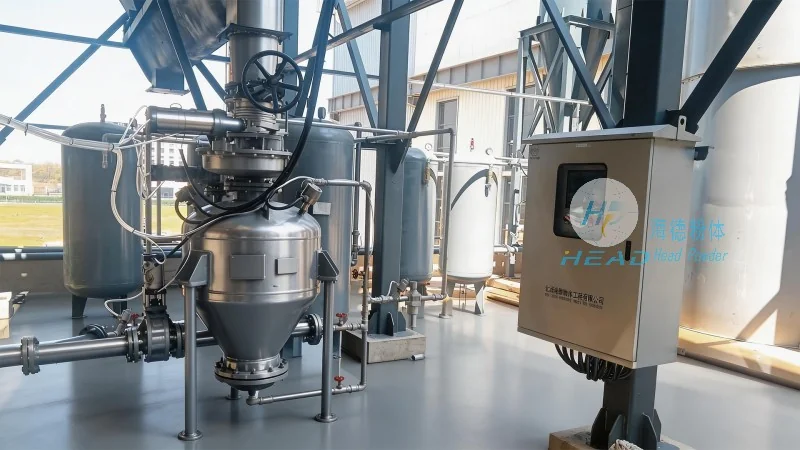
Another significant benefit is the energy efficiency of pneumatic conveying systems. By using air pressure to move materials, these systems can achieve high throughput with lower energy consumption compared to traditional methods. This not only reduces operational costs but also aligns with sustainability goals, as less energy is required to transport the material. The system's flexibility also allows for easy integration with existing production lines, enabling seamless transitions between storage, processing, and packaging stages without the need for extensive modifications to the facility layout.
Application Scenarios and System Design
Pneumatic conveying systems for manganese carbonate are commonly employed in scenarios where materials need to be transported over long distances or through complex layouts, such as in large-scale mining and processing plants. The design of these systems typically involves a combination of positive and negative pressure conveying, depending on the specific requirements of the application. Positive pressure systems, which blow air into the pipeline, are ideal for short to medium distances and can handle larger particle sizes, while negative pressure systems, which draw material into the pipeline, are better suited for longer distances and more sensitive applications where dust control is paramount.
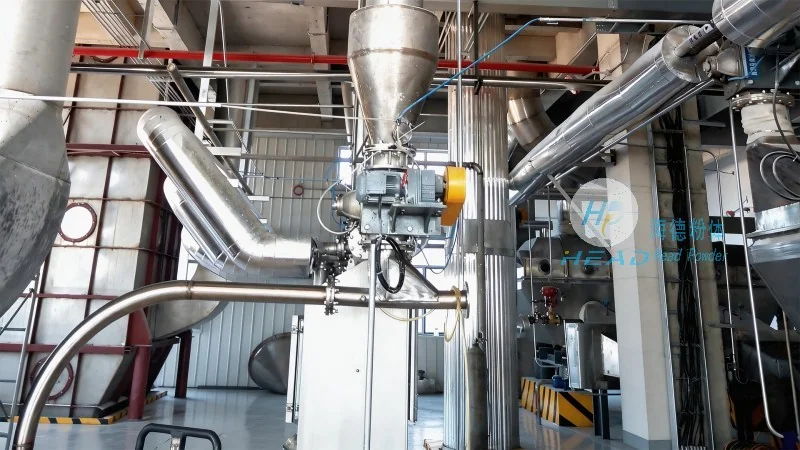
Shandong HeadPowder Engineering Co., Ltd. takes a customized approach to system design, considering factors such as the volume of material to be transported, the distance between source and destination, and the existing infrastructure of the facility. The company's engineers work closely with clients to assess their operational needs and recommend the most suitable conveying configuration, whether it involves a single pipeline or a network of interconnected lines. This tailored approach ensures that the system not only meets current requirements but also provides scalability for future growth, allowing businesses to adapt to changing production demands without significant investment in new equipment.
Enhancing Safety and Environmental Compliance
Handling manganese carbonate requires adherence to strict safety and environmental regulations, and pneumatic conveying systems are designed to address these concerns effectively. The enclosed nature of the conveying process minimizes dust emissions, reducing the risk of respiratory issues for workers and preventing environmental contamination. Additionally, the systems are equipped with advanced filtration and dust collection mechanisms that capture and neutralize any airborne particles, ensuring compliance with local and international standards. This focus on safety and environmental responsibility is a core part of Shandong HeadPowder Engineering Co., Ltd.'s mission, as the company understands that sustainable operations are essential for long-term success in the industry.
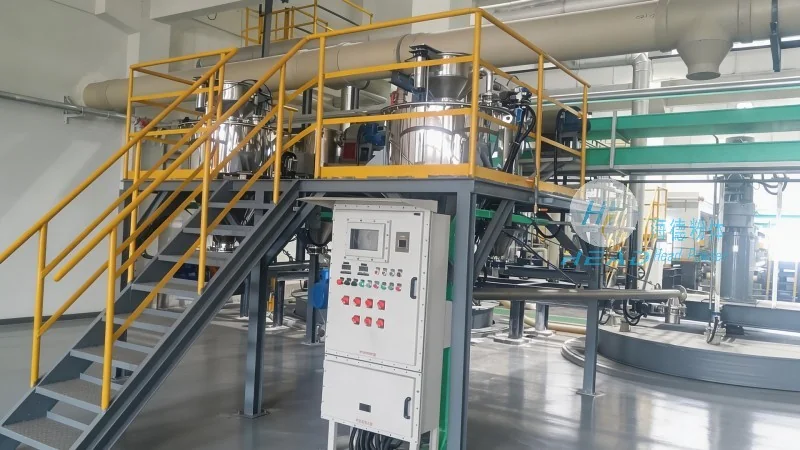
Furthermore, pneumatic conveying reduces the need for manual handling of heavy or bulky materials, minimizing the risk of workplace injuries and improving overall operational safety. By automating the material transport process, the company helps clients achieve a safer working environment while maintaining high productivity levels. The integration of modern control systems and monitoring tools also allows for real-time tracking of material flow, enabling quick identification and resolution of any issues that may arise during operation.
Conclusion and Future Outlook
In conclusion, pneumatic conveying plays a vital role in the efficient and safe transportation of manganese carbonate, offering numerous advantages over traditional mechanical methods. Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in implementing these advanced systems, leveraging its expertise to deliver customized solutions that meet the unique needs of each client. As industries continue to demand higher efficiency and sustainability in material handling, pneumatic conveying technology will remain a key component in optimizing operations for manganese carbonate processing. The company's commitment to innovation and quality ensures that clients can rely on their systems for years to come, supporting their growth and success in the competitive global market.




