Efficient and clean handling of talc powder is a critical concern for industries relying on this mineral for various applications. Traditional methods often face challenges such as dust contamination, material loss, and operational inefficiencies. This article explores how pneumatic conveying technology offers a superior solution to enhance talc powder handling efficiency while maintaining a clean working environment.
Understanding Talc Powder Handling Challenges
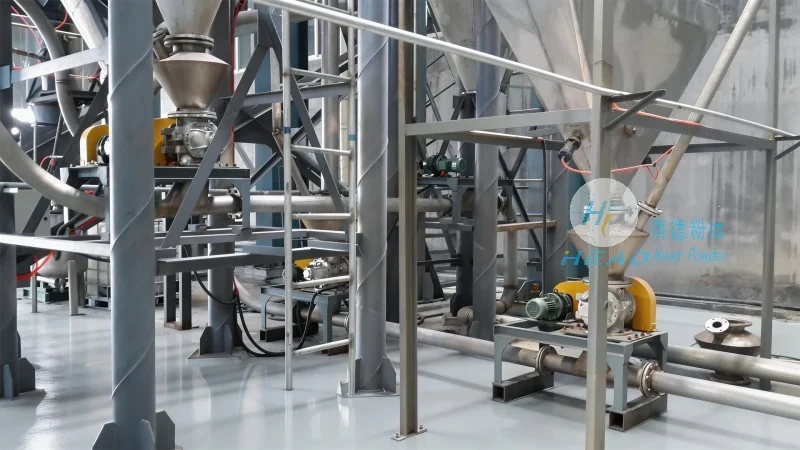
Talc powder, a soft mineral with a high moisture content and fine particle size, presents unique challenges during transportation and processing. Conventional methods like belt conveyors or bucket elevators can lead to dust dispersion, product degradation, and increased maintenance costs. The need for a system that minimizes contamination and maximizes throughput has driven the adoption of advanced pneumatic conveying solutions.
Pneumatic Conveying Technology: How It Works
Pneumatic conveying uses compressed air to transport dry bulk materials like talc powder through a pipeline system. The process involves creating a flow of air that carries the powder particles, ensuring a continuous and controlled movement from the source to the destination. There are two primary types of pneumatic conveying: pressure and vacuum systems. Pressure systems use positive pressure to push the material through the pipeline, while vacuum systems use negative pressure to pull it. For talc powder, pressure systems are often preferred due to their ability to handle high volumes and long distances with minimal pressure drops.
Key Benefits of Pneumatic Conveying for Talc Powder
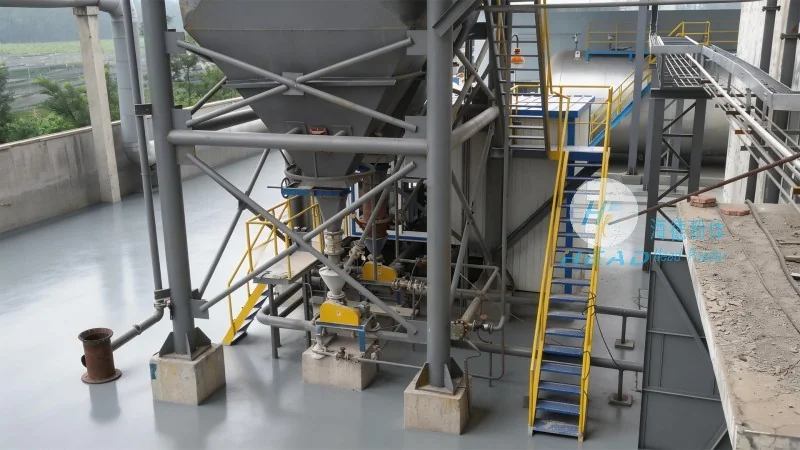
Implementing pneumatic conveying for talc powder handling brings several advantages that directly impact operational efficiency and product quality. First, it significantly reduces dust exposure, creating a cleaner workplace and minimizing health risks for operators. This is particularly important in industries where talc is used in food, cosmetics, or pharmaceutical applications, where purity is paramount. Second, the system minimizes material loss and degradation, as the powder is contained within the pipeline, preventing contact with external contaminants. Third, pneumatic conveying offers higher throughput and flexibility, allowing for integration with existing production lines and easy adjustment of flow rates. Additionally, the technology reduces energy consumption compared to traditional methods, contributing to lower operational costs and a smaller environmental footprint.
HeadPowder: Your Partner in Talc Powder Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling systems, specializes in designing and manufacturing customized pneumatic conveying solutions tailored to the unique needs of talc powder applications. With years of experience in the industry, HeadPowder understands the challenges faced by manufacturers and offers innovative solutions that enhance efficiency and maintain product integrity. The company’s expertise lies in selecting the appropriate conveying system, whether it’s a pressure or vacuum design, based on factors such as material characteristics, distance, and throughput requirements. HeadPowder’s team of engineers works closely with clients to assess their specific needs and develop a system that meets their operational goals.
Customization and Integration: Ensuring Optimal Performance
Every talc powder handling application is unique, and HeadPowder recognizes the importance of customization in achieving optimal performance. The company offers a range of components, including feeders, cyclones, filters, and control systems, that can be integrated into a comprehensive pneumatic conveying system. For example, a feed hopper with a rotary valve ensures a consistent flow of talc powder into the pipeline, while a cyclone separator effectively separates the powder from the air stream, allowing for recycling of the air and reducing waste. The control system, often equipped with sensors and automation, monitors the conveying process in real-time, providing data on flow rates, pressure, and temperature. This allows for immediate adjustments to maintain the desired performance and prevent system failures.
Case Study: Improved Efficiency and Cleanliness in a Talc Processing Plant
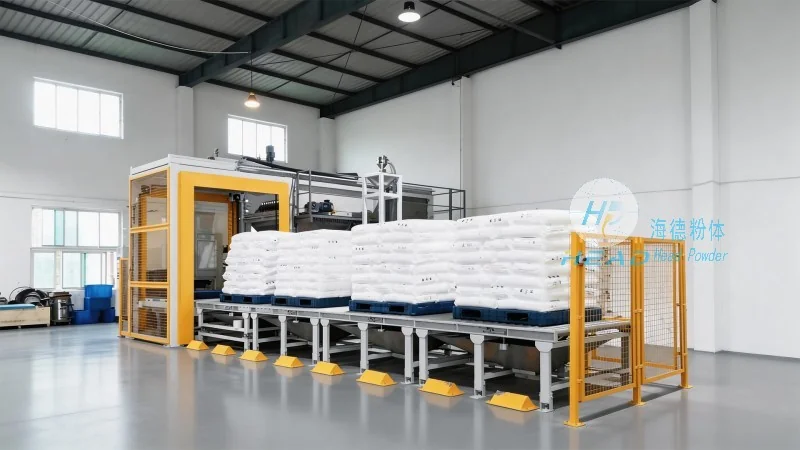
One of HeadPowder’s clients, a leading manufacturer of talc-based products, faced significant challenges with dust contamination and low throughput in their existing handling system. By implementing a customized pneumatic conveying solution from HeadPowder, the client achieved a 30% increase in handling efficiency and a 90% reduction in dust exposure. The new system also reduced material loss by 15%, resulting in cost savings and improved product quality. The client’s operations now run smoothly, with minimal downtime and consistent performance, demonstrating the effectiveness of pneumatic conveying in talc powder handling.
Conclusion: The Future of Talc Powder Handling
Pneumatic conveying technology has proven to be a game-changer in enhancing talc powder handling efficiency and maintaining a clean working environment. By leveraging the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., industries can overcome the challenges associated with traditional handling methods and achieve higher productivity and product quality. As the demand for talc powder continues to grow, the adoption of advanced pneumatic conveying systems will be crucial in meeting the needs of manufacturers while ensuring safety and environmental compliance.




