For industrial facilities dealing with dust collection and ash transport, optimizing the process for efficiency and cleanliness is paramount. Traditional methods often face challenges such as material degradation, contamination, and operational inefficiencies. Pneumatic conveying technology emerges as a superior solution, offering a clean, efficient, and reliable method to handle dust collection ash. This article delves into the principles, benefits, and practical applications of pneumatic conveying systems tailored for this specific industry need.
Pneumatic Conveying Technology: How It Works
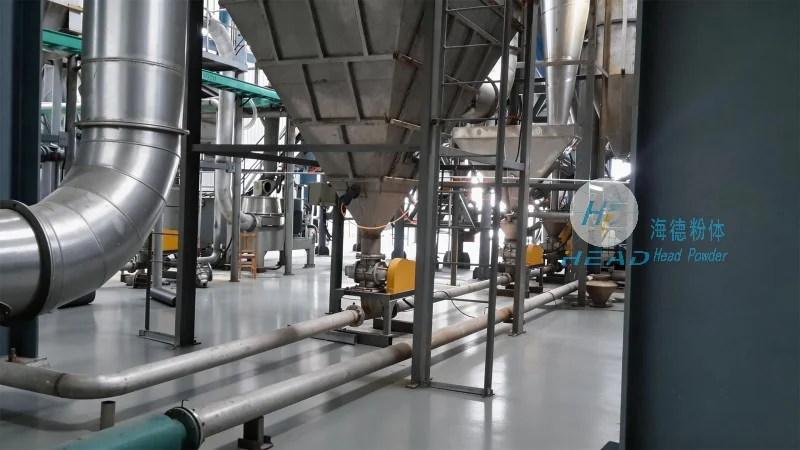
Pneumatic conveying systems utilize air or gas to transport bulk materials like dust collection ash through a pipeline network. The process typically involves a blower or compressor that generates airflow, which then propels the material through the system. There are two primary types of pneumatic conveying: dilute phase and dense phase. Dilute phase systems use high-velocity air to move material in a suspended state, suitable for short to medium distances and low to medium material loads. Dense phase systems, on the other hand, use lower velocities and higher pressure to transport material in a slurry-like state, ideal for longer distances and higher material loads. The choice between these systems depends on the specific requirements of the industrial application, including material characteristics, distance, and desired flow rates.
The Benefits of Pneumatic Conveying for Dust Collection Ash Transport
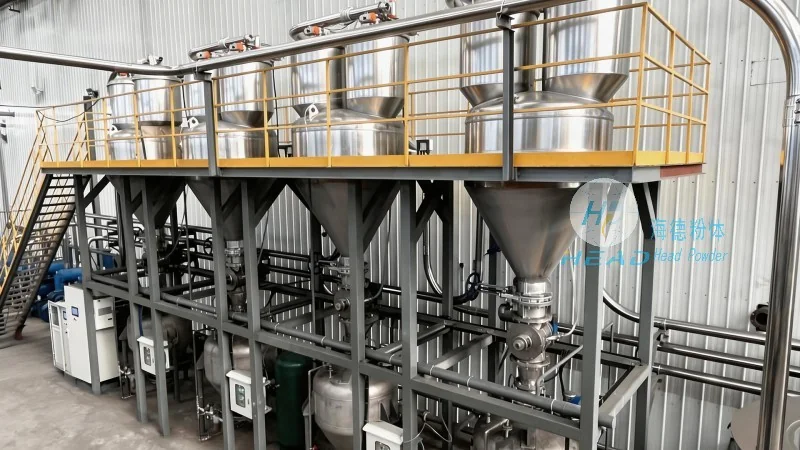
Implementing pneumatic conveying for dust collection ash transport offers numerous advantages over traditional methods. Firstly, it provides a clean and hygienic operation, as the material is contained within a sealed pipeline system, preventing dust dispersion into the environment and reducing the risk of contamination. This is particularly important in industries where product purity and environmental compliance are critical. Secondly, pneumatic conveying enhances operational efficiency by enabling continuous, automated material transport, reducing downtime and labor costs. The technology also allows for precise control over flow rates and pressure, ensuring consistent material handling and minimizing material degradation. Additionally, the system's compact design and flexibility make it suitable for integration into existing industrial setups, adapting to various facility layouts and spatial constraints.
Key Features and Advantages of Pneumatic Conveying Systems
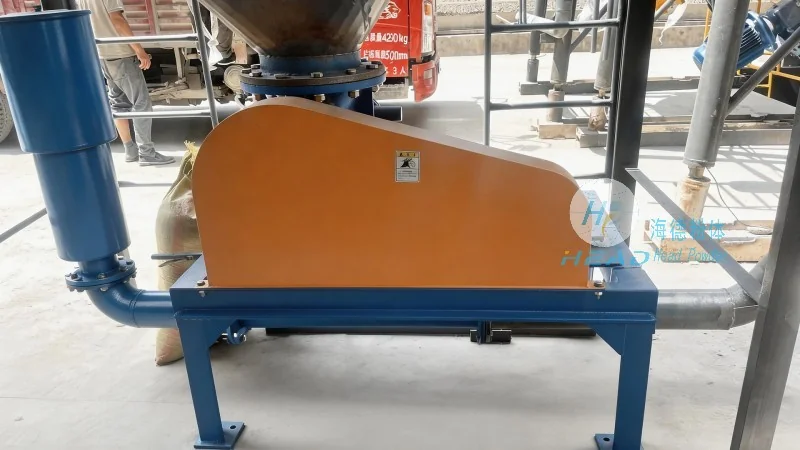
Modern pneumatic conveying systems for dust collection ash transport are equipped with several key features that enhance performance and reliability. These include advanced blower technology for efficient air delivery, variable speed drives to adjust flow rates dynamically, and robust pipeline materials resistant to corrosion and abrasion from the ash. The systems also incorporate monitoring and control systems that allow real-time tracking of material flow, pressure, and temperature, enabling proactive maintenance and troubleshooting. Furthermore, the modular design of these systems allows for easy expansion or modification as operational needs evolve, providing long-term value and adaptability. The combination of these features ensures that the pneumatic conveying system operates reliably, efficiently, and safely, meeting the stringent demands of industrial dust collection and ash transport applications.
Case Study: HeadPowder's Pneumatic Conveying Solutions
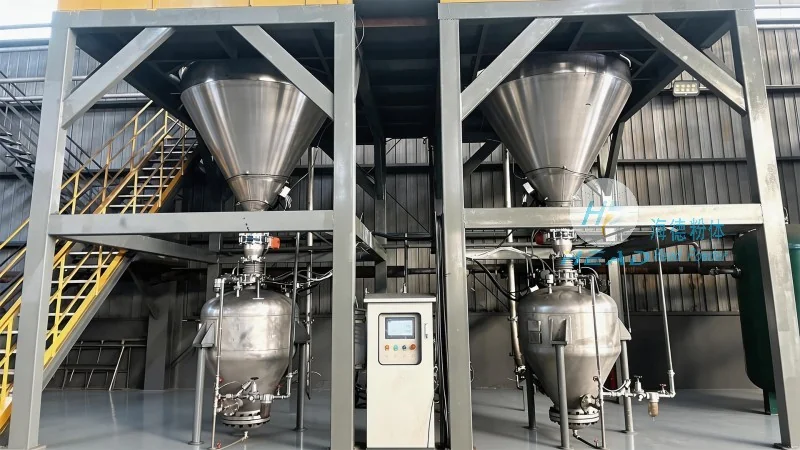
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial engineering solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of dust collection ash transport. With a focus on efficiency, cleanliness, and reliability, HeadPowder's systems have been successfully implemented in various industrial facilities across China. For instance, a client in the power generation industry faced challenges with traditional ash transport methods, leading to increased operational costs and environmental concerns. By adopting HeadPowder's pneumatic conveying system, the facility achieved significant improvements in material transport efficiency, reduced labor requirements, and enhanced environmental compliance. The system's ability to handle high volumes of ash while maintaining a clean and sealed operation demonstrated the effectiveness of pneumatic conveying in solving complex industrial challenges. HeadPowder's expertise in engineering and manufacturing ensures that their pneumatic conveying solutions are customized to meet specific client requirements, providing a reliable and efficient solution for dust collection ash transport.
Conclusion: Choosing the Right Pneumatic Conveying Solution
For industrial facilities seeking to optimize dust collection ash transport, pneumatic conveying technology offers a clean, efficient, and reliable solution. By understanding the principles and benefits of pneumatic conveying, as well as the key features and advantages of modern systems, facilities can make informed decisions to enhance their operational performance. Companies like Shandong HeadPowder Engineering Co., Ltd. provide specialized engineering and manufacturing services to design and implement tailored pneumatic conveying systems that meet the unique needs of each industrial application. By investing in a pneumatic conveying system, facilities can achieve improved efficiency, reduced costs, and enhanced environmental compliance, ensuring long-term success in their operations.




