HeadPowder, a leading engineering firm based in Shandong, China, specializes in the application and optimization of pneumatic conveying technology for cement raw material transport. This technology has become increasingly vital in modern cement production, offering efficient and reliable solutions for handling bulk materials like limestone, clay, and iron ore.
Understanding Pneumatic Conveying in Cement Production
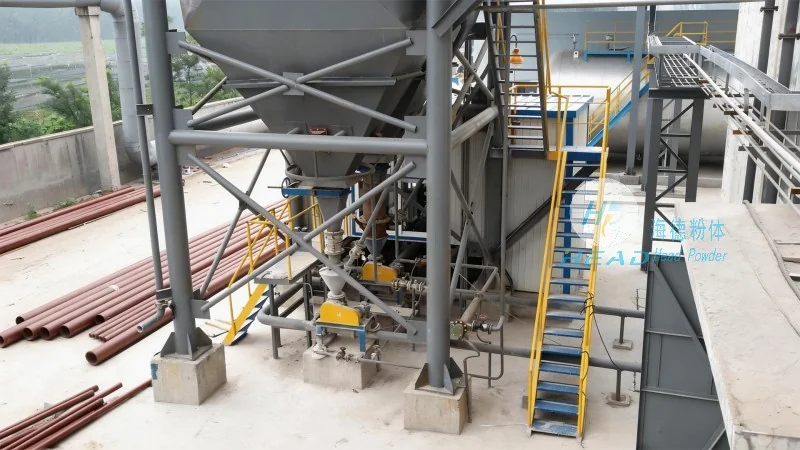
Pneumatic conveying systems utilize air or gas to transport solid materials through pipelines. In the context of cement raw material handling, this technology ensures seamless movement from storage silos to the preheater or kiln. The primary advantage lies in its ability to minimize material degradation, reduce dust emissions, and enhance overall operational efficiency compared to traditional mechanical conveying methods.
Key Benefits of Pneumatic Conveying for Cement Plants
For cement manufacturers, pneumatic conveying offers several critical benefits. Firstly, it provides a dust-free environment, which is essential for maintaining workplace safety and compliance with environmental regulations. Secondly, the system reduces the risk of material breakage, preserving the quality of raw materials, especially delicate components like limestone. Thirdly, the automated nature of pneumatic conveying minimizes labor costs and human error, leading to consistent and reliable material flow. Additionally, the technology allows for flexible layout designs, enabling plants to adapt to changing production needs without major infrastructure overhauls.
HeadPowder's Expertise in Design and Implementation
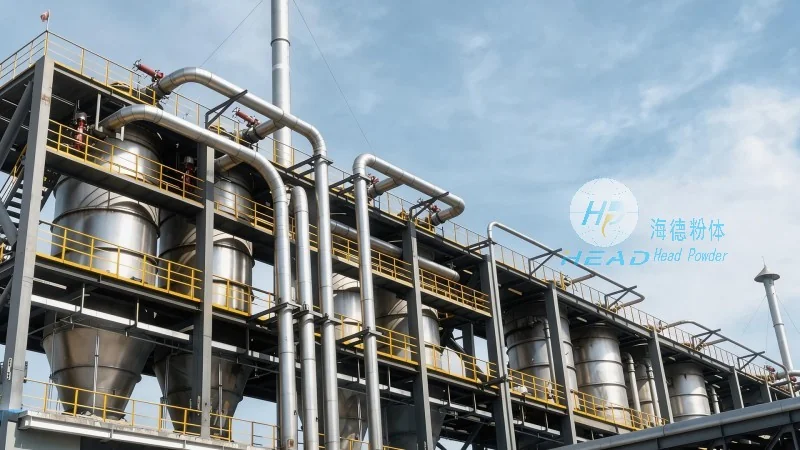
Shandong HeadPowder Engineering Co., Ltd. leverages its extensive experience to design customized pneumatic conveying solutions tailored to the specific requirements of cement plants. Our team of engineers conducts thorough site assessments and material analysis to determine the most suitable conveying system, whether it's a positive pressure, negative pressure, or hybrid system. We focus on optimizing the system's performance by selecting appropriate air velocities, pipeline diameters, and material handling capacities, ensuring that the design meets both current and future production demands.
Optimization Strategies for Enhanced Performance
Optimizing pneumatic conveying systems involves several key strategies. One critical aspect is the selection of the right air compressor and filter system to maintain consistent air pressure and quality. Regular maintenance of the pipeline network, including cleaning and inspection, is essential to prevent blockages and ensure long-term system reliability. Additionally, implementing advanced control systems allows for real-time monitoring of material flow rates and pressure differentials, enabling immediate adjustments to maintain optimal performance. HeadPowder employs these strategies to help clients achieve higher throughput, lower energy consumption, and extended equipment lifespan.
Case Studies and Successful Implementations
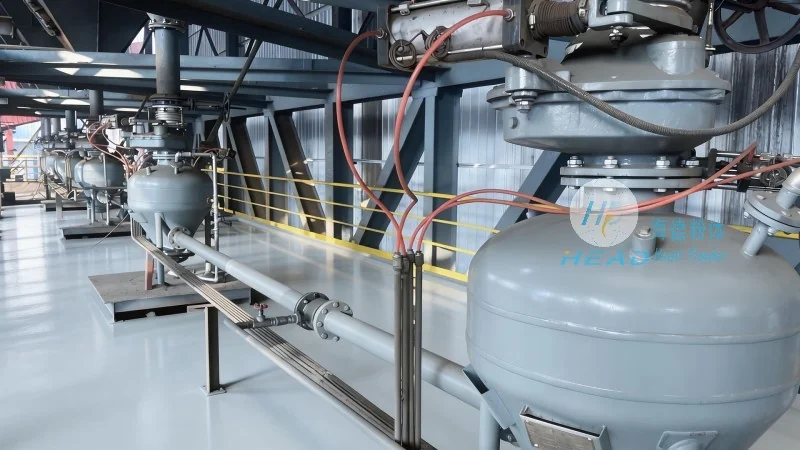
HeadPowder has successfully implemented pneumatic conveying systems for numerous cement plants across China. For instance, a major cement manufacturer in Shandong reduced material handling costs by 15% and improved dust control by 90% after adopting our optimized system. Another client, located in the eastern region, enhanced their production capacity by 20% through the installation of a high-capacity pneumatic conveying line. These case studies highlight the tangible benefits of our expertise in designing and implementing efficient pneumatic conveying solutions.
Conclusion and Future Outlook
As the cement industry continues to evolve, the importance of efficient raw material transport cannot be overstated. Pneumatic conveying technology, when properly designed and optimized, offers a robust solution to meet these challenges. HeadPowder remains committed to delivering innovative and reliable solutions that enhance the performance and sustainability of cement production facilities. By leveraging our technical expertise and customer-centric approach, we help cement plants achieve their operational goals while maintaining high standards of safety and environmental responsibility.




