HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for the efficient transport of nanometer calcium carbonate. This article provides an in - depth look at the long - distance pneumatic conveying system specifically engineered for nanometer calcium carbonate, highlighting its technical features, operational advantages, and practical applications.
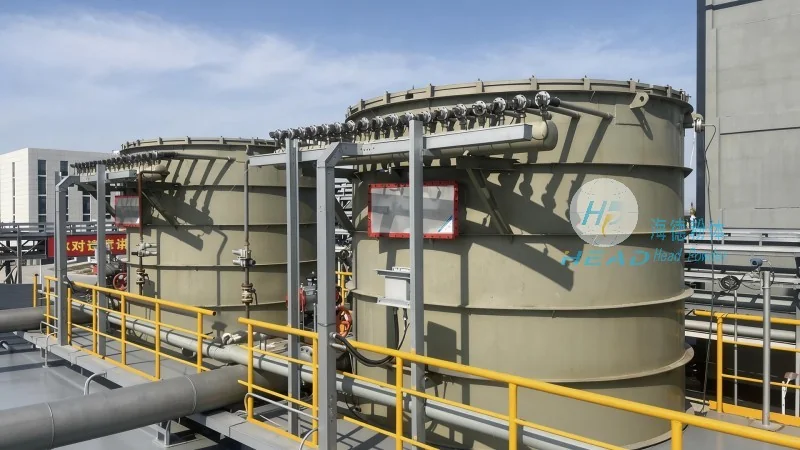
System Overview and Core Components
The long - distance pneumatic conveying system for nanometer calcium carbonate is a sophisticated solution that integrates multiple components to ensure reliable and efficient material transport over extended distances. At its core, the system comprises a series of key elements, including a material feeder, a high - pressure air compressor, a conveying pipeline network, and a dust collection and control unit. The material feeder is designed to handle the fine, powdery nature of nanometer calcium carbonate, ensuring consistent and controlled feeding into the system. The high - pressure air compressor provides the necessary air pressure to drive the material through the pipeline, while the conveying pipeline network is constructed from durable materials that can withstand the abrasive properties of the nanometer calcium carbonate particles. The dust collection and control unit is crucial for maintaining air quality and preventing environmental contamination, as nanometer calcium carbonate is a fine powder that can easily become airborne.
Technical Advantages and Performance Characteristics
One of the primary advantages of this long - distance pneumatic conveying system is its ability to transport nanometer calcium carbonate over significant distances with minimal material loss and high efficiency. The system operates under positive pressure, which helps to prevent the material from settling in the pipeline and ensures a continuous flow. The high - pressure air compressor is equipped with advanced control systems that allow for precise adjustment of air pressure and flow rate, optimizing the conveying process for different material characteristics and distance requirements. Additionally, the conveying pipeline is designed with smooth internal surfaces and appropriate diameter to minimize friction and energy consumption, further enhancing the system's overall performance. The system also features a self - cleaning mechanism that helps to prevent clogging and maintain consistent operation over time.
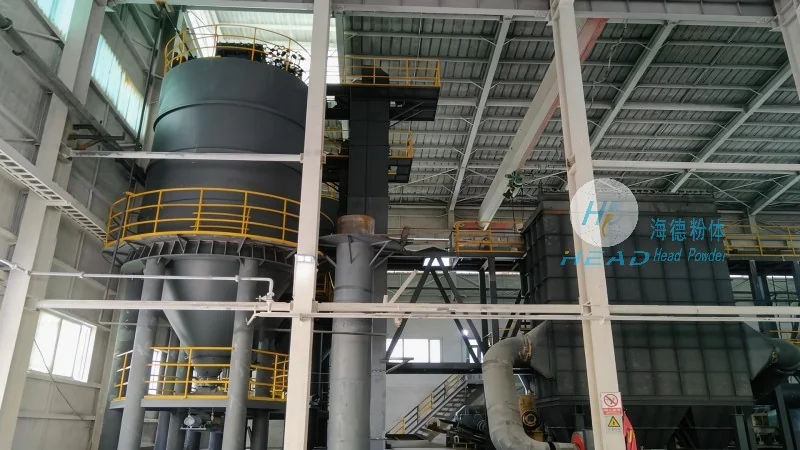
Application Scenarios and Industry Benefits
The long - distance pneumatic conveying system for nanometer calcium carbonate is widely used in various industrial applications, particularly in the production of coatings, plastics, and rubber products, where high - purity nanometer calcium carbonate is essential. By efficiently transporting the material from storage facilities to processing plants, the system reduces the need for manual handling and minimizes the risk of contamination. This not only improves production efficiency but also enhances product quality by ensuring that the nanometer calcium carbonate is delivered in a consistent and controlled manner. The system's ability to handle large volumes of material over long distances also makes it suitable for large - scale manufacturing operations, where material transport is a critical step in the production process.
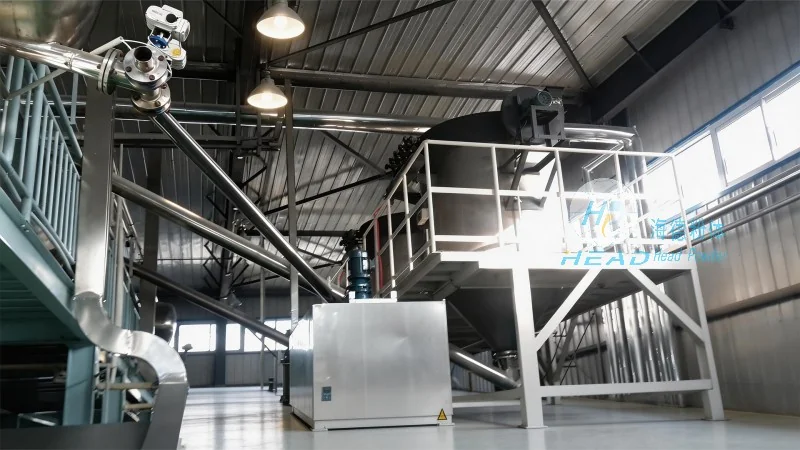
Operational Safety and Environmental Considerations
HeadPowder places a strong emphasis on operational safety and environmental compliance in the design and operation of its pneumatic conveying systems. The system incorporates multiple safety features, such as pressure relief valves and emergency shut - off mechanisms, to prevent accidents and ensure the safety of personnel. The dust collection and control unit is designed to capture and filter the fine particles of nanometer calcium carbonate, reducing the risk of airborne dust and minimizing the impact on the environment. Additionally, the system is constructed with materials that are resistant to corrosion and wear, ensuring long - term durability and low maintenance costs. HeadPowder's commitment to safety and environmental responsibility is reflected in the rigorous testing and certification of its systems, which meet or exceed industry standards.
Customization and Service Support
HeadPowder understands that each industrial application has unique requirements, and therefore, offers customized solutions for the long - distance pneumatic conveying system. The company works closely with clients to assess their specific needs, including material characteristics, distance, and production capacity, and designs a system that is tailored to meet those requirements. HeadPowder also provides comprehensive after - sales service, including installation, commissioning, and maintenance support, to ensure that the system operates at optimal performance levels. The company's team of experienced engineers and technicians is available to provide technical support and troubleshooting services, helping clients to maximize the benefits of the system and minimize downtime.




