For industries dealing with dry stone powders, efficient material handling is crucial to maintain production efficiency and product quality. A dry stone powder conveying system is a specialized solution designed to transport these powders from one location to another without the need for traditional bulk handling methods. Such systems are integral to processes in sectors like construction, mining, and chemical manufacturing, where the consistent and reliable movement of dry powders is essential for operational continuity.
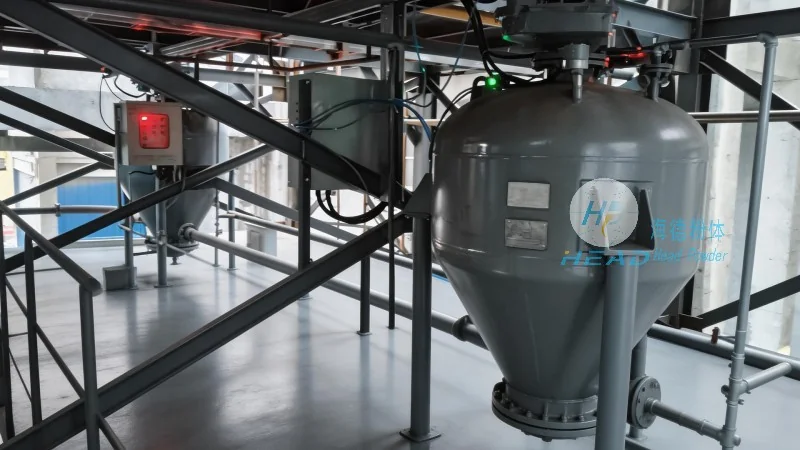
Pneumatic Conveying: The Core Technology in Dry Stone Powder Handling
At the heart of modern dry stone powder conveying systems lies pneumatic conveying technology. This method utilizes air to transport dry powders through a network of pipes, eliminating the need for mechanical components like belts or buckets that are common in traditional systems. The process involves creating a pressure differential or using vacuum to move the powder particles, which can be either dense-phase or dilute-phase, depending on the application requirements. Pneumatic conveying offers a flexible and versatile approach to handling dry stone powders, making it suitable for various distances and layouts.
Key Advantages of Pneumatic Conveying for Dry Stone Powders
One of the primary advantages of pneumatic conveying systems is their ability to handle dry stone powders without the risk of contamination or degradation. Unlike mechanical systems that may introduce friction or heat, pneumatic systems maintain the integrity of the powder, ensuring that its properties remain unchanged throughout the conveying process. This is particularly important for high-value or sensitive dry stone powders used in pharmaceuticals or specialty chemicals, where purity is paramount.
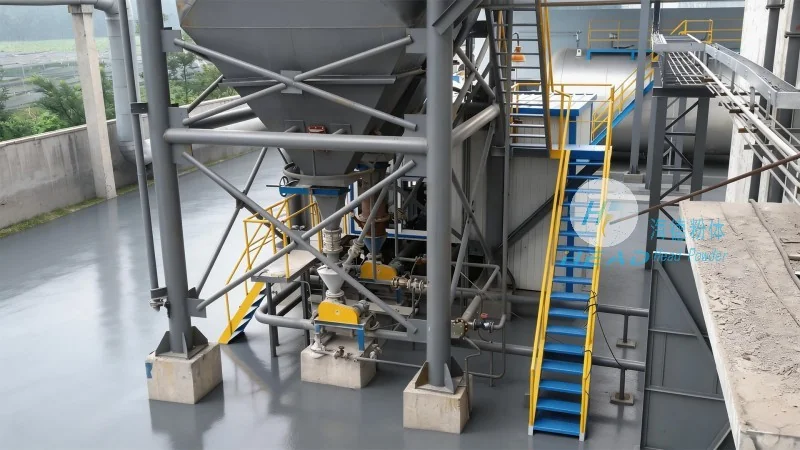
Another significant benefit is the reduced risk of dust exposure and environmental contamination. Pneumatic conveying systems are designed with enclosed pipelines and proper filtration, minimizing the release of fine powder particles into the environment. This not only improves workplace safety by reducing respiratory hazards but also aligns with environmental regulations, making it a more sustainable choice for industrial operations.
System Components and Design Considerations
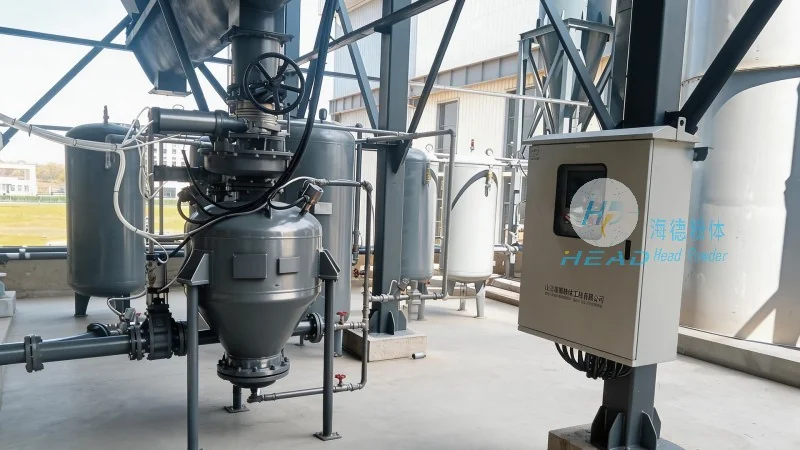
The effectiveness of a dry stone powder conveying system depends on its well-designed components. Key elements include the hopper or feeder, which feeds the powder into the system, the conveying line (pipes) that transports the material, and the receiver or discharge point where the powder is deposited. The design of these components is critical to ensure smooth operation and prevent blockages or material degradation. For example, the hopper may be equipped with a rotary valve or a screw feeder to control the flow rate, while the pipes are often made of materials like stainless steel or polyethylene to resist corrosion and abrasion from the dry stone powders.
Applications and Industry Impact
Dry stone powder conveying systems, especially those utilizing pneumatic technology, have a wide range of applications across different industries. In the construction sector, they are used to transport cement, lime, and other dry building materials to job sites, improving efficiency and reducing manual labor. In mining operations, these systems help in transporting ore powders from processing plants to storage or further processing facilities. The chemical industry also benefits from such systems when handling dry powders like pigments, fillers, or specialty chemicals, where precision and purity are critical.
By leveraging pneumatic conveying, companies can achieve higher throughput rates and lower operational costs compared to traditional methods. The flexibility of these systems allows for easy integration into existing production lines, and their ability to handle varying powder characteristics makes them adaptable to changing production needs. This adaptability is a key factor in their widespread adoption across various industrial sectors.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
As a leading provider of dry powder handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing advanced conveying systems tailored to the needs of industries dealing with dry stone powders. With a focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. HeadPowder's expertise lies in understanding the unique challenges of dry stone powder transportation and developing customized systems that address these challenges effectively.
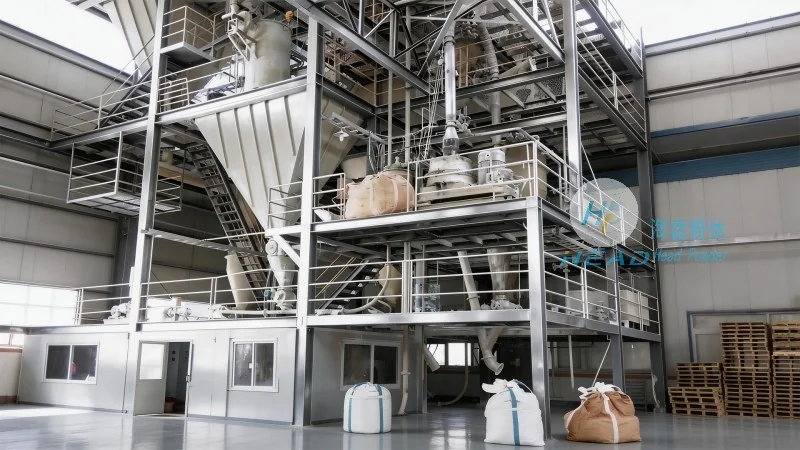
HeadPowder's systems are engineered to meet the highest standards of performance and safety. The company's commitment to using durable materials and advanced technology ensures that their conveying systems can withstand the rigors of industrial environments while maintaining optimal efficiency. Whether for small-scale operations or large-scale industrial plants, HeadPowder offers solutions that are scalable and adaptable, providing customers with a long-term investment in their material handling infrastructure.
Headquartered in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. leverages its local expertise and manufacturing capabilities to deliver high-quality products and services to clients worldwide. The company's team of experienced engineers and technicians work closely with customers to understand their specific requirements and develop tailored solutions that enhance operational efficiency and reduce costs. This customer-centric approach has contributed to HeadPowder's reputation as a leading provider in the dry powder conveying industry.




