HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced solutions for powder handling and material transport. The intelligent tonne bag feeding station is a critical component in modern industrial operations, designed to efficiently handle bulk powders from tonne bags into pneumatic conveying systems. This equipment integrates automation and precision control to ensure smooth and reliable material transfer, enhancing overall production efficiency and safety.
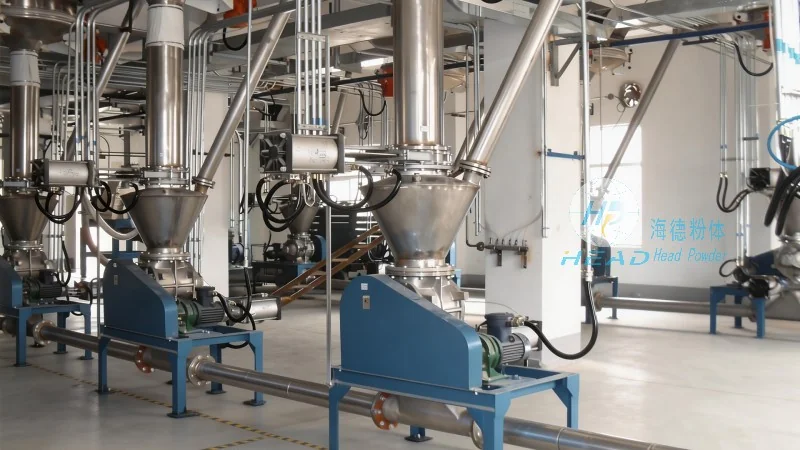
Overview of the Intelligent Tonne Bag Feeding Station
The intelligent tonne bag feeding station is engineered to streamline the process of feeding bulk powders from large tonne bags into pneumatic conveying lines. It combines mechanical, pneumatic, and control systems to achieve seamless material transfer, reducing manual intervention and minimizing the risk of material loss or contamination. The station is typically equipped with features such as automatic bag opening, material discharge, and integrated dust collection, making it suitable for various industrial applications, including chemical, pharmaceutical, food, and mining industries.
Key Components and Their Functions
The intelligent tonne bag feeding station consists of several key components, each playing a vital role in the overall operation. These components include a bag opening mechanism, a material discharge system, a pneumatic conveying unit, a dust collection system, and a control panel. The bag opening mechanism is designed to safely and efficiently open the tonne bag, allowing the material to be discharged into the conveying system. The material discharge system may include a hopper or a rotary valve to regulate the flow of powder. The pneumatic conveying unit uses compressed air to transport the powder from the discharge point to the destination point. The dust collection system ensures that airborne particles are captured and filtered, maintaining a clean and safe working environment. The control panel allows operators to monitor and control the entire process, ensuring optimal performance and safety.
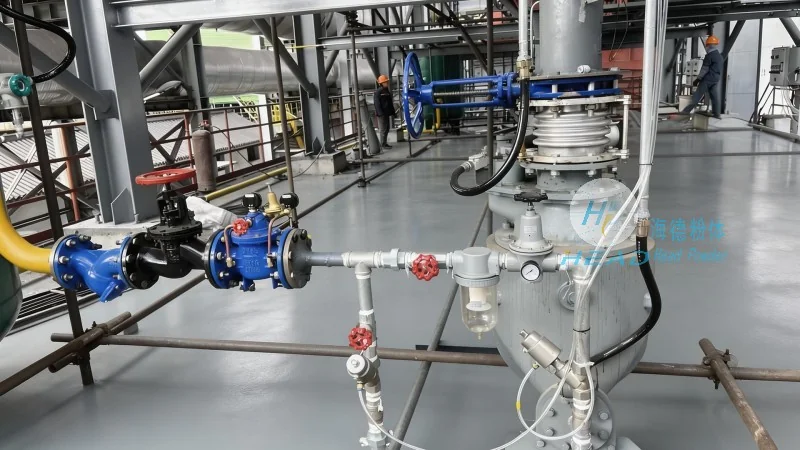
Operation Process of the Intelligent Tonne Bag Feeding Station
The operation of the intelligent tonne bag feeding station involves several sequential steps, each coordinated by the control system. The process typically begins with the placement of a tonne bag onto the station's loading platform. The control system then initiates the bag opening mechanism, which may involve cutting or tearing the bag's top to allow material discharge. Once the bag is opened, the material is discharged into the hopper or discharge system. The control panel monitors the material level in the hopper and adjusts the discharge rate as needed. The pneumatic conveying unit then activates, using compressed air to transport the powder from the discharge point to the destination point, such as a silo or a processing unit. The dust collection system operates simultaneously to capture any airborne particles, ensuring that the working environment remains clean and safe. The entire process is automated, with minimal human intervention required, and can be adjusted based on the material characteristics and production requirements.
Working Principle of the Pneumatic Conveying System
The working principle of the pneumatic conveying system used in the intelligent tonne bag feeding station is based on the movement of material particles suspended in a stream of air. The system operates by creating a pressure differential between the discharge point and the destination point, which causes the powder to be carried by the air flow. The compressed air is introduced into the conveying line at the discharge point, and the powder is drawn into the air stream, forming a slurry or a suspension. The air and powder mixture then travels through the conveying line to the destination point, where the air is separated from the powder, typically using a cyclone or a filter. The separated powder is collected in a silo or a storage container, while the air is either vented to the atmosphere or recirculated back into the system. The control system regulates the air pressure and flow rate to ensure efficient and reliable material transport, minimizing pressure losses and maximizing the conveying distance.
Advantages of the Intelligent Tonne Bag Feeding Station
The intelligent tonne bag feeding station offers several advantages over traditional manual feeding methods. First, it significantly reduces the risk of material contamination and exposure to dust, as the entire process is enclosed and automated. Second, it improves production efficiency by minimizing downtime and labor requirements, allowing for continuous operation. Third, it enhances safety by eliminating manual handling of heavy tonne bags and reducing the risk of accidents. Fourth, it provides precise control over the material flow rate, ensuring consistent quality and reducing waste. Finally, the station is designed for easy maintenance and cleaning, with components that can be easily accessed and serviced, reducing downtime and maintenance costs.
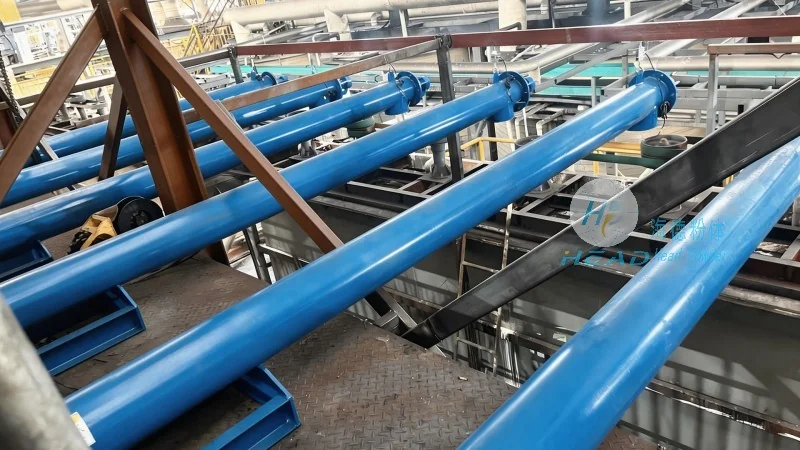
Applications and Industries
The intelligent tonne bag feeding station is widely used in various industries that handle bulk powders. In the chemical industry, it is used to feed raw materials into reactors and processing units. In the pharmaceutical industry, it is used to handle active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring that the materials are handled in a sterile and controlled environment. In the food industry, it is used to handle food powders, such as flour, sugar, and spices, ensuring that the materials are handled in a hygienic and safe manner. In the mining industry, it is used to transport ore and other minerals from the mine to processing facilities. The station's versatility and adaptability make it suitable for a wide range of applications, making it an essential component in modern industrial operations.
Conclusion
The intelligent tonne bag feeding station is a sophisticated piece of equipment that combines advanced technology and automation to efficiently handle bulk powders from tonne bags into pneumatic conveying systems. Its operation process involves sequential steps, coordinated by a control system, to ensure smooth and reliable material transfer. The working principle of the pneumatic conveying system is based on the movement of material particles suspended in a stream of air, creating a pressure differential to transport the powder. The station offers several advantages, including improved efficiency, safety, and quality control, making it an essential component in modern industrial operations. As a leading manufacturer based in Shandong, China, HeadPowder continues to innovate and provide advanced solutions for powder handling and material transport, meeting the evolving needs of various industries.




