White gray powder conveyors are critical industrial equipment for transporting bulk powders like white and gray powders. Widely used in construction, chemical processing, and food industries, these systems offer reliability and efficiency in handling fine materials. Their operation involves systematic steps, with underlying principles ensuring smooth material movement.
Key Components and Structural Design of White Gray Powder Conveyors
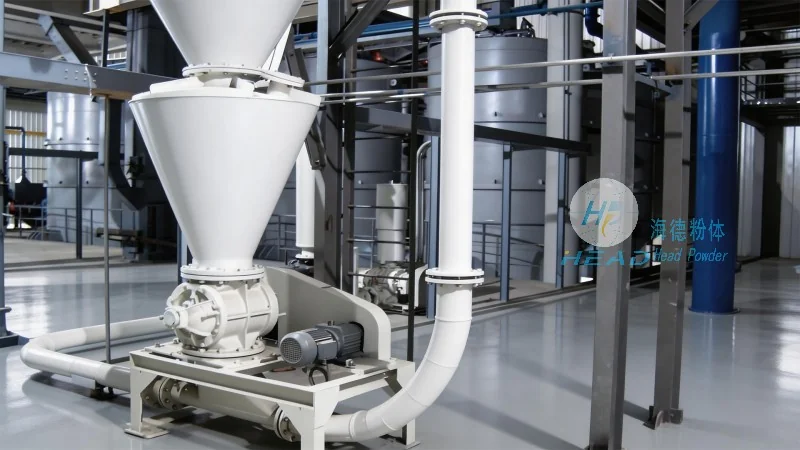
White gray powder conveyors typically consist of core components working in unison. These include a hopper for material storage, a conveyor mechanism (belt or screw), a drive system powered by electric motors, and a control panel for operation. The hopper securely holds the powder, preventing spillage and ensuring steady feed. The conveyor mechanism—whether a moving belt or rotating screw—transports the powder from the hopper to the discharge point. The drive system provides the necessary force to rotate the conveyor parts. The control panel allows operators to adjust parameters like speed, pressure, and material flow, optimizing performance.
The Operational Workflow of White Gray Powder Conveyors
The operation begins with material loading into the hopper, sourced from storage silos or batch containers. Once the hopper is filled, the conveyor system activates. The drive system powers the conveyor belt or screw, initiating movement. The powder is then transported to the discharge outlet. Conveyor speed can be adjusted to control flow rate, ensuring consistent discharge. The control panel monitors real-time parameters such as pressure, temperature, and material levels, providing feedback to operators. If blockages or overloads occur, the system can be adjusted or stopped to prevent equipment damage.
Working Principles Behind White Gray Powder Conveyors
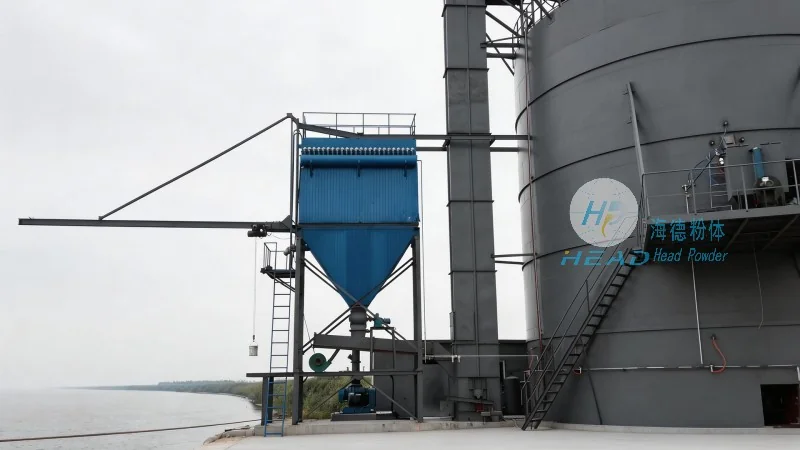
The working principles of white gray powder conveyors rely on mechanical transport and fluid dynamics. For belt conveyors, material rests on the moving belt, carried by its motion. The belt is driven by a motor rotating pulleys, with friction ensuring no slipping. Screw conveyors push material forward via a rotating screw, creating a pressure gradient that moves the powder along the length. Pneumatic systems use compressed air to propel powder through pipelines. Each type operates on these fundamentals, ensuring efficient and reliable transport.
Applications and Advantages of White Gray Powder Conveyors
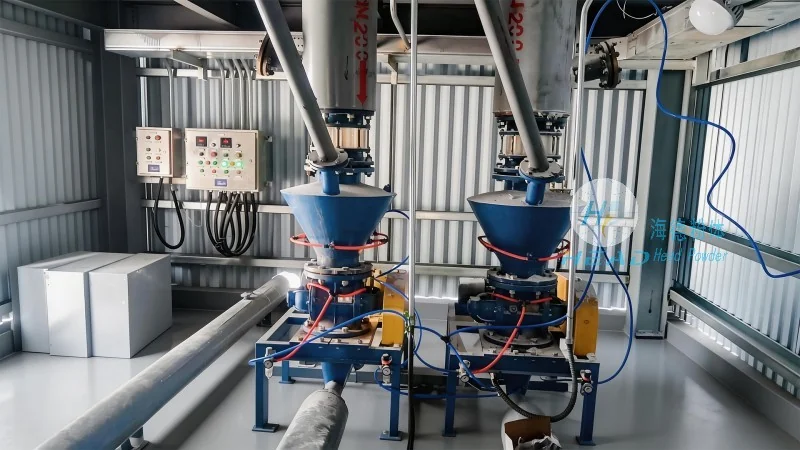
White gray powder conveyors serve diverse applications across industries. In construction, they transport cement, lime, and other powders for concrete mixing. In chemicals, they handle raw materials and finished products like pharmaceutical or fertilizer powders. In food processing, they move ingredients such as flour, sugar, and spices, maintaining hygiene. Benefits include improved efficiency, reduced labor costs, and enhanced safety. These systems handle large volumes with minimal human intervention, lowering accident risks and boosting productivity. Their design minimizes material loss and contamination, preserving powder purity.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of industrial conveyor systems, specializes in designing, manufacturing, and supplying white gray powder conveyors. With extensive industry experience, HeadPowder has built a reputation for high-quality, reliable equipment meeting diverse industry needs. HeadPowder is headquartered in Shandong, China, with a team of skilled engineers and technicians dedicated to innovative solutions for powder handling challenges. The company’s products are built for durability, efficiency, and ease of maintenance, ensuring long-term performance and customer satisfaction. Adhering to strict quality standards and advanced manufacturing techniques, HeadPowder’s commitment to quality and customer service has made it a trusted partner globally.




