HeadPowder, a leading enterprise in the field of powder handling technology, specializes in intelligent powder pneumatic conveying systems. This article delves into the fundamental principles behind these systems and explores the key operational scenarios where they are applied, providing a comprehensive overview for industry professionals and potential clients.
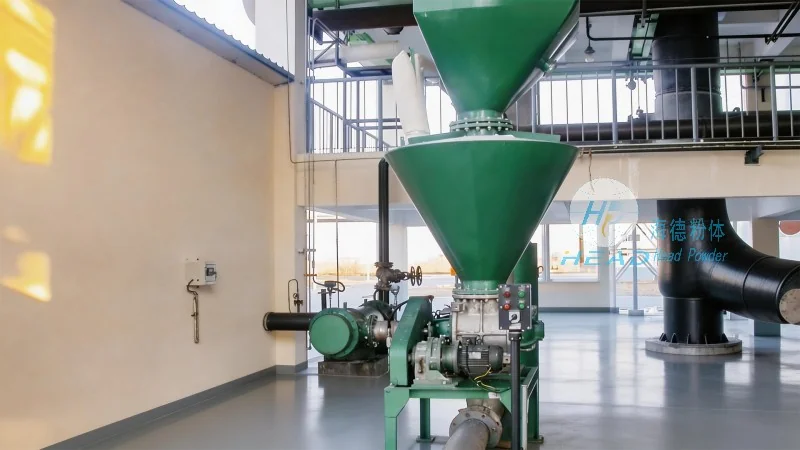
Understanding the Core Principles of Intelligent Powder Pneumatic Conveying
At the heart of intelligent powder pneumatic conveying lies the fundamental concept of using air as a medium to transport bulk powders. Unlike traditional mechanical conveying methods, which rely on physical components like belts or screws, pneumatic systems utilize pressurized or suction air to move materials through pipelines. The intelligent aspect of these systems is characterized by advanced control technologies, real-time monitoring, and automation capabilities that optimize performance, ensure safety, and enhance operational efficiency.
The basic principle involves generating a flow of air within a pipeline, which then carries the powder particles. This can be achieved through either positive pressure (where air is forced into the system) or negative pressure (where air is drawn out). The choice between these methods depends on factors such as the material properties, the distance of transport, and the required flow rate. For instance, positive pressure systems are often preferred for long-distance or high-volume applications, as they can maintain consistent pressure and prevent material degradation. Negative pressure systems, on the other hand, are suitable for applications requiring dust control or when handling materials that are sensitive to contamination.
Intelligent control systems play a pivotal role in modern pneumatic conveying. These systems integrate sensors, such as pressure transducers, flow meters, and particle counters, to monitor critical parameters in real time. By collecting data on air pressure, flow velocity, and material concentration, the system can automatically adjust the air flow rate, pressure, or conveying speed to maintain optimal conditions. This automation not only reduces the risk of equipment failure but also minimizes downtime and improves overall productivity. Additionally, advanced algorithms can predict potential issues, such as blockages or pressure drops, allowing for proactive maintenance and preventing costly disruptions.
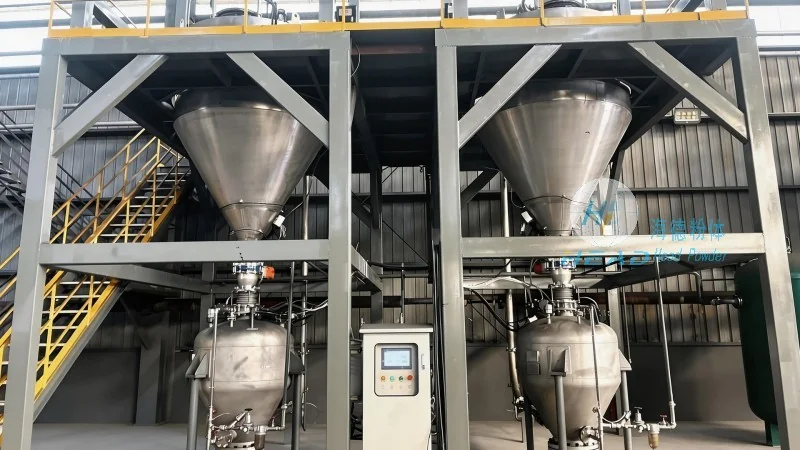
Key Operational Scenarios and Applications
Intelligent powder pneumatic conveying systems are widely adopted across various industries due to their versatility and efficiency. The following scenarios highlight the practical applications and benefits of these systems:
Chemical and Pharmaceutical Industries: In the chemical and pharmaceutical sectors, the handling of powders requires strict adherence to hygiene, safety, and quality standards. Intelligent pneumatic conveying systems are ideal for transporting raw materials, intermediates, and finished products. For example, in pharmaceutical manufacturing, these systems can be used to convey active pharmaceutical ingredients (APIs) and excipients with minimal risk of cross-contamination. The closed-loop design of the system ensures that materials remain contained, preventing exposure to environmental factors and maintaining product integrity. Moreover, the precise control over flow rates and pressure helps in achieving consistent dosing, which is crucial for batch-to-batch uniformity.
Food and Beverage Sector: The food and beverage industry demands equipment that meets stringent sanitary standards and can handle sensitive materials without compromising quality. Intelligent pneumatic conveying systems are widely used in processing facilities to transport ingredients like flour, sugar, and spices. The systems are typically constructed from stainless steel and other food-grade materials, ensuring compliance with regulations such as FDA and EU standards. The closed and dust-free environment reduces the risk of microbial contamination and maintains the freshness of the products. The ability to control the temperature and humidity within the system further enhances the preservation of perishable items, making it suitable for applications like dairy processing and bakery production.
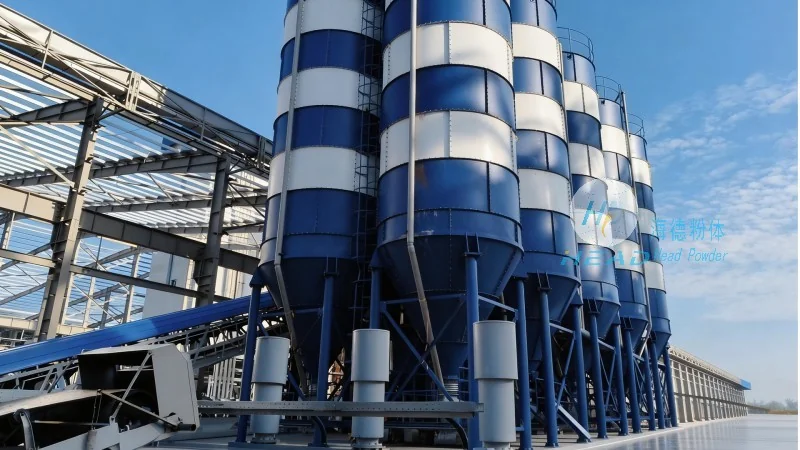
Mineral Processing and Mining: In the mining and mineral processing industry, large volumes of bulk materials, such as ores and minerals, need to be transported over long distances. Intelligent pneumatic conveying systems offer a cost-effective and efficient solution compared to traditional methods like trucks or conveyor belts. These systems can handle abrasive and heavy materials, reducing wear and tear on equipment. The automated control systems ensure consistent flow rates, which is essential for maintaining the throughput of processing plants. Additionally, the ability to integrate with other processing equipment, such as crushers and screens, allows for seamless material handling from extraction to refining.
Plastics and Rubber Manufacturing: The plastics and rubber industry involves the handling of various powders and granules, including resins, fillers, and additives. Intelligent pneumatic conveying systems are used to transport these materials from storage silos to processing machines. The systems can handle different particle sizes and densities, ensuring that the material is conveyed without segregation or degradation. The precise control over air flow and pressure helps in maintaining the quality of the final product, as variations in material flow can affect the consistency of the end product. Moreover, the closed system prevents dust emissions, which is important for maintaining a safe working environment and complying with environmental regulations.
Advantages of Intelligent Powder Pneumatic Conveying Systems
Compared to traditional conveying methods, intelligent powder pneumatic conveying systems offer several advantages that make them a preferred choice for many industries. These benefits include:
Enhanced Safety and Hygiene: The closed-loop design of the systems eliminates the risk of dust emissions and cross-contamination, making them ideal for applications where safety and product purity are paramount. This is particularly important in industries like pharmaceuticals and food processing, where even small amounts of contamination can have significant consequences.
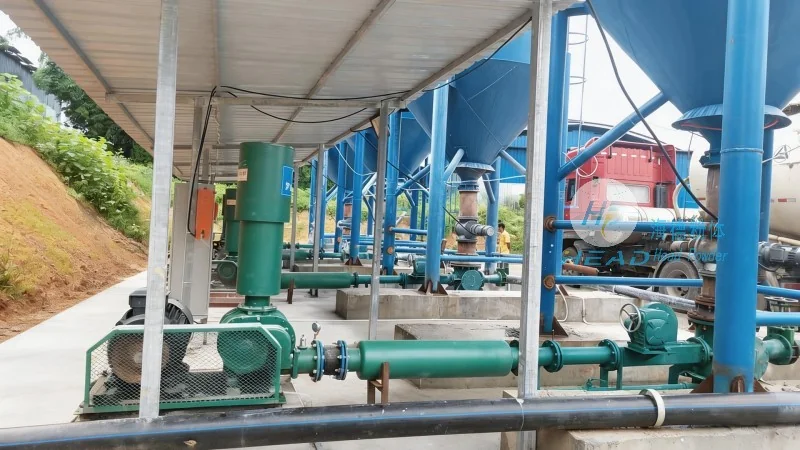
Improved Efficiency and Productivity: The automation and real-time monitoring capabilities of intelligent systems optimize performance, reducing downtime and increasing throughput. By maintaining consistent flow rates and pressure, these systems ensure that materials are conveyed efficiently, minimizing energy consumption and operational costs.
Flexibility and Versatility: Intelligent pneumatic conveying systems can handle a wide range of materials, from fine powders to coarse granules, and can be adapted to different transport distances and flow rates. The modular design allows for easy expansion or modification, making them suitable for growing businesses or changing production needs.
Reduced Maintenance and Downtime: The advanced control systems and predictive maintenance features help in identifying potential issues before they cause major failures. This proactive approach reduces the need for frequent maintenance and minimizes downtime, leading to lower operational costs and higher productivity.




