Barley, a vital grain crop, plays a crucial role in the food and beverage industry, as well as in animal feed production. Efficient material conveying of barley is essential for optimizing processing workflows, ensuring product quality, and enhancing operational efficiency in various industrial settings. This article explores the fundamental principles behind barley material conveying systems and highlights the key characteristics of their application scenarios, with a focus on the expertise and solutions provided by Shandong HeadPowder Engineering Co., Ltd., a leading company in the field.
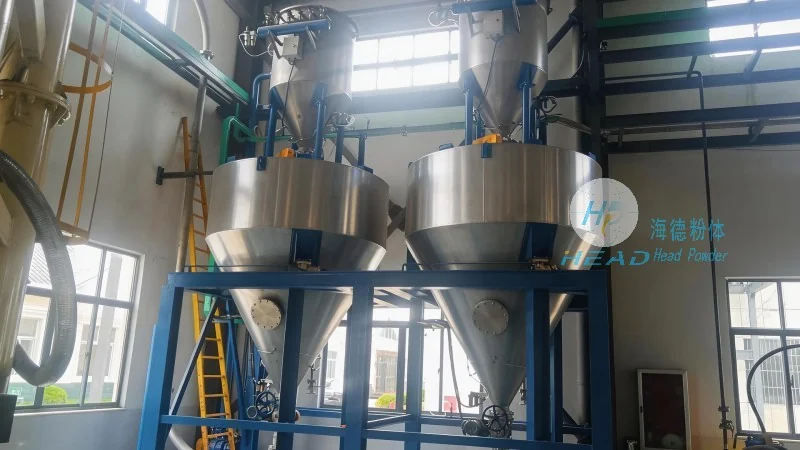
Understanding the Core Principles of Barley Material Conveying
The process of barley material conveying involves the movement of barley grains from one location to another within a processing facility. Several key principles underpin the design and operation of these systems, ensuring reliable and efficient transport. First, the physical properties of barley, such as its size, density, and moisture content, are critical factors that influence the choice of conveying method. For instance, barley grains are relatively uniform in size but can vary in moisture levels, which affects their flow characteristics. Conveying systems must account for these variations to prevent issues like blockages or uneven flow. Second, the principle of mechanical energy transfer is fundamental to most conveying systems. This involves the use of motors, belts, or other mechanical components to generate the force needed to move the barley. Common mechanical conveying methods include belt conveyors, screw conveyors, and bucket elevators, each with distinct advantages depending on the specific application requirements.
Another important principle is the consideration of gravity and incline in material handling. While mechanical systems are widely used, some applications leverage gravity to reduce energy consumption. For example, inclined chutes or gravity chutes can be employed to move barley from one level to another with minimal power input. However, this approach is often limited by the angle of the incline and the grain's characteristics, making it suitable for certain low-speed or low-volume operations. The third principle revolves around the control of material flow and the prevention of segregation. Barley grains, like many other bulk materials, can segregate during transport, leading to uneven distribution of moisture or impurities. Advanced conveying systems incorporate features such as adjustable speed controls, variable incline angles, and anti-segregation designs to maintain a consistent flow and prevent material separation.
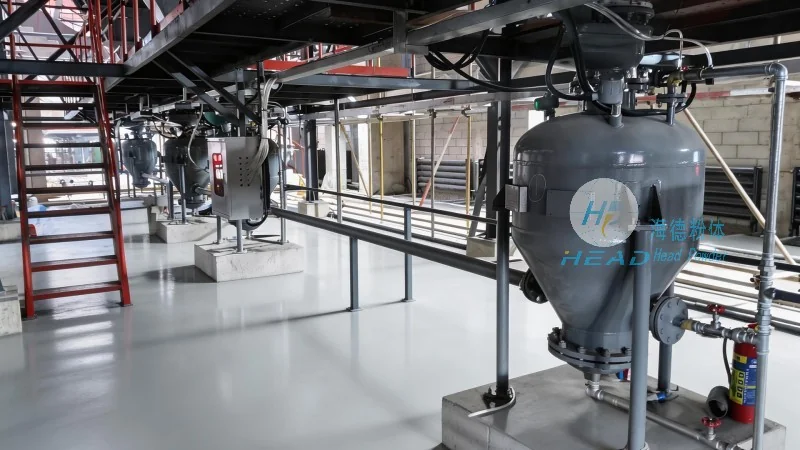
Key Working Scene Characteristics of Barley Material Conveying Systems
The application scenarios for barley material conveying systems are diverse and tailored to the specific needs of different industries. Understanding these characteristics is essential for selecting the most appropriate equipment and optimizing operational performance. One primary working scene is the grain processing plant, where barley is received, cleaned, and prepared for further processing. In this environment, conveying systems are used to transport barley from storage silos to processing lines, such as milling or malting operations. The key characteristics here include high throughput capacity, durability to withstand abrasive grain particles, and the ability to handle varying moisture levels without clogging. Shandong HeadPowder Engineering Co., Ltd. specializes in designing custom conveyor solutions for such industrial applications, ensuring that the equipment can handle large volumes of barley efficiently and maintain product integrity.
A second important working scene is the agricultural storage facility or warehouse. Here, barley is stored in bulk after harvest and needs to be moved to processing centers or distribution points. The characteristics of this scenario focus on long-term storage and the need for gentle handling to prevent grain damage. Conveying systems used in warehouses often include pneumatic conveyors or flexible hose systems that can transport barley over longer distances with minimal disruption to the grain's quality. These systems are designed to be low-maintenance and capable of operating in various environmental conditions, including temperature fluctuations and humidity variations.
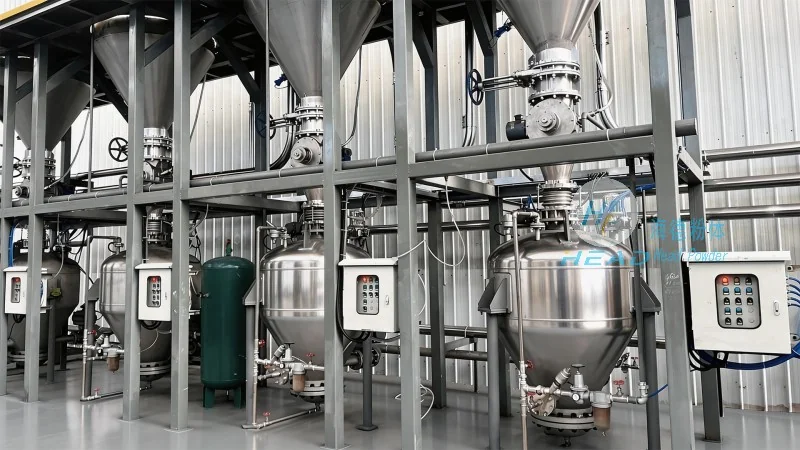
A third application scenario is in the animal feed industry, where barley is processed into feed pellets or mixed with other ingredients. The conveying systems in this context must be hygienic and capable of handling mixed materials, including grains, additives, and possibly moisture. The key characteristics include the ability to prevent cross-contamination, easy cleaning, and the integration with other processing equipment. Shandong HeadPowder Engineering Co., Ltd. offers specialized conveying solutions for feed production, incorporating features like sanitary design, adjustable speed controls, and material separation mechanisms to ensure that the final feed product meets quality and safety standards.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced material conveying systems tailored for the agricultural and food processing industries. With a strong focus on innovation and customer-centric solutions, HeadPowder has established itself as a trusted partner for companies operating in barley and other grain processing sectors. The company is headquartered in Shandong, China, and leverages decades of industry experience to develop cutting-edge conveying technologies that address the unique challenges of modern grain handling.
HeadPowder's product portfolio includes a wide range of conveyor systems, from basic belt conveyors to sophisticated pneumatic and screw conveyors. Each system is designed with the specific needs of barley material conveying in mind, ensuring optimal performance, durability, and efficiency. The company's engineering team works closely with clients to understand their operational requirements, process flow, and budget constraints, providing customized solutions that enhance productivity and reduce downtime. By integrating advanced materials and manufacturing techniques, HeadPowder's conveying systems are built to withstand the harsh conditions of grain processing, including high abrasion, moisture, and temperature variations.
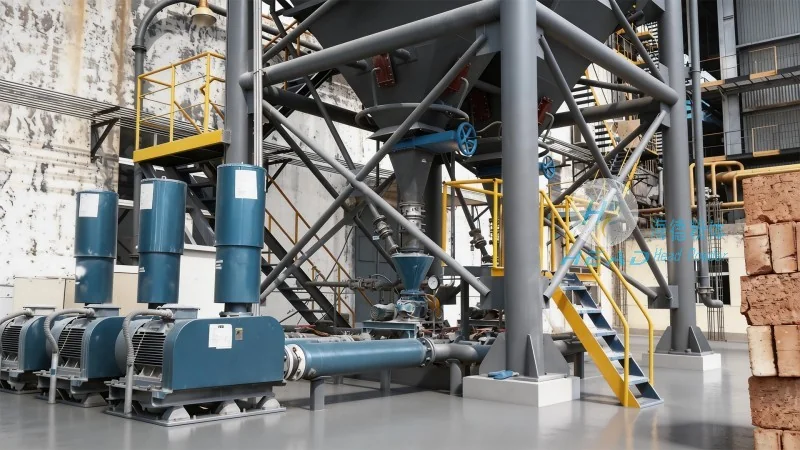
One of the key strengths of HeadPowder is its commitment to quality and customer support. The company adheres to international standards and employs rigorous testing protocols to ensure that all products meet or exceed industry expectations. Additionally, HeadPowder offers comprehensive after-sales services, including maintenance, repair, and technical support, to help clients maximize the lifespan and performance of their conveying equipment. This dedication to customer satisfaction has made HeadPowder a preferred choice for businesses seeking reliable and efficient barley material conveying solutions.
Conclusion: Optimizing Barley Handling with Advanced Conveying Solutions
In conclusion, the principles and working scene characteristics of barley material conveying are critical factors in ensuring efficient and effective grain processing. By understanding the physical properties of barley and the operational requirements of different applications, industries can select the most appropriate conveying systems to enhance productivity and product quality. Shandong HeadPowder Engineering Co., Ltd. stands at the forefront of this field, providing innovative and customized solutions that address the unique challenges of barley material handling. With a focus on durability, efficiency, and customer support, HeadPowder continues to be a key player in the agricultural and food processing industries, helping businesses optimize their operations and achieve their production goals.




